GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our high-performance engineered apparel catalog manufactured under strict ISO 9001 and OEKO-TEX standard procedures.
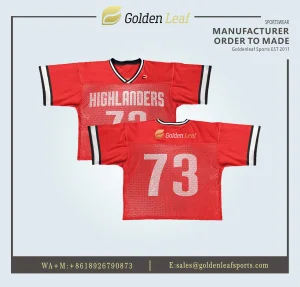
Dissecting the shift from legacy tackle-twill uniforms to light-weight, high-ventilation Revolution (Rev) mesh sublimation engineering.
Modern basketball performance demands extreme weight reduction without compromising tensile endurance. The core architecture of a high-tier Basketball Rev Jersey relies on 100% polyester open-cell micro-mesh or bird-eye interlock matrix (ranging from 145 to 180 GSM). Unlike legacy heavy double-knit fabrics, Rev jersey construction integrates micro-porous air channels that accelerate thermoregulation through convection cooling.
Rather than relying on heavy rubberized screen printing or bulky multi-layer twill patches that trap sweat against the athlete's chest, top-tier B2B suppliers utilize deep-pigment Italian sublimation inks (such as Kian or J-Teck). Under 210°C high-pressure heat transfer, the dye shifts directly from solid to gaseous state, permanently fusing into the polymer core of the fabric fibers.
Basketball movement involves continuous high-overhead vertical extensions, rapid direction switches, and intense contact. Professional Rev jerseys feature deep cut armholes, athletic V-neck or overlapping flat collar ribbing, and side-panel gussets. Seams are joined via ISO 4916 4-needle 6-thread flatlock stitching to eliminate skin friction and prevent seam blowout during physical defense.
Understanding supply chain economics, factory-direct pricing tiers, lead time predictability, and OEM/ODM operational dynamics for global distributors.
Bypass intermediary brokers. Partnering directly with integrated Shenzhen apparel facilities reduces unit costs by 35%–50%, enabling higher gross margins for athletic apparel distributors, private-label brands, and regional sporting goods stores.
With digital sublimation and laser panel cutting, pre-production virtual mockups take 24–48 hours, physical samples 5–7 working days, and bulk production of 500–5,000 units completes within 12–18 business days.
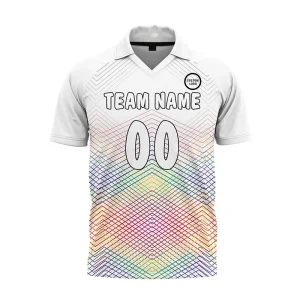
Traditional cut-and-sew mills mandate 500+ unit minimums per colorway. Our digital workflow supports low minimum order quantities starting at just 10 pieces per design, allowing custom player names and numbers without surcharge.
Full custom branding capabilities including woven neck labels, heat-transfer inner size specs, custom branded hang tags, polybag packaging, and barcoded inventory packaging for seamless Amazon or warehouse intake.
Meeting stringent global import standards, environmental safety regulations, and rigorous multi-stage physical garment testing.
All raw polyester knits, elastic bands, thread yarns, and sublimation inks are certified under OEKO-TEX Standard 100 (Class I for direct skin contact). Products fully comply with EU REACH Annex XVII regarding azo dyes, heavy metals, phthalates, and organotin compounds.
For youth basketball leagues across North America, materials strictly adhere to US CPSIA standards regarding lead content limits in textile coatings (<90 ppm) and total lead content (<100 ppm), ensuring absolute safety for junior sports programs.
Every single shipment undergoes a rigorous 5-stage inspection regime: 1) Greige fabric inspection, 2) Post-sublimation color matching against Pantone TCX/C books, 3) Cut-panel laser alignment, 4) Seam tension testing, and 5) Final dimensional measurement sanity check.
Customizing Rev jersey technical specs based on end-user athletic environments and commercial market channels.
Requires heavy-duty 180 GSM bird-eye micro-mesh, FIBA-compliant shoulder cuts, reinforced tackle-twill look via sublimated shadow layers, and custom player tall-sizing options (e.g., +2" length modifications).
Requires lightweight 150 GSM interlock fabric, fast 10-day turnaround for rapidly shifting team rosters, budget-optimized package rates for jersey + shorts + shooting shirt sets, and unisex youth grading.
Requires ultra-breathable high-ventilation open mesh, UV 50+ blocking treatments, fast-drying capillary yarns, and high-contrast dual-side reversible Rev constructions for quick home/away team changes.
Requires heavy-weight 220 GSM vintage mesh texture, custom oversized retro cut patterns, woven side seam tab labels, custom metallic foil sublimation accents, and specialized retail packaging.
How artificial intelligence, recycled polymers, and digital twin prototyping are redefining sportswear manufacturing efficiency.
Transitioning 100% of standard virgin polyester lines to eco-friendly rPET fabrics derived from ocean-bound plastic bottles. rPET delivers identical tensile strength, moisture permeability, and sublimation color vibrancy while reducing carbon footprint by 40%.
Integrating machine-learning visual alignment cameras into automated laser cutting beds. AI algorithms optimize pattern positioning to minimize fabric waste down to under 3%, while automatically adjusting for stretch tension during cutting.
Replacing physical sample shipping with 3D CAD digital twin renders with true-to-life fabric physics simulations. Research into conductive yarn integration for real-time biometric tracking (heart rate, respiration) woven seamlessly into the jersey chest panel.
Factory-direct answers to common procurement, fabric specification, and delivery queries from overseas buyers.
Discover additional high-demand custom teamwear and activewear solutions available for global wholesale order.
Connect directly with our engineering team for instant technical consultations, vector design mock-ups, physical fabric swatch kits, and competitive factory-direct volume quotes.
Request Custom Quotation & Swatch Kit