



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
High-performance technical garments and custom apparel produced under strict Industry 4.0 quality benchmarks.
An empirical analysis of global sport participation growth, regulatory evolution, and high-tech textile transitions.
Netball has evolved from a predominantly Commonwealth sport into a rapidly growing global athletic powerhouse. Managed globally by World Netball (formerly the International Netball Federation - INF), over 20 million athletes participate across 80+ nations. This expansion has created sophisticated demands for athletic apparel, moving away from heavy traditional cotton tunics toward digitally sublimated, high-tenacity synthetic textiles engineered for high-intensity indoor and outdoor play.
As elite tournaments like the Netball World Cup and the Commonwealth Games gain record viewership, commercial sponsorship has flooded into national governing bodies. Consequently, club kits, university teamwear, and professional uniforms now demand identical technical specifications: multi-directional elasticity, rapid capillary moisture evacuation, aerodynamic seam construction, and intense color fastness capable of enduring rigorous industrial laundering.
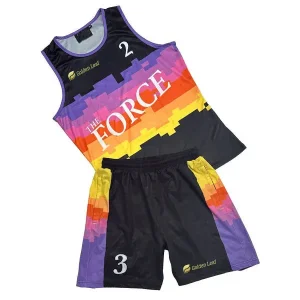
Edge-to-edge ink infusion at 220°C ensures logos, player names, positions, and sponsor branding become molecularly bonded to the fabric, completely eliminating graphic peeling or fading.
Anatomical grading designed specifically for female elite athletes. Side split hems, modified racerbacks, and stretch bodysuits offer unrestricted lateral mobility during intense match play.
Incorporating post-consumer recycled polyethylene terephthalate (rPET) micro-filaments without compromising tensile strength, enabling international brands to hit strict ESG compliance targets.
Understanding regional buying patterns, technical requirements, and wholesale procurement criteria across key international markets.
Institutional buyers, sports brand owners, and wholesale exporters operate under rigid procurement timelines. The netball season cycle varies between hemispheres: Australia and New Zealand demand bulk deliveries between November and February, whereas the UK, South Africa, and European leagues procure heavily between May and August. To manage this cyclic demand, exporters must offer robust supply chain agility, precise sizing calibration, and guaranteed color reproduction across re-orders.
| Target Region | Primary Market Segments | Dominant Apparel Styles | Technical Fabric Specifications | Key Compliance Standard |
|---|---|---|---|---|
| Australia & New Zealand (ANZ) | SSN Clubs, State Academies, School Leagues | Sublimated Netball Dresses, A-Line Skirts, Patch Bibs | 160-180 GSM Poly-Spandex (88/12), UV50+ Shielding | AS/NZS 4399 Sun Protective Capability |
| United Kingdom & Ireland | Superleague, BUCS University Teams, Local Clubs | 2-Piece Top & Skort Combinations, Thermal Midlayers | 150 GSM Honeycomb Cool-Max Mesh, Brushed Back Fleece | REACH Chemical Regulation Compliance |
| South Africa & Africa Region | Telkom Netball League, Varsity Sports, Schools | Lightweight Breathable Dresses, Reversible Training Tops | 140-160 GSM Bird-Eye Polyester Mesh, Quick-Dry Finish | SABS Textile Wash & Color Fastness Grade 4+ |
| North America & Caribbean | Collegiate Clubs, National Squads, Promotional Kits | Unisex Scrimmage Vests, Compression Tights, Hoodies | 200+ GSM Interlock Knit, High Elastane Compression | OEKO-TEX Standard 100 Safety Certification |
How advanced digital integration, automated laser cutting, and end-to-end quality assurance redefine international garment export economics.
The traditional OEM sportswear export model relied on manual cutting, uncalibrated batch dyeing, and lengthy sample iterations. Today, China's modernized apparel hubs—exemplified by Shenzhen-based facilities like GoldenLeaf Sports—leverage fully digitized Industry 4.0 infrastructure. By pairing Enterprise Resource Planning (ERP) systems with Manufacturing Execution Systems (MES), every step from yarn sourcing to custom sublimation is monitored in real-time.
High-speed optical camera lasers scan sublimated fabric rolls, automatically detecting registration marks to cut pattern panels with precise millimeter tolerances, preventing hem distortion.
In-line inspection protocols monitor seam tensile strength, stitching density (4-needle 6-thread flatlock), velcro durability on bib attachments, and weight consistency prior to packaging.
Digital printing workflows remove costly screen setups, making 10-piece custom minimum order quantities (MOQs) financially viable for grassroots teams while retaining mass-production unit pricing.
Sophisticated Raster Image Processor (RIP) color profiles ensure exact visual fidelity between digital vector proofs and physical dye transfer on synthetic polyesters, ensuring brand consistency across seasons.
Selecting optimal knits, yarn structures, and physical finishing treatments for high-intensity court dynamics.
Unlike general casual wear, netball apparel operates under extreme friction, frequent player contact, and aggressive directional shifts. Exporters must meticulously evaluate raw material parameters before initiation of cut-and-sew operations:
The gold standard for netball match dresses. Composed of 88% high-multi-filament polyester and 12% Lycra/Spandex. Delivers high recovery force, opacity (non-see-through guarantee), and 4-way mechanical stretch.
Engineered with a textured 3D pinhole pattern that optimizes capillary action. Moisture is quickly pulled from the skin to the outer garment surface for rapid evaporation, keeping athletes cool during heatwaves.
Utilized for structural outer jackets, coach polos, and training luggage accessories. Features a tight diagonal weave pattern that resists tears, wind abrasion, and rough pitch-side handling.
From elite professional leagues to youth development pathways, tailored solutions fulfill distinct athletic demands.
Elite competition demands exact body-contouring cuts, mesh side ventilation inserts, reinforced flatlock stitching to reduce chafing, and quick-detach velcro bib panels compliant with international broadcasting logo regulations.
School systems prioritize durability and multi-size versatility. Modest cut options (longer length hems, higher necklines), reinforced stress points, and unisex training pinnies ensure long-lasting multi-season service life.
Community clubs require cost-efficient, low-MOQ solutions. Standardized sizing blocks, fast 12-to-15 day production turnarounds, and easy online re-ordering portals allow club secretaries to kit out teams with minimal hassle.
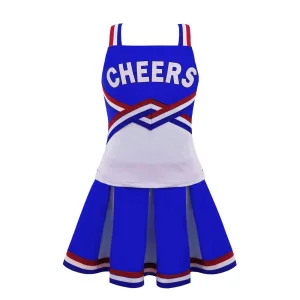
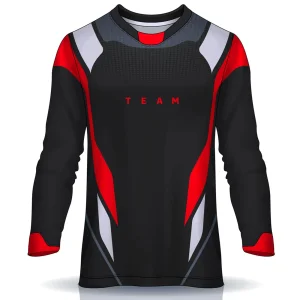
Explore our full line of sublimated sportswear, activewear, scrimmage bibs, and promotional team accessories.
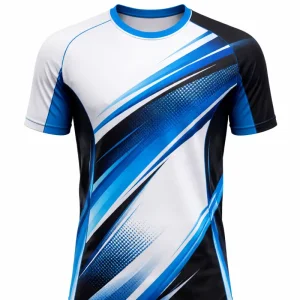
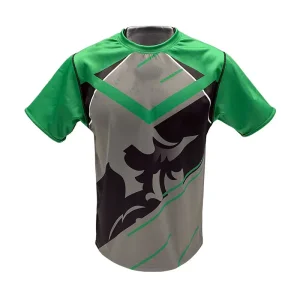
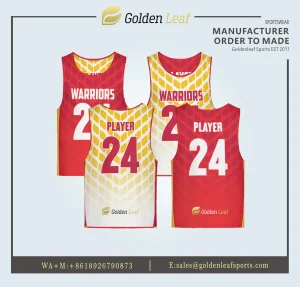
Rigorous AQL 2.5 standards and technical testing protocols ensure total confidence for overseas procurement managers.
When sourcing netball apparel from international manufacturing partners, supply chain executives must enforce strict audit parameters to avoid costly shipping delays or garment defects. GoldenLeaf Sports implements a multi-tier Quality Assurance (QA) workflow engineered specifically for sublimation and high-stretch performance apparel:
Every batch of raw poly-spandex and micro-mesh undergoes GSM verification, stretch/recovery ratio checks, and ISO 105 color fastness testing to ensure resistance to perspiration and friction.
Prior to full roll printing, a 1:1 scale paper proof is heat-pressed onto target fabric to confirm vector sharpness, sponsor logo scaling, position tag alignment, and Pantone color accuracy.
Dedicated inspectors review finished garments for thread tails, seam strength along stress points, bib velcro adhesion, size tag placement, and symmetrical panel layout.
Garments are individually packed in printed polybags, labeled with player names, numbers, and team sizes, and grouped by club rosters to streamline distribution upon arrival.
Detailed technical and commercial answers directly from our factory engineering team.
Our standard minimum order quantity is 10 pieces per design for digitally sublimated garments (including netball dresses, tops, skorts, and scrimmage vests). Because each panel is printed digitally before laser cutting, individual player names, numbers, and custom sizes can be included within the same 10-piece run at no extra charge.
Virtual digital artwork mock-ups are delivered within 24–48 hours. Pre-production physical samples require 5–7 working days. Bulk production for orders of 100 to 1,000 units is completed in 12–18 working days. Courier express air shipping (DHL/FedEx/UPS) takes 4–6 days worldwide, while sea freight takes 18–25 days depending on the destination port.
Yes. We offer both removable velcro patch bibs and printed-on bib configurations. For velcro bibs, we utilize high-durability soft-loop fasteners positioned strictly according to World Netball dimensional guidelines to ensure secure attachment during high-contact match play without snagging the dress fabric.
For warm environments, we recommend our 140–150 GSM Micro Bird-Eye Mesh or Cool-Max Interlock polyester. These technical knits feature high-density micro-pores that facilitate rapid convective air cooling and rapid capillary moisture evacuation, keeping athletes dry and lightweight.
Absolutely. Full private-label customization is standard. We provide heat-transfer inner neck branding, woven side labels, custom hangtags with barcoding, branded polybags, and custom master carton labeling to support seamless direct-to-retail or fulfillment center intake.
We archive digital vector files, master artwork layouts, and specific Pantone TCX/C code RIP profiles in our automated ERP database. Re-orders are matched against archived physical color swatches using spectrophotometer colorimeters to guarantee 99%+ visual identity across production cycles.
Accelerate your teamwear business with factory-direct pricing, Industry 4.0 production speeds, and uncompromised technical quality.
Request an Instant Factory Quote