



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered to match elite international athletic standards with full digital dye-sublimation capabilities.
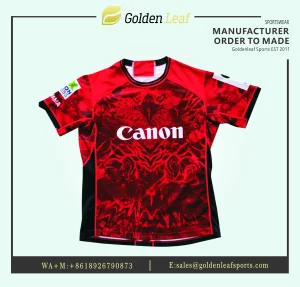
A Comprehensive Analysis of Multi-Sport Ergonomics, High-Tensile Fabric Engineering, and OEM Manufacturing Adaptation
In contemporary sports apparel procurement, the search term "Ellie Kildunne sports background manufacturers" represents far more than a query for a singular athlete’s wardrobe; it reflects a macro-level shift in modern athletic sportswear manufacturing. Ellie Kildunne—an elite English international rugby union fullback, Team GB Rugby Sevens Olympian, and cross-discipline athlete with background roots in track & field, equestrian agility, and tennis—symbolizes a new era of hybrid athletic demands. Athletes of this caliber require sportswear that seamlessly merges explosive sprinting biomechanics, violent contact durability, aerodynamic efficiency, and elevated street-style aesthetics.
For global sportswear distributors, club outfitters, and apparel brand sourcing executives, translating this multi-sport athletic profile into physical garments requires advanced apparel engineering. Chinese sportswear manufacturers have evolved beyond traditional OEM assembly to pioneer custom digital dye-sublimation, reinforced flatlock stitching, and smart zoned micro-mesh ventilation patterns specifically tuned for cross-functional performance.
SEO & Sourcing Intelligence: Modern athletic buyers demand multi-discipline garments. A rugby shirt is no longer just a boxy cotton top; it is a high-compression, 4-way stretch polyester-elastane shield engineered to withstand high-velocity tackles while optimizing skin thermoregulation during 80 minutes of intense play.
This technical evolution has compelled premier Chinese sportswear factories to integrate Industry 4.0 digital sublimation workflows. By leveraging automated digital RIP color matching, registration-mark laser cutting, and computer-guided twin-needle seam reinforcement, factories can produce customized team kits inspired by elite athletic backgrounds without incurring prohibitive tooling costs or extensive lead times.
To withstand the rigorous physical stress demonstrated in elite rugby sevens, netball, and track events, Chinese OEM factories utilize specialized synthetic yarn constructions. Below is an engineering overview of the primary fabrics utilized across high-grade athletic garment manufacturing:
| Fabric Category | Composition & Weight | Key Mechanical Properties | Primary Application |
|---|---|---|---|
| Pro-Rugby Twill | 88% Poly / 12% Elastane (260-280 GSM) | Extreme burst strength (>850 kPa), anti-grab finish, 4-way stretch | Elite Rugby Kits, AFL Uniforms |
| Cool-Max Bird-Eye | 100% Polyester Interlock (145-165 GSM) | Capillary wicking, rapid dry (<15 mins), high breathability | Soccer, Basketball, Athletics Tank Tops |
| Technical Micro-Mesh | 92% Poly / 8% Spandex (150 GSM) | Zoned thermal dissipation, soft hand-feel, anti-friction | Side panels, Youth Lacrosse, Netball Bodysuits |
| Hydrophobic Fleece | 100% Brushed Poly Fleece (280-320 GSM) | Thermal insulation, weather-resistant outer DWR treatment | Team Hoodies, Warm-up Jackets, Dailywear |
How Shenzhen manufacturing hubs combine flexible micro-batch flexibility with industrial-scale output.
By decoupling traditional screen-printing setup constraints through digital dye-sublimation, modern Chinese facilities support low Minimum Order Quantities (starting from 10 pcs/design), enabling brands to test niche teamwear markets risk-free.
Integrated optical cameras scan sublimation paper registration marks to guide high-speed laser cutters. This guarantees pixel-perfect pattern alignment across all size gradients from Youth 6Y to Adult 5XL with under 0.5mm deviation.
Rigorous QC protocols mandate stitch tension testing (AQL 2.5), color matching under standard D65 light boxes, crocking/wash fastness verification, size chart dimensional compliance, and individual bag sorting before shipment.
In compliance with EU REACH and OEKO-TEX Standard 100, top Chinese factories utilize non-toxic, water-based Italian sublimation inks alongside GRS-certified recycled polyester (rPET) derived from post-consumer plastic bottles.
Targeted apparel solutions tailored for regional sports ecosystems across North America, Europe, and Oceania.
Built for maximum impact resistance in the UK, Australia, France, and New Zealand. Custom rugby kits incorporate rubberized grip prints across the chest, reinforced collar gussets, and high-stretch elastane panels designed to resist tearing during line-outs and scrums.
Serving US and Canadian NCAA/High School athletic programs requiring complete uniform packages (Lacrosse, Basketball, Baseball, Soccer). Full customization includes individual player names, squad numbers, and institutional sponsor logos printed edge-to-edge.
Tailored pro-fit bodysuits, reversible pinnies, and athletic dresses featuring specialized female anatomical block grading. Ensures complete freedom of motion, anti-chafing flatlock seams, and zero transparency under high-intensity arena lighting.
Explore our complete manufacturing portfolio covering specialized sports, daily leisure, and outerwear.
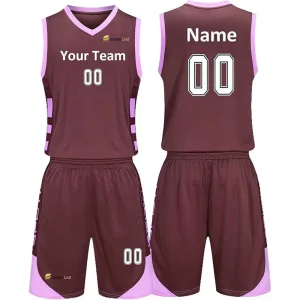
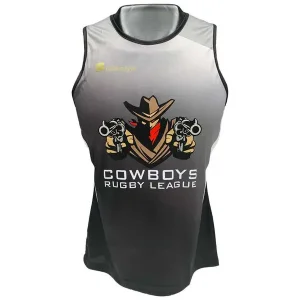
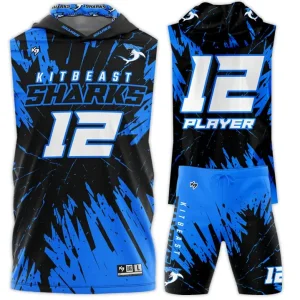
Clear, direct technical details on factory capabilities, production turnarounds, and OEM/ODM workflows.
In terms of apparel sourcing, it denotes a demand for cross-functional performance garments designed for multi-sport athletes. Garments must bridge the gap between high-velocity agility (track/sprinting), extreme physical contact resistance (rugby sevens), and high-visibility lifestyle aesthetics. Our factory translates this background into high-burst elastane twills, flatlock seam reinforcement, and vibrant digital dye-sublimation printing.
Our baseline MOQ for custom sublimated jerseys, shorts, pinnies, and netball bodysuits is 10 pieces per design run. Because each panel is digitally printed prior to automated laser cutting, player names, squad numbers, and individual size variations can be incorporated within a single 10-piece order at no additional surcharge.
2D/3D digital vector proofs are provided within 24–48 hours of Tech Pack submission. Physical pre-production samples require 5–7 working days for dye-sublimation, laser cutting, sewing, and QC sign-off. Bulk orders ranging from 300 to 1,500 units typically dispatch in 12–18 working days following signed sample approval.
We utilize computerized RIP color management software calibrated to Pantone Matching System (PMS / TCX) color standards. Using imported eco-friendly Italian sublimation inks on high-purity white base polyesters, we achieve ISO Grade 4.5 color fastness against washing, perspiration, and UV fading, guaranteeing 99% color consistency across seasonal re-orders.
Yes. Full OEM & ODM private-label solutions are available. We manufacture heat-transfer neck labels, woven brand tags, customized cardboard hangtags, individually printed biodegradable polybags, and barcode-labeled shipping cartons fully compliant with Amazon FBA or international warehouse distribution standards.