GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
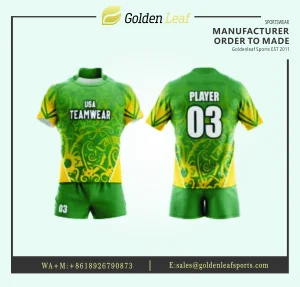
Explore our flagship OEM/ODM custom sublimated apparel products engineered for elite athletic performance, club leagues, and global private label distributors.
Analyzing technical specifications, ergonomic panel engineering, and supply chain dynamics driving the international sportswear export sector.
In the rapidly evolving global sportswear landscape, securing a highly capable China football odm manufacturer has transitioned from a pure cost-efficiency exercise into a strategic technological partnership. Modern professional football clubs, athletic brands, semi-pro academies, and sports gear distributors demand apparel that withstands high-tensile physical friction while maintaining optimal thermoregulation. The shift from standard OEM (Original Equipment Manufacturing) to full-scale ODM (Original Design Manufacturing) means that elite Chinese factories are no longer merely assembling cut panels; they are engineering proprietary micro-filament polyester structures, formulating eco-compliant sublimation dyestuffs, and utilizing generative AI CAD modeling to optimize player movement dynamics.
As search engines evaluate manufacturing entities through Google’s E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) guidelines, sourcing managers require verifiable technical data rather than generic marketing claims. A premier China-based ODM exporter integrates end-to-end capabilities: from raw yarn extrusion and warp-knitting fabric creation to high-precision RIP raster color management, laser registration cutting, flatlock ISO 607 seam construction, and automated AQL 2.5 final auditing.
Unlike basic OEM stitching, our ODM framework provides brands with complete proprietary block pattern development, ergonomic sleeve gussets, collar structural integrity, and custom ventilation zoning tailored specifically to regional body anthropometrics (US, EU, Asian sizing metrics).
By engineering multi-channel hydro-wicking cross-section fibers (such as micro-star cross-section polyester interlock ranging from 145 GSM to 180 GSM), sweat is drawn rapidly away from the dermis to the garment outer surface via micro-capillary forces for instant evaporative cooling.
Utilizing high-purity imported disperse dye inks engineered specifically for high-temperature thermo-transfer at 215°C, our custom sublimated football uniforms achieve absolute dye molecular bonding within the synthetic polymer chain, completely eliminating bleeding or washing fade.
Unpacking how Shenzhen and the Pearl River Delta apparel industrial matrix delivers unmatched speed, material redundancy, and cost efficiency.
Operating from Shenzhen—the global epicenter of high-tech manufacturing and hardware innovation—allows modern football apparel factories to fuse electronic digital printing precision with textile craftsmanship. Within a 50-kilometer radius of our production hub, we access specialized knitting mills, custom elastic webbing suppliers, recycled PET yarn converters, and eco-certified dye houses.
This dense industrial clustering provides unprecedented supply chain resilience. When global logistics experience localized bottlenecks or raw yarn prices fluctuate, our integrated network ensures continuous material replenishment. Furthermore, direct access to premier export terminals such as Yantian and Shekou ports streamlines global container shipping and air freight forwarding to overseas destinations across North America, Europe, Oceania, and the Middle East.
Many overseas trading intermediaries subcontract separate stages of football jersey production—outsourcing graphic design to one studio, printing to an external dye house, and stitching to a third-party workshop. This fragmented model frequently results in color batch variation, misaligned dynamic side stripes, delayed production schedules, and zero quality accountability.
Our established 3,000 m² facility eliminates third-party risks by executing every operational node under one centralized management system:
| Manufacturing Parameter | Standard OEM Sourcing | GoldenLeaf China Football ODM Standard | Performance Benefit |
|---|---|---|---|
| Fabric Construction | 100% Basic Circular Polyester Mesh | Micro-Star Interlock & 4-Way Poly-Spandex (88/12) | Superior tensile recovery & non-chafing skin comfort |
| Printing Technology | Traditional Screen Print / Basic Sublimation | 1200 DPI High-Density Italian Eco-Sublimation Ink | Breathable zero-handfeel print, unyielding vivid colors |
| Seam Engineering | Standard 3-Thread Overlock Seam | ISO 607 4-Needle 6-Thread Flatlock Reinforcement | Eliminates skin irritation and resists tackle tearing |
| Pattern Customization | Rigid Stock Templates Only | Fully Tailored CAD Blocks & Dynamic Mesh Venting | Ergonomic athletic fit for elite competition standards |
| Minimum Order Quantity (MOQ) | 500 - 1,000 Pcs per style | Flexible 10 Pcs micro-run per custom design | Ideal for squad customization, individual names & numbers |
A granular technical walk-through of how raw technical fibers are transformed into FIFA-compliant team uniforms.
Our athletic design team ingests brand tech packs or vector graphics (AI, EPS, PDF), converting artwork into precise pattern templates tailored for modern athletic cuts. Body mapping technology places high-breathability bird-eye mesh panels strategically under armpits and across lower back zones where heat build-up is highest.
To eliminate discrepancies between digital screen RGB preview and physical textile CMYK print, we utilize advanced Raster Image Processor (RIP) software mapped directly to the Pantone Matching System (PMS). Fluorescent and high-chroma team accents are calibrated using custom color profile curves.
Using state-of-the-art Japanese wide-format digital printers equipped with high-density piezo printheads, eco-certified water-based sublimation inks are printed onto specialized 57 GSM heat-transfer paper, guaranteeing crystal-clear vector line resolution down to 0.1mm detail.
The printed transfer paper and high-filament white polyester fabric pass simultaneously through rotary continuous oil-heated transfer calenders. At 215 degrees Celsius and under 4.5 bar pneumatic pressure, the solid ink sublimates directly into a gaseous state, instantly penetrating and locking within the synthetic polyester polymer chains. The result is a total zero-handfeel graphic that never peels, cracks, or restricts fabric breathability.
Instead of manual shears or die-cutting that cause dimensional distortion, our facility employs automated vision camera laser cutting machines. The optical sensors register printed target marks on the sublimated rolls, cutting panels with 0.2mm edge precision while heat-sealing synthetic edges to prevent fraying during subsequent assembly.
Assembly technicians construct garments using specialized sewing machinery. Shoulder and armhole seams receive reinforced double-line overlocking, while side panels incorporate flatlock ISO 607 stitching to eliminate inner seam abrasion against athletic skin during intense match play.
ODM orders receive full branding packages: heat-applied satin neck labels, woven side seam tabs, high-definition 3D silicone crest emblems, custom swing tags, and barcoded retail polybags customized for international retail clearance.
Every completed football uniform unit undergoes rigorous inspection by our internal QA team. Garments are audited for dimensional accuracy against approved size charts, color fastness, seam tension integrity, and accurate player number/name matching before automated sorting into master shipping cartons.
Discover how our custom football apparel design platform powers diverse athletic tiers, retail brands, and regional sporting environments worldwide.
We supply full matchday home, away, and third kits alongside training gear (bibs, tracksuits, compression base layers) for top-tier professional clubs and youth academies across Europe, South America, and North America. Every kit offers personal player name and number customization inside micro-MOQ production runs.
For emerging or established sports apparel labels seeking complete ODM turnkey support, we act as an invisible, highly responsive manufacturing backbone. From initial sketch rendering to custom woven neck labels, hang tags, and branded packaging, we deliver shelf-ready retail product lines.
High schools, university intramural leagues, and international tournament organizers benefit from our rapid 12 to 18-day turnaround times. Reversible pinnies and sublimated shorts allow multi-team event organizers to cut apparel logistics costs while maintaining uniform visual standards.
Engineered for teams competing in warm, humid regions (e.g., Southeast Asia, Australia, Gulf Region, Latin America), our micro-mesh polyester options integrate UPF 50+ UV filtering and anti-bacterial silver ion treatments to minimize body odor and prevent fabric cling.
Combining street fashion aesthetics with performance athletic fabrics, our factory creates high-impact sublimated gaming jerseys, athletic joggers, and oversized hoodies with complex vibrant graphics and gradient artwork engineered specifically for live broadcasts and arena sponsorships.
Companies hosting internal football tournaments or sponsoring regional charity matches leverage our rapid 24 to 48-hour digital mock-up workflow. Low minimum orders allow corporate clients to brand custom kits with exact corporate brand colors and sponsor placement.
Ensuring every custom sports garment meets rigorous global safety, environmental, and physical performance benchmarks.
Global consumers and sporting federations demand apparel free from toxic substances, azo dyes, heavy metals, and phthalates. All base polyester textiles, elastic bands, zip closures, and sublimation inks utilized in our Shenzhen manufacturing plant comply strictly with OEKO-TEX Standard 100 (Class I for Infant and Skin Contact) and EU REACH regulations.
Our water-based sublimation inks emit zero volatile organic compounds (VOCs) during high-temperature thermal transfer, making our factory environmentally sustainable while ensuring finished football uniforms are 100% hypoallergenic for long-duration skin contact.
To earn our status as a premier China football odm manufacturer, every new fabric batch undergoes mandatory laboratory stress testing before entering the sewing line:
Clear, direct technical answers curated by our lead garment engineers and export supply chain directors.
Browse our extended production lines encompassing rugby kits, fitness wear, basketball apparel, and custom sports flags.