



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct from GoldenLeaf Sports Shenzhen 3,000 m² Industry 4.0 Sublimation & Manufacturing Hub
Analyzing the shift from traditional Test territories to a 2.5 billion hyper-engaged international fanbase driving athletic apparel demand.
Cricket is experiencing an unprecedented structural transformation. Historically concentrated within Commonwealth nations such as India, England, Australia, Pakistan, and South Africa, the sport has breached legacy boundaries. Driven by the explosive growth of Twenty20 (T20) domestic leagues—such as the Indian Premier League (IPL), Big Bash League (BBL), Caribbean Premier League (CPL), and Major League Cricket (MLC) in the United States—the global cricket fanbase has expanded to over 2.5 billion individuals, establishing cricket as the second most popular sport on the planet.
This geographic expansion has shifted sportswear procurement dynamics. Fan loyalty is no longer restricted to national team merchandise; it has decentralized into regional franchise kit demands, grassroots amateur club proliferation, and high-frequency seasonal jersey updates. Furthermore, the inclusion of T20 cricket in the 2028 Los Angeles Olympic Games has mobilized government and private investment in sports infrastructure across North America, Europe, and East Asia, creating massive demand for customized, performance-grade teamwear.
Cricket is unique in its physical demands on athletic textiles. Matches range from multi-day test formats requiring maximum thermal comfort under intense sunlight to high-intensity T20 formats demanding hyper-breathable, 4-way stretch polymers. Modern global brand buyers, sporting goods distributors, and teamwear brands require sportswear engineered for extreme environmental stress:
What International Sportswear Brands, Distributors, and League Buyers Demand from Chinese Manufacturers
Global distributors no longer maintain large warehouse inventory. Modern contracts require low minimum order quantities (MOQ 10 pcs per design) where each individual garment features unique player names, numbers, and sponsor placements printed directly into the fabric without extra setup fees.
Sponsors demand exact vector color reproduction across all batch orders. Utilizing advanced RIP software (Ergosoft/Wasatch) and Eco-friendly imported inks, manufacturers must guarantee Grade 4+ color fastness (ISO 105-C06) with zero shade variance over multi-season reorders.
Overseas clients require streamlined cross-border operations. Manufacturers must seamlessly deliver under EXW, FOB Shenzhen, CIF, and DDP (Delivered Duty Paid) terms via air, sea, and courier networks with complete customs and tax clearance.
How Shenzhen's Advanced Apparel Manufacturing Ecosystem Outperforms Global Alternatives in Quality, Cost, and Lead Times.
The global sportswear industry has undergone severe supply chain disruptions in recent years. While south-Asian apparel hubs often struggle with fragmented raw material access, power grid volatility, and fluctuating dye quality, China’s Greater Bay Area (specifically Shenzhen) offers an unmatched, vertically integrated manufacturing infrastructure.
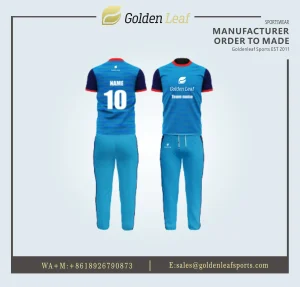
GoldenLeaf Sports operates within this cluster, housing pattern engineering, digital sublimation transfer, high-precision registration laser cutting, sewing lines, and a 5-inspector QA/QC protocol inside a single 3,000 m² campus. This spatial integration eliminates internal logistics latency, allowing raw white polyester yarn to transform into fully customized, branded cricket uniform sets within days.
Unlike screen printing or vinyl transfers which sit on top of the fabric and block ventilation, digital sublimation locks eco-solvent inks directly into the polyester micro-fibers under 200°C heat and extreme pressure. The resulting graphic becomes part of the molecular structure of the jersey—guaranteeing 100% breathability, zero peeling, and zero cracking despite intense wash cycles.
Traditional manual shearing causes alignment errors across complex side-panel graphics and collar seams. GoldenLeaf Sports utilizes optical-camera guided laser cutting tables that detect printed registration marks on the fabric. Panels are sliced with sub-millimeter precision, sealing edge fibers to prevent fraying and ensuring perfect seam alignment during assembly.
Tailoring Textile Engineering and Block Patterns for Key Geographic Markets
Primary Driver: Rapid expansion of Major League Cricket (MLC), university clubs, and corporate weekend leagues.
Apparel Spec: Relaxed American athletic sizing, heavyweight poly-spandex blends, mesh side venting, and multi-sponsor sublimation graphics.
Primary Driver: Traditional County club cricket, school academies, and indoor winter T20 leagues.
Apparel Spec: Tailored European block cuts, classic cream/white traditional weaves alongside vibrant T20 sublimated kit designs, 160 gsm bird-eye mesh fabric.
Primary Driver: High-sun exposure environment, professional club systems, and regional grassroots sports.
Apparel Spec: Maximum UV 50+ blocking protection, hyper-wicking mesh, reinforced collar stays, and high-frequency stretch side panelling.
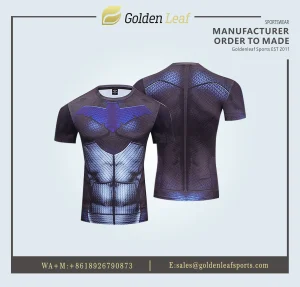
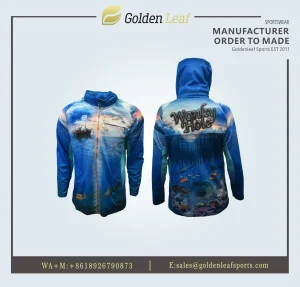
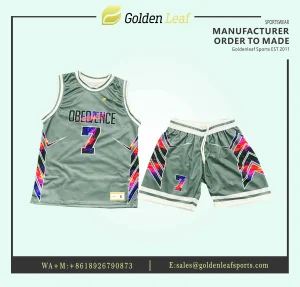
Factory-Direct ODM & Private Label Manufacturing Services
Essential Technical & Commercial Information for Brands, Distributors, and Sports Organizations
Whether you are scaling a regional cricket brand, managing league contracts, or launching an international athletic wear line—our 160-person technical manufacturing team is ready to deliver precision apparel under guaranteed lead times.