GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our engineered team kits, customized jerseys, and technical outerwear tailored for global distributors and sports organizations.
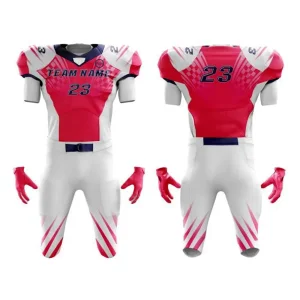
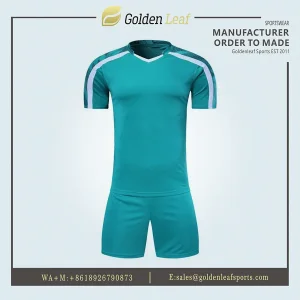
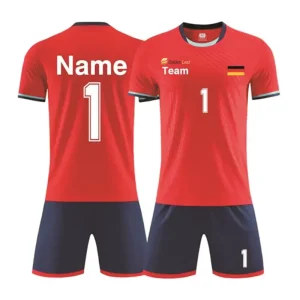
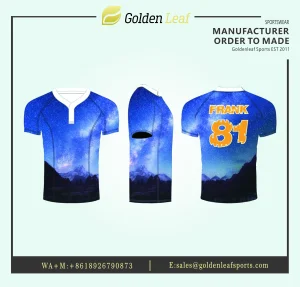
From basic Cut-Make-Trim (CMT) workshops to automated digital sublimation ecosystems—how China's sportswear exporters are reshaping global athletic procurement.
In the contemporary global athletic apparel market, the phrase "China good soccer kits Exporters & Exporter" represents far more than a simple sourcing search query. It signifies a profound paradigm shift in international sportswear manufacturing, supply chain engineering, and digital fabric customization. Over the past decade, China’s athletic textile hub—centered predominantly in the high-tech manufacturing corridors of Guangdong Province, specifically Shenzhen—has transformed from low-margin, high-volume CMT facilities into sophisticated Original Equipment Manufacturer (OEM) and Original Design Manufacturer (ODM) powerhouses.
This technical white paper explores the underlying mechanics that enable leading Chinese sportswear exporters, such as GoldenLeaf Sports (ShenZhen) Co., Ltd., to command high global market share while maintaining strict quality standards, competitive pricing, and rapid operational agility. By integrating advanced 3D digital garment modeling, automated RIP colour management, environmentally compliant dye sublimation inks, and lean flexible sewing lines, modern soccer kit exporters can fulfill complex global contracts ranging from elite professional clubs to grassroots youth leagues with unprecedented turnaround speeds.
Detailed analysis of synthetic yarn structures, GSM selection, capillary moisture-wicking technology, and digital dye transfer physics.
Utilizing 100% micro-polyester filaments engineered between 145 GSM and 180 GSM. Micro-mesh and bird-eye knits maximize surface area to optimize cross-flow ventilation while preserving structural tear resistance during intense match play.
Engineered yarn cross-sections (such as cross-shaped or trilobal fibers) draw sweat instantly away from the athlete's dermis via capillary pressure, transferring moisture to the fabric's outer boundary for sub-minute flash evaporation.
Utilizing non-toxic, OEKO-TEX certified disperse dyes. Injected directly into the molecular structure of heated polyester fibers at 200°C–220°C, creating high-definition colors that never crack, peel, or fade under heavy washing.
| Performance Parameter | Full Digital Dye Sublimation | Traditional Screen Printing | Cut-and-Sew Vinyl Transfer |
|---|---|---|---|
| Breathability & Airflow | 100% Unobstructed (Ink bonds chemically) | Restricted (Heavy rubberized ink barrier) | Severely Blocked (Plasticized film patch) |
| Color & Design Complexity | Unlimited gradients, logos, player names | Limited to 4–6 solid spot colors | Basic vector cuts, multi-layer weight |
| Durability & Fastness | Grade 4-5 (Fibers permanently dyed) | Prone to cracking after 25+ washes | Edge peeling after high-temp drying |
| Variable Data Customization | Zero extra charge per player name/number | High film setup cost per custom garment | High labor cost per individual heat press |
| Environmental Footprint | Zero water waste process, eco-friendly inks | Chemical screen washing & liquid runoff | Polymer waste backing sheets generated |
Understanding the strategic, operational, and technological density of the Pearl River Delta apparel manufacturing hub.
Shenzhen, positioned at the heart of Guangdong's textile innovation ecosystem, offers unparalleled proximity to functional raw material mills, specialized yarn dyers, custom trim manufacturers, and international freight ports (Yantian/Shekou). What takes weeks in other manufacturing regions—such as sourcing 4-way stretch poly-spandex mesh or custom Jacquard ribbed collar trims—is accomplished within 24 to 48 hours locally.
This localized density dramatically compresses the time-to-market cycle for international soccer exporters, allowing bulk pre-production samples to be executed within 5–7 working days and full production orders delivered within 12–18 days.
Modern sports uniform production requires immaculate seam strength and dimensional stability. Top Chinese exporters employ senior apparel technicians—making up over 80% of GoldenLeaf Sports' 160-person workforce—who excel in operating 4-needle 6-thread flatlock machines, automated laser registration cutters, and digital pattern-grading CAD suites.
Supported by a dedicated 5-person QA/QC inspection team checking point-to-point measurement tolerances, stitch density, and Pantone color accuracy prior to packaging, buyers receive error-free goods ready for immediate retail or team distribution.
Navigating the shift toward low-MOQ on-demand manufacturing, eco-friendly recycled polymers, and integrated OEM/ODM partnership models.
Legacy apparel manufacturing demanded thousands of units per style, tying up inventory capital. Modern soccer kit exporters break this barrier by offering low minimums (starting at just 10 pcs/design), enabling sports brands to test new aesthetic concepts without over-committing capital.
Environmental, Social, and Governance (ESG) compliance is now essential. Leading Chinese manufacturers incorporate recycled post-consumer PET bottle yarns into high-performance jerseys, providing certified sustainable options for global brands targeting eco-conscious consumers.
Top exporters streamline international trade by offering comprehensive logistics support, including EXW, FOB Yantian, CIF, and Delivered Duty Paid (DDP) air/sea freight solutions—handling tariff clearance and door-to-door transit seamlessly.
How specialized sublimated soccer kits and teamwear address distinct operational demands across diverse international markets.
High-intensity competitive leagues demand lightweight (145-150 GSM) micro-mesh kits with athletic trim cuts, reinforced stress points, flatlock friction-free stitching, and vibrant high-contrast sponsor graphics that remain sharp under stadium lights and high-definition broadcasts.
Educational institutions across North America, Europe, and Australia require multi-year style consistency for team roster additions. Pattern-grading systems ensure identical color matching and precise fitting across youth sizes (6Y) to adult extended cuts (5XL).
Independent activewear brands leverage complete OEM/ODM solutions—including custom heat-seal neck labels, woven side tabs, custom hangtags, branded polybags, and bespoke silicone chest crests—to launch professional collections with reduced overhead.
Large-scale amateur tournaments, charity cups, and corporate wellness initiatives require rapid-turnaround bulk soccer kits that combine cost efficiency, high breathability, and vibrant multi-sponsor visual space.
Clear, factory-direct answers covering production mechanics, MOQ terms, fabric engineering, and global logistics.
A reputable soccer kit exporter combines vertical technical integration with transparent quality governance. Key benchmarks include in-house digital dye sublimation capabilities (preventing third-party delays), strict fabric testing for pilling and color fastness (ISO 105 standard Grade 4+), low flexible minimum order quantities, clear pattern grading for regional fits (US, EU, AU sizing), and dedicated multi-stage QC inspections prior to dispatch.
Our baseline MOQ for custom sublimated soccer uniforms, jerseys, and shorts is 10 pieces per design. Because panels are printed digitally before being cut and assembled, individual player names, numbers, and sizes can vary across the 10-piece batch at no additional custom fee.
Digital 2D vector mock-ups are completed within 24 to 48 hours. Pre-production physical samples take 5 to 7 working days. Once approved, bulk manufacturing of 300 to 1,000 units is typically completed in 12 to 18 working days inside our 3,000 m² Shenzhen factory.
We recommend 145 GSM to 160 GSM 100% micro-polyester bird-eye mesh or waffle-knit interlock. These engineered knits offer optimal weight-to-breathability ratios, utilizing hydrophilic capillary channels to instantly dissipate moisture during match play.
Yes. We offer complete ODM and private-label packaging: heat-transfer or woven neck labels, custom paper hangtags, individual branded polybags, barcodes, size stickers, and master carton marking configured to your exact commercial requirements.
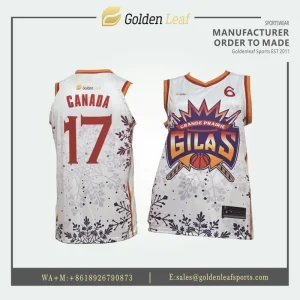
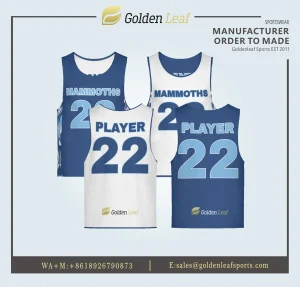
Discover our specialized range of rugby, basketball, cheerleader, lacrosse, and multi-sport custom apparel engineered for high endurance.