GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct from China's leading digital sublimation and technical apparel manufacturing infrastructure.
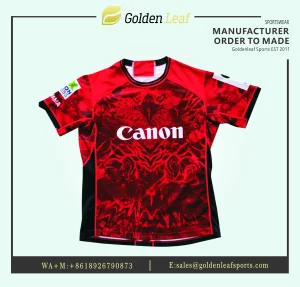
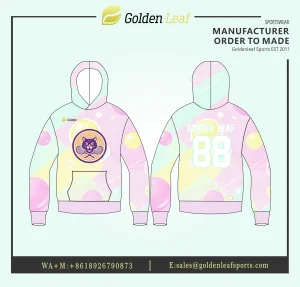
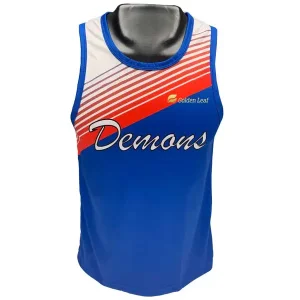
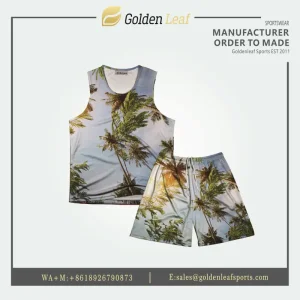
Bridging international sporting standards from Jersey's iconic grounds to China's apex manufacturing ecosystems.
The global sports apparel market is undergoing a seismic transformation. Modern professional sporting bodies, international tournament organizers, and regional leagues are no longer satisfied with generic off-the-shelf uniforms. Nowhere is this demand for technical perfection more evident than in international cricket environments—exemplified by historic venues such as the Grainville Cricket Ground in St. Saviour, Jersey, home to the Jersey Cricket Board and a recurring venue for International Cricket Council (ICC) World Cricket League tournaments.
Matches played at venues like Grainville subject athletic apparel to rigorous microclimatic conditions: coastal humidity, intense solar UV exposure, high physical friction during fielding slides, and prolonged multi-day endurance requirements. Consequently, national sports organizations, governing bodies, and global apparel brands seek manufacturing partners capable of combining advanced material science with extreme supply chain agility.
Key Strategic Insight: The intersection of specialized venue requirements (such as Grainville's turf and weather conditions) and advanced OEM manufacturing in Shenzhen, China has established a new benchmark for global teamwear procurement. Chinese manufacturers now supply over 65% of custom sublimated team kits across ICC Associate nations and elite sporting clubs worldwide.
Chinese sportswear enterprises have pivoted from low-cost volume cutting to high-precision, technology-driven activewear manufacturing. Utilizing state-of-the-art Italian fluorescent inks, automated laser-cutting tables, registration mark recognition systems, and specialized poly-spandex knits, Chinese factories lead the world in delivering tournament-ready match uniforms, training bibs, technical outerwear, and club merchandise.
How continuous R&D and supply chain integration deliver unmatched competitive edges for international buyers.
Utilizing high-definition RIP color management software coupled with Epson and Mimaki industrial print heads, ensuring exact Pantone color matching for club heraldry and corporate sponsor logos without color bleeding or cracking.
Custom-milled 145 GSM to 280 GSM polyester interlock, bird-eye mesh, and 4-way stretch poly-spandex blends engineered with moisture-wicking capillary channels that pull sweat away from the athlete's skin to expedite evaporation.
Heavy-duty, anti-chafing twin-needle and 4-needle 6-thread flatlock stitching technology designed to withstand high-tensile torque during bowling actions, tackling in rugby, or sliding across natural grass outfield surfaces.
The manufacturing cluster located in the Longgang and Bao'an districts of Shenzhen represents the world's most concentrated textile technology corridor. Unlike traditional manufacturing hubs that rely on fragmented subcontracting, modern tier-1 Chinese manufacturers integrate design, digital paper printing, heat-transfer sublimation, laser pattern cutting, garment assembly, and multi-stage Quality Assurance under a single roof.
This vertical integration yields unprecedented efficiency metrics:
From elite matchday whites to multi-sport community apparel across key global target markets.
Custom whites, cream test kits, and vibrant T20/One-Day colored kit combinations designed to strict ICC guidelines, featuring reinforced collar plackets, mesh underarm breathability panels, and padded trousers.
Scalable production lines for schools, university sports departments, and multi-discipline clubs spanning cricket, rugby, soccer, basketball, ultimate frisbee, and track & field equipment.
Complete white-label execution including custom woven neck tags, heat-seal silicone labels, printed polybags, custom hangtags, and barcoded inventory packaging ready for global retail distribution.
Analysis of procurement data across Europe, North America, Australasia, and the Middle East reveals three defining shifts in international buyer intent:
Direct technical guidance for team managers, brand owners, and procurement directors.
China's sportswear manufacturers offer unmatched technological precision, scalable sublimation capabilities, and extensive pattern libraries tailored to ICC and international sporting standards. With rapid production turnarounds, specialized UV-protective micro-mesh fabrics, and full OEM/ODM branding capabilities, Chinese facilities provide high-end custom apparel at factory-direct pricing, ideal for both professional national setups and regional clubs.
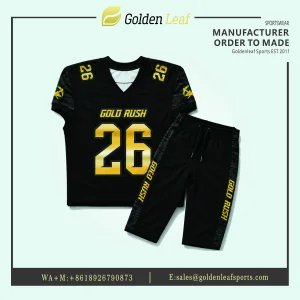
Our standard production MOQ starts at just 10 pieces per design for custom sublimated jerseys, shorts, and pinnies. Because panels are printed digitally before being cut and assembled, individual player names, squad numbers, and custom sizes can be varied within the same 10-piece order at no additional charge.
Virtual 2D/3D artwork proofs are provided within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Once the sample is approved, bulk orders of 300 to 1,000 garments typically ship within 12 to 18 working days directly from our facility.
For match jerseys, we recommend 145–160 GSM 100% Polyester Cool-Max interlock or bird-eye mesh for optimal moisture dissipation. For training gear and shorts, 180–220 GSM micro-mesh or 4-way stretch poly-spandex (88/12 blend) provides enhanced movement and durability during active play.
Yes. We provide complete private-label manufacturing including woven or heat-transfer neck tags, custom branded hangtags, individual barcoded polybags, custom elastic waistbands, and outer carton branding tailored to your brand's specifications.
We support EXW, FOB Shenzhen/Hong Kong, CIF, and full DDP (Delivered Duty Paid) shipping options via express courier (DHL, FedEx, UPS), air freight, and ocean shipping. We deliver routinely across North America, Europe, the UK, Australia, New Zealand, and Asia-Pacific regions.
Engineered for high performance, maximum comfort, and severe durability.