



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our precision-engineered sports apparel. Manufactured utilizing digital dye-sublimation, reinforced multi-needle stitching, and high-tenacity polyester blends.
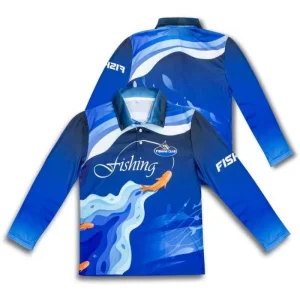
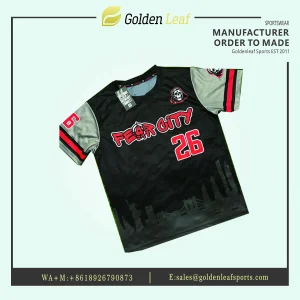
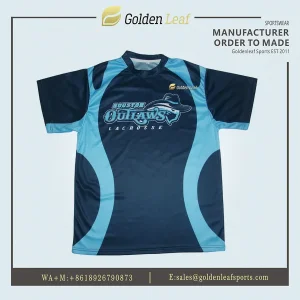
The global rugby apparel market has experienced a profound shift from heavy, water-retentive cotton traditional jerseys to high-performance, engineered synthetic textiles. Modern rugby Union, League, and Rugby Sevens demand uniforms capable of enduring high-impact physical tackles, rapid moisture dissipation, and extreme stretch recovery. As global athletic brand owners, sports clubs, collegiate programs, and league outfits seek optimal balance between durability and player agility, the strategic sourcing focus has centered on specialized China Rugby Jerseys Suppliers & Companies.
The convergence of advanced digital dye-sublimation technology and high-tensile poly-elastane fabric engineering has redefined what institutional buyers expect from OEM/ODM partners. In historical supply chain models, custom cut-and-sew jersey production introduced long lead times, color bleed risks, and high minimum order thresholds. Today, elite Chinese manufacturing ecosystems—spearheaded by specialized hubs in Shenzhen—combine flexible Industry 4.0 production lines with full vertical integration. This enables rapid prototyping, zero-fade customization, and scalable volume output that matches international sporting federation regulations.
Strategic Sourcing Insight: Modern rugby kit procurement is no longer driven solely by unit cost. Professional leagues and distributors prioritize structural burst strength (minimum 280-320 GSM poly-spandex), seam rupture resistance, and color match consistency across repeated reorders (Pantone RIP system alignment).
Moving beyond standard 100% polyester to 280GSM-320GSM heavy interlock knits mixed with 12% Spandex, offering maximum tensile strength against opponent grabbing and tackling.
Digital pre-production sampling delivered within 24-48 hours, coupled with low 10-piece minimum order quantities (MOQ) for custom sublimation orders with zero design compromise.
Comprehensive private label development including heat-transfer woven neck labels, customized silicone grip hems, reinforced collars, and eco-friendly polybag packaging.
Rugby apparel subjects textiles to severe dynamic stresses unmatched in most team sports. Player performance and garment longevity depend on specific technical parameters. Leading Chinese rugby jersey manufacturers deploy rigorous material engineering standards to prevent seam splitting, color degradation, and fabric tearing during intense scrums and rucks.
Unlike standard soccer or running tees (typically 140-160 GSM), professional rugby playing shirts require dual-knit or multi-structure synthetic compositions:
The collar and shoulder yoke are the primary load-bearing points during tackles. Premier factories implement double-pass twin-needle flatlock stitching along all panel joins. Collar styles are specialized into three high-performance profiles:
Reinforced bar-tack stitching at the apex to prevent splitting under forward tension during scrums.
Ergonomic curved collar featuring soft elastic banding to reduce neck friction and tackle grabbing.
Heavy-duty woven canvas collar with rubber safety buttons designed for safety and classic club tradition.
Sublimation printing forces high-grade disperse dyes into the polyester polymer matrix under 200°C heat and intense pressure. GoldenLeaf Sports and leading Chinese suppliers exclusively utilize imported Italian eco-friendly inks that meet OEKO-TEX Standard 100 certification. This guarantees zero toxicity, Grade 4-5 color fastness against washing, UV exposure, and heavy perspiration, ensuring neon and complex gradient team graphics remain bright match after match.
Selecting an OEM partner requires looking into operational resilience, digital workflow automation, and quality management protocols. Over the past decade, Shenzhen has emerged as the world's premier digital sports apparel center, merging tech technology with deep textile manufacturing expertise.
A benchmark facility like GoldenLeaf Sports operating out of Longgang District, Shenzhen, exemplifies this modern industrial capability. Spanning a 3,000 square meter integrated production campus with over 160 skilled technicians, the factory handles every processing stage under one roof:
CAD system size grading ensuring consistent fit across Youth (6Y) to Extended Men's (6XL) sizing blocks.
Raster Image Processing calibrated directly to Pantone Matching System (PMS) to eliminate color shift.
Automated optical camera registration laser cutters sealing synthetic edges while guaranteeing 100% graphic symmetry.
Five dedicated Quality Assurance inspectors auditing fabric tension, print clarity, seam strength, and dimensions.
By controlling fabric sourcing, dye sublimation transfer printing, laser cutting, sewing line assembly, and packaging under single management, leading suppliers reduce production lead times to just 12-18 working days while safeguarding intellectual property and private brand artwork.
Sourcing custom rugby gear from China serves varied downstream business models across tier-one export markets, including Australia, New Zealand, the UK, Ireland, France, the USA, and South Africa. Understanding specific operational requirements ensures seamless procurement outcomes for overseas brand owners and team kit suppliers.
Demands high-compression 300GSM poly-spandex match kits with targeted ventilation mesh underarms, customized silicone waist strips, and player name/number individualization within single bulk production orders.
Requires cost-effective, durable 250GSM interlock fabric capable of surviving weekly heavy wash cycles. Prioritizes quick top-up reorder systems for incoming school rosters across multi-year kit lifecycles.
Focuses on casual heritage rugby polos, oversized fashion fits, custom embroidery badge applications, custom branded inner neck tapes, woven hem tags, and retail-ready barcode packaging.
Logistics & Freight Compliance: Premier suppliers support full Incoterms flexibility—including EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid)—with express air shipment (4-7 days) for urgent league starts or optimized ocean container freight for bulk seasonal stock orders.
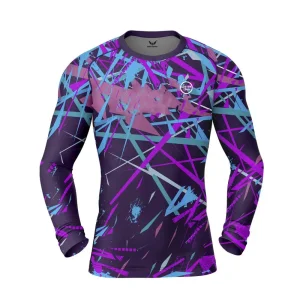
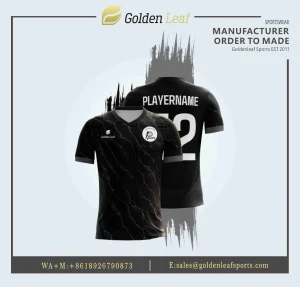
Browse our extended product lines designed for training, activewear, compression support, and club daily wear.
Technical, operational, and commercial insights answered directly by our garment engineering desk.
Our standard minimum order quantity is 10 pieces per design for sublimated rugby jerseys, shorts, and pinnies. Because each panel is digitally printed prior to automated laser cutting, player names, numbers, sponsors, and individual sizes (from Youth 6Y to Adult 6XL) can vary within the same 10-piece batch at no additional charge.
We employ heavy-duty twin-needle flatlock seam joining with high-tensile polyester core thread. All critical pressure points (neck collar join, shoulder yoke, and sleeve seams) undergo bar-tack reinforcement. Our production samples pass ISO burst strength tests exceeding 700 kPa, preventing fabric popping or seam separation during scrums.
Digital mock-up previews are generated within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production for orders ranging between 100 to 2,000 pieces is completed within 12 to 18 working days post-sample sign-off inside our 3,000 m² Shenzhen facility.
Yes, full OEM private-label customization is standard. We provide woven or heat-seal neck labels, customized silicone internal hem grippers (to keep jerseys tucked into shorts), printed hang tags, branded polybags, and custom carton marking aligned with your brand specifications.
We exclusively use non-toxic, imported Italian sublimation inks bonded into 100% polyester micro-fibers at 200°C. Colors achieve Grade 4-5 fastness under ISO 105-C06 testing standards. The graphics become part of the fabric itself, guaranteeing zero cracking, peeling, or fading across seasons of wash cycles.