


GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Verified technical sport garments engineered for active tournaments, high-intensity training squads, and bespoke corporate leagues.
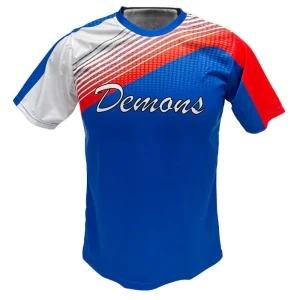
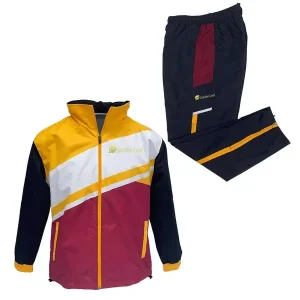
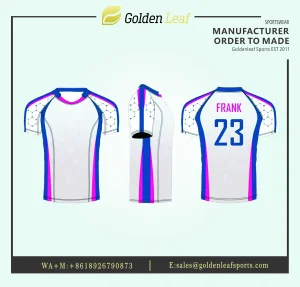
Transitioning from static bulk inventories to agile, zero-inventory print-on-demand networks across the sporting apparel sector.
Traditional athletic apparel supply models bound distributors to capital-intensive stockpiles of pre-numbered uniforms. Modern clubs operate on agile micro-runs, requiring manufacturers capable of on-demand numbering, custom sponsor integration, and dynamic sizing without volume penalization.
Traditional silkscreen and rubberized heat transfers fail under industrial laundry cycles, suffering from cracking and breathability loss. Digital sublimation molecularly infuses non-toxic disperse dyes directly into the synthetic matrix, ensuring zero hand-feel and permanent vibrancy.
Shortened athletic tournament timelines demand compressed prototyping-to-delivery cycles. Chinese integrated factories utilizing computer-aided pattern nesting and laser cutting facilitate rapid transitions from vector CAD approval to international dispatch within 12 to 18 business days.
Harmonizing raw material clusters, precision sewing expertise, and international athletic body specifications across five primary sectors.
Use Case: High school conferences, university intramurals, and scholastic athletic departments requiring durable, budget-conscious, multi-gender kits. Built with reinforced double-needle construction and tear-resistant bird-eye polyester that endures institutional high-temp cleaning.
Use Case: Regional football associations, semi-professional rugby unions, and basketball clubs demanding custom ventilation zoning, antimicrobial finishes, and exact Pantone color consistency across seasonal home, away, and alternate match day sets.
Use Case: Endurance runs, multi-corporate tournaments, and massive community charity events where lightweight, quick-drying 145gsm micro-interlock fabric provides superior evaporation kinetics and unrestricted freedom of movement.
Use Case: Fast-growing youth basketball and lacrosse programs utilizing dual-layer single-garment pinnies and graded size blocks (6Y through 14Y), allowing seamless team-split scrimmages without carrying secondary sets.
Systematic integration of next-generation circular polymers, automated nesting algorithms, and intelligent textile quality inspection.
Expanding GRS-certified rPET yarn options derived from post-consumer plastics, matching tensile strength and dye receptivity of virgin synthetic polymers.
AI-driven visual alignment cameras automatically detect printed panel boundaries, eliminating graphic drift and cutting fabric consumption margins by 14%.
Closed-loop, low-energy sublimation calibration protocols reducing volatile organic compound (VOC) presence to absolute zero and lowering kilowatt footprint.
Conductive thread integration for athletic telemetry and embedded RFID chips in care tags for simplified institutional inventory track-and-trace systems.
Eliminating cross-border friction via strict international material certifications and market-tailored grading charts.
Every dye batch utilized inside our facility complies with strict OEKO-TEX Standard 100 toxicity thresholds. Finished garments are safe for junior skin contact and free from banned azo compounds, heavy metals, and persistent phthalates.
Athletic anatomy varies substantially between geographic operational fields. Our computerized CAD library offers differentiated sizing sets: standard North American roomy blocks, European tailored cuts, and Oceanic rugby/netball reinforced profiles.
Dedicated quality assurance specialists verify order specifics at fiber roll intake, print paper transfer, post-cutting registration, flatlock assembly, and pre-bag packaging to ensure stitch count uniformity and zero dimensional deviance.
Full-spectrum manufacturing capabilities encompassing specialized team gear, motorsports wear, and tournament accessories.
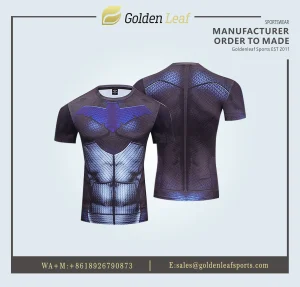
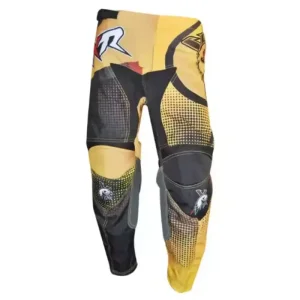
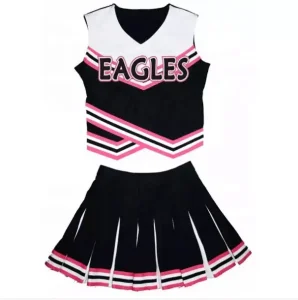
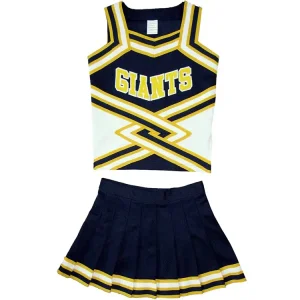
Transparent technical parameters and contracting criteria for international sports apparel procurement heads.
Our standard minimum order quantity is 10 pieces per design. Because our panels are digitally printed on industrial sublimation plotters before precision cutting, you can specify individual player names, numbers, and separate sizes within the same 10-piece run at zero extra surcharge.
Traditional screen printing layers plastisol ink on top of the garment, forming an impermeable rubber barrier that traps body heat and sweat. Full dye sublimation converts ink into a gas under 200°C heat and high pressure, dyeing the internal polyester fibers without obstructing natural airflow pores.
Digital graphic mock-ups are returned within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production orders ranging between 300 and 1,000 pieces typically complete manufacturing within 12 to 18 working days directly from our facility floor.
Yes. We offer turnkey ODM and private-label programs including customized heat-sealed neck tags, woven loop labels, barcode hang tags, recycled branded polybags, and custom master carton shipping marks engineered to match your local distribution hub standards.
For collision disciplines such as rugby and American football, we supply high-tensile 280–320gsm poly-spandex interlock with reinforced seams. For soccer, running, and volleyball, we maintain 140–180gsm micro-mesh and bird-eye knits optimized for moisture evacuation.
We support EXW, FOB Shenzhen/Yantian, CIF, and full DDP door-to-door delivery across North America, Europe, Australia, and New Zealand. Clear tracking documentation and comprehensive visual QA reports accompany every dispatch.
Connect directly with our Shenzhen technical apparel engineering team for vector pattern preparation, fabric weight consultation, and rapid bulk quotation.