GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct factory manufacturing solutions engineered for international sports brands, clubs, and apparel distributors.
Understanding how Chinese technical manufacturers eliminated branding constraints, optimized tensile seam durability, and scaled zero-setup-cost customization for international rugby buyers.
In modern high-impact collision sports like Rugby Union, Rugby League, and Rugby Sevens, athletic teamwear demands an uncompromising balance between structural integrity and visual flexibility. Historically, team outfitters relied on traditional screen printing, vinyl heat transfers, or cut-and-sew fabric panels. These legacy methods presented major operational liabilities for professional procurement officers, team kit managers, and sports brand owners.
Traditional print techniques add physical weight to the garment, impede moisture management by clogging fabric pores, and crack or peel under intensive tackling and repetitive commercial laundering. Furthermore, adding multiple sponsor logos, intricate sleeve badges, club crests, and individual player names exponentially inflated unit costs due to setup screen charges and labor-intensive application steps.
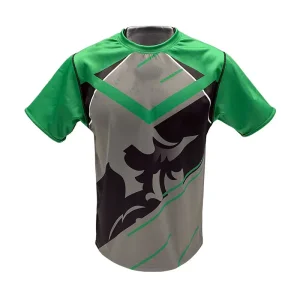
China's specialized OEM/ODM sports apparel manufacturing clusters—most notably centered around Shenzhen and Guangdong Province—have fundamentally disrupted this paradigm through full-dye ink sublimation technology. By transforming vector graphics directly into gaseous dye under high temperature (210°C) and controlled pressure (4.5 bar), color pigments bond permanently with synthetic polyester fibers at the molecular level. The result is a fully customized rugby shirt with unlimited logos, infinite color palettes, and zero extra unit surcharge, maintaining complete breathability and maximum fabric elongation.
A deep dive into vector RIP rasterization, dye-diffusion physics, and flatbed heat press calibration.
Instead of charging per screen or per logo position, our digital pre-press workflow merges 10, 20, or 50 sponsor logos into a unified high-resolution vector print file. Primary crests, sleeve patches, collar motifs, chest sponsors, and back numbers are combined effortlessly within a single CAD layout before printing.
Using premium Italian-formulated Eco-friendly inks (such as Kian or J-Teck), dye particles penetrate deep into the polyester filaments during heat pressing. The ink sublimates directly from solid to gas without entering a liquid state, ensuring zero altered surface texture, zero weight addition, and 100% pore openness for quick-dry moisture evacuation.
Full-dye sublimated rugby jerseys undergo rigorous ISO 105-C06 washing speed tests and ISO 105-B02 artificial light exposure tests. Unlike screen-printed plastic oils that crack under sun exposure or mud friction, sublimated graphics maintain vibrant Pantone accuracy through hundreds of heavy match conditions.
| Performance Metric | Full-Dye Sublimation (China OEM) | Screen Printing | Vinyl Heat Transfer |
|---|---|---|---|
| Logo Quantity Limitation | Unlimited (Included in base unit price) | Restricted (Surcharges per color/location) | Restricted (Surcharges per cut logo) |
| Fabric Breathability & Airflow | 100% Retained (Pores remain open) | Blocked in printed zones | Completely blocked by plastic film |
| Garment Hand-Feel & Weight | Zero added weight; zero surface bump | Heavy, rubbery texture on chest | Stiff patch feel; restrictive movement |
| Durability Under Match Friction | Permanent molecular bond; won't peel | Cracks after 15–20 match washes | Peels under heavy tackling & mud |
| MOQ Flexibility per Design | Low (From 10 pcs with individual player names) | High (Minimum 100+ pcs per print plate) | Medium (Labor-intensive cutting process) |
China's vertical integration from raw yarn spinning to finished custom garment dispatch offers strategic advantages for global B2B procurement.
Chinese mills produce technical rugby textiles designed specifically for collision resistance. Options range from 280 GSM heavyweight interlock to 300 GSM 4-way stretch poly-spandex (88% Polyester / 12% Elastane) with anti-microbial and moisture-wicking treatments.
Equipped with 6-needle 4-thread flatlock machinery and reinforced bar-tack stitching at stress points (armpits, neck tape, side slits), Chinese factories ensure seams withstand over 350 Newtons of pulling force during scrums and rucks.
With automated registration-mark laser cutters and high-speed Japanese Mimaki or Epson 3200 print heads, pre-production physical samples are completed in 3 to 5 business days, cutting product development cycles in half.
Professional exporters deploy inline QA inspectors at every stage: vector art pre-flighting, paper heat transfer verification, panel laser cutting precision check, stitching tension audit, and final needle detection prior to packing.
Key structural innovations driving global demand across Rugby Union, Rugby League, and Sevens tournaments.
The global rugby market has transitioned away from traditional heavy cotton shirts toward skin-tight or semi-athletic polyester elastane jerseys. Modern elite players require apparel that opponents cannot easily grab during a tackle. Chinese manufacturers utilize 3D body-mapping pattern software to produce ergonomic panels that flex naturally with shoulder rotation and torso extension.
Collar tearing is one of the most common failure points in rugby teamwear. Leading exporters engineer several collar variations customized to match level and budget:
With data analytics becoming standard across professional and semi-pro leagues, rugby shirts now frequently feature an internal mesh pouch located between the shoulder blades. This tailored pocket securely holds GPS tracking units without causing chafing or movement distraction.
Tailored manufacturing strategies for sports brands, university leagues, corporate tournaments, and private label distributors.
High-volume orders requiring strict Pantone color matching (Delta-E < 1.0), serialized player numbering, custom sleeve sponsors, and exact sizing consistency across Senior, Academy, and Youth tiers.
Demands durable 280 GSM fabrics that endure tough multi-season wear and commercial laundry cycles, bundled with matching shorts, socks, and sideline training jackets under unified branding.
Complete brand localization options including custom woven neck tags, heat-seal care labels, custom silicone chest logos, branded polybags, and FSC-certified barcode packaging ready for retail distribution.
Direct technical answers from our engineering team regarding fabric weights, lead times, artwork vector files, and export logistics.
Expand your brand's offering with fully sublimated technical performance garments manufactured to match your custom rugby range.