GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our technical sportswear product line engineered in our 3,000 m² Shenzhen manufacturing facility with high-precision digital sublimation and zero-fade color technology.
Data-backed operational efficiency and production standards operating out of Shenzhen's premier textile innovation hub.
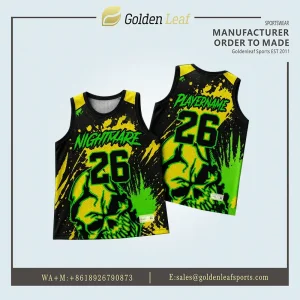
In the contemporary landscape of athletic performance wear, traditional garment decoration methods—such as screen printing, heat-transfer vinyl, and direct-to-garment (DTG) printing—have increasingly yielded ground to full digital dye-sublimation technology. For procurement managers, team outfitters, and sportswear brand directors searching for trusted China Sublimation Basketball Jersey Suppliers & Manufacturers, understanding the material science and economic dynamics behind this transition is essential for securing a competitive advantage in the global market.
Unlike surface-level print applications, thermal dye-sublimation relies on a precise solid-to-gas phase molecular transformation. Disperse dyes are printed onto high-release transfer paper via digital inkjet plotters using specialized RIP (Raster Image Processor) software. Under high-calender heat pressing (typically 190°C to 210°C at 4 to 6 bar pressure), the synthetic polyester fibers undergo thermal expansion, opening their polymer structure. Simultaneously, the dye solid sublimate directly into a gaseous state without entering a liquid phase, bonding irreversibly into the core of the micro-polyester filaments. The result is an ultra-durable, zero-hand-feel graphic that becomes an integral part of the fabric itself.
| Performance Feature | Full Dye-Sublimation Printing | Traditional Screen Printing | Heat Transfer Vinyl (HTV) |
|---|---|---|---|
| Breathability & Wicking | Uncompromised; zero weight addition | Heavy ink deposit blocks mesh pores | Solid film creates heat trapped areas |
| Color Fastness (ISO 105) | Grade 4.5 – 5.0 (Extreme wash resistance) | Grade 3.0 – 4.0 (Fades after 20+ washes) | Grade 2.5 – 3.5 (Peels under high heat dryer) |
| Roster Personalization | 100% variable data (Names/Nos) at 0 cost | High screen charge per individual player | Labor intensive; high cost per unit |
| Graphic Resolution | Photo-realistic (Up to 1440 DPI) | Limited color layering; coarse vector | Vector shapes only; no subtle gradients |
| Garment Stretchability | Expands naturally with 4-way stretch poly | Prone to cracking under tension | Restricts fabric elasticity and movement |
A superior sublimated jersey is only as good as the underlying substrate. Leading Chinese manufacturers like GoldenLeaf Sports (Shenzhen) Co., Ltd. leverage advanced synthetic yarn engineering to supply customized fabric compositions tailored specifically for modern, explosive basketball dynamics.
During competitive basketball games, players experience quick lateral shifts, vertical leaps, and constant contact, generating significant metabolic body heat and moisture. Fabric selection must strike a precise balance between tensile durability, hydro-phobic moisture dispersion, and lightweight comfort.
Engineered with micro-perforations that create a 3D capillary structure. Rapidly channels sweat away from the epidermis to the fabric exterior where ambient airflow accelerates evaporation. Ideal for basketball jerseys, summer practice pinnies, and high-intensity training singlets.
A tight double-knit weave offering a smooth, matte finish with outstanding print sharpness. Perfect for premium pro-cut basketball jerseys requiring sharp line graphics, vivid neon gradients, and extreme tear resistance against jersey-grabbing defense.
Utilized primarily in modern tight-fit basketball compression shorts, side accent paneling, and elastic waistbands. Provides 360-degree anatomical recovery, reducing muscle oscillation while preventing mechanical binding during deep defensive slides.
The global sportswear procurement landscape has evolved beyond mere labor-cost arbitrage. Modern overseas buyers—including North American team dealers, European sports distributors, and Australian club brand managers—require uncompromising quality control, speed-to-market, and flexible minimum order quantities (MOQ).
Shenzhen, China, has established itself as the world’s epicentre for high-tech digital textile manufacturing. The concentration of specialized supply chains within a 50-kilometer radius enables unprecedented operational efficiency:
Tailored sublimated sportswear engineering configured to meet the distinct structural, sizing, and regulatory standards of major global regional markets.
Demands: Extended torso lengths, wide armhole drop cuts, heavy-duty flatlock 4-needle 6-thread seam construction, and fast 10-14 day turnarounds between regional tournament qualifiers.
Factory Execution: Graded US standard size blocks (Standard American Fit), reinforced neck ribbing, and pre-sorted player-pack polybagging for instant roster distribution upon delivery.
Demands: Strict compliance with FIBA uniform guidelines regarding number dimensions (front/back), sponsor patch placement zones, athletic slim-fit silhouettes, and eco-certified materials.
Factory Execution: Custom Euro-fit pattern blocks, precise Pantone PMS C matching for corporate sponsor compliance, and OEKO-TEX certified micro-mesh fabrics.
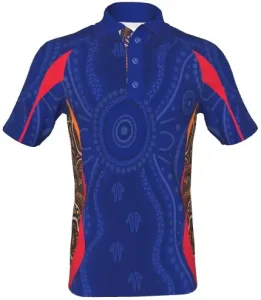
Demands: High UV radiation protection (UPF 50+ rating), dual-layer reversible basketball singlets, and intricate cultural or Indigenous art print capability.
Factory Execution: Ultra-lightweight double-layer bird-eye mesh (140 GSM per side) preventing bleed-through, vector artwork resolution up to 1400 DPI, and UPF-treated yarn integration.
Expert technical insights provided directly by our apparel engineering desk for international buyers and procurement heads.
Our standard production MOQ is 10 pieces per design for full sublimated jerseys, shorts, or team kits. Because digital sublimation prints directly onto raw fabric panels before cutting, each garment within the 10-piece run can feature individual player surnames, roster numbers, and custom sizes (e.g., S to 5XL) at no extra cost.
We operate strictly on the Pantone Matching System (PMS C Solid Coated). Our prepress team uses dedicated RIP color-profiling software calibrated to our specific digital plotters, heat-transfer presses, and micro-polyester fabrics. We offer solid color swatches on physical fabric for volume buyers prior to full production runs.
Digital 2D/3D artwork proofs are rendered within 24 to 48 hours. Pre-production physical samples take 5 to 7 working days. Bulk manufacturing for orders of 100 to 1,000 units is typically completed in 12 to 18 working days. Express courier shipping via DHL/FedEx takes 3 to 5 business days globally.
Yes. We offer comprehensive OEM/ODM private label services. This includes custom sublimated or woven neck labels, heat-seal size transfers, custom hangtags, branded edge taping, individual printed polybags, and custom barcoded packaging tailored for Amazon FBA, Shopify sellers, or retail store drop-shipping.
Because sublimation dyes are permanently bonded into the polyester core at a molecular level, our garments achieve an ISO 105 color fastness rating of Grade 4.5 or higher. They will not bleed, fade, crack, or peel even after 100+ commercial wash cycles in high-temperature laundry setups.
Every production batch undergoes a 5-stage Quality Assurance protocol adhering to AQL 2.5 standards: 1) Raw fabric flaw & GSM check, 2) Paper press color alignment, 3) Registration laser-cut dimensional verification, 4) Seam pull stress testing, and 5) Final 100% manual inspection for loose threads, size accuracy, and correct spelling of player names.
Explore our full ecosystem of sublimated team kits, activewear bottoms, and specialized athletic apparel manufactured to global export standards.
Connect directly with our senior textile technicians in Shenzhen for instant vector mockups, fabric sample swatches, and factory-direct B2B quotation pricing.