GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
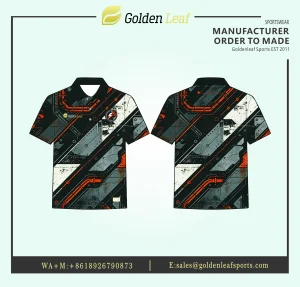
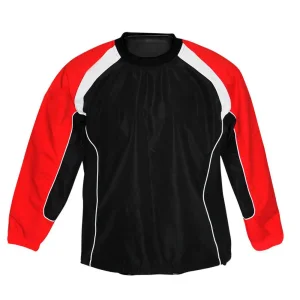
Explore our high-performance customized athletic apparel portfolio engineered with Italian sublimation inks and high-tenacity polyester knits.
A Macro Perspective on Technological Convergence, Fan Engagement Dynamics, and Supply Chain Modernization in the Global Cricket Market.
The global cricket fanbase represents one of the largest and most passionate sports ecosystems in the world. Spanning traditional powerhouses across South Asia, Australasia, the United Kingdom, and the Caribbean, while experiencing rapid commercial expansion in North America (via Major League Cricket) and the Middle East, cricket has evolved from a seasonal pastime into a multi-billion-dollar global merchandise market. For brands, franchise leagues, fan clubs, and retail chains, sourcing high-performance, custom cricket fanbase apparel demands a sophisticated blend of textile engineering, vibrant visual customization, rapid-turnaround capabilities, and cost-efficient mass manufacturing.
Why Shenzhen’s Precision Manufacturing Ecosystem Delivers Unmatched Quality, Cost Efficiency, and Speed-to-Market for Cricket Fanware.
Our Shenzhen manufacturing hub leverages direct proximity to elite yarn mills, specialized dye houses, high-speed sublimation paper producers, and precision hardware suppliers, slashing component lead times by over 40%.
Equipped with high-precision EPSON and MIMAKI digital sublimation printers utilizing imported non-toxic Eco-inks. We guarantee brilliant Pantone color reproduction with a strict color deviation tolerance (ΔE < 1.5).
Every batch of cricket fan jerseys, polos, and fan accessories undergoes strict 5-stage quality audits: raw fabric tension tests, pre-print digital art verification, post-transfer color check, seam strength evaluation, and final packaging audit.
Whether you require a trial order of 10 customized squad pieces for a local fan club or a 50,000-unit bulk shipment for an international stadium giveaway, our automated laser cutting and modular assembly lines deliver uncompromised precision.
End-to-End OEM & ODM Frameworks Engineered for Global Brands, E-Commerce Retailers, and Sports Organizations.
Navigating the modern sports merchandise landscape requires far more than basic garment assembly. Global brands and franchise operators require strategic supply chain integration that reduces inventory risk while maximizing customer satisfaction. GoldenLeaf Sports delivers comprehensive, turnkey macro solutions tailored specifically to the global cricket fanbase marketplace:
| Solution Category | Target Client Profile | Core Technical Capabilities | Strategic Value Delivered |
|---|---|---|---|
| Franchise League Turnkey Merchandising | Tournament Organizers, Franchise Owners, Official Retail Distributors | Full ODM design suite, mass dye-sublimation, official hologram/hangtag integration, customized player roster dropshipping. | Ensures 100% official brand compliance, eliminates stockouts during peak match weeks, and secures maximum profit margins. |
| On-Demand Fan Club POD (Print-on-Demand) | E-Commerce Brands, Online Supporter Stores, Regional Fan Clubs | Low-MOQ flexibility (from 10 pcs/design), individual name/number customization, digital proofing within 24 hours. | Zero excess inventory liability, infinite customized SKU generation, rapid global direct-to-door delivery options. |
| Corporate Sponsor & Event Activation Kits | Global Brand Sponsors, Tournament Hospitality Providers | Co-branded cricket polos, sublimation flags, caps, bomber jackets, promotional fan giveaway sets. | High brand visibility in broadcast coverage, superior tactile comfort for VIP attendees, bulk cost optimization. |
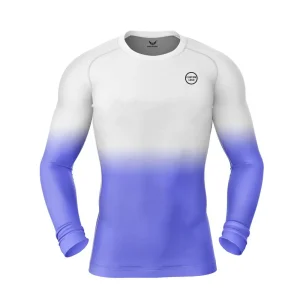
| Amateur Club & Grassroots Teamware | School Academies, Regional Cricket Leagues, Community Clubs | Multi-garment matching sets (playing whites, T20 kit, travel polos, compression base layers, socks). | Standardized club color matching across all apparel lines, durable reinforced construction built for intense match play. |
Tailoring Material Performance, Fit Specifications, and Visual Aesthetic to Diverse Worldwide Cricket Markets.
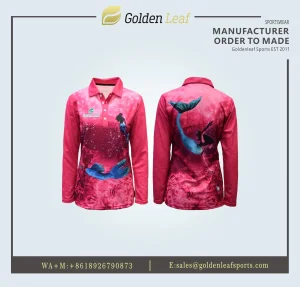
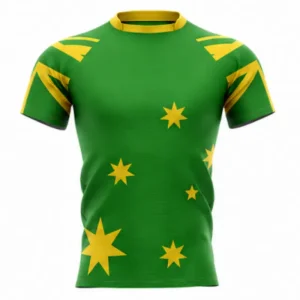
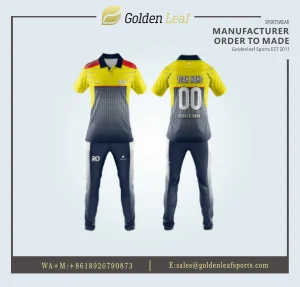
Scenario focus: High-humidity matchday comfort and intense visual vibrancy. Engineered with 145 GSM micro-mesh polyester featuring ultra-fast drying rates to keep millions of fans cool in tropical stadium environments.
Scenario focus: Premium heavy-duty polos, outerwear, and traditional whites. Utilizing 180 GSM interlock knits and thermal fleece bomber jackets designed for chilly early-season conditions in England and Southern Australia.
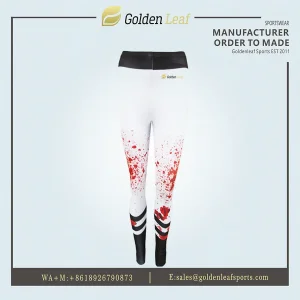
Scenario focus: High-fashion lifestyle sportswear fusion. Incorporating relaxed-fit streetwear cuts, customized baseball-style cricket jerseys, and athletic compression tights tailored for North American sporting tastes.
A Professional Standard Operating Procedure Guide for Corporate Sourcing Directors and Apparel Buyers.
When sourcing custom cricket fanbase products at scale, professional buyers must evaluate factory capability across stringent parameters. GoldenLeaf Sports operates under audited international quality frameworks, ensuring seamless import compliance and long-term product durability:
Expert Answers to Critical Sourcing Questions Regarding Custom Cricket Apparel Production, Logistics, and Quality Control.
GoldenLeaf Sports (Shenzhen) Co., Ltd. operates a dedicated 3,000 m² apparel manufacturing facility with 14+ years of expertise. Unlike general trading companies, we manage the complete production chain under one roof: artwork vectorization, RIP color management, digital sublimation printing, high-temperature heat transfer, automated laser cutting, sewing line assembly, and strict 5-stage QC inspection. This vertical integration allows us to deliver high-volume stadium merchandise and boutique fan club collections with unmatched speed and consistency.
Our standard MOQ is just 10 pieces per design for custom sublimated cricket jerseys, polos, shorts, and pinnies. Because each panel is printed digitally prior to cutting, you can customize individual player names, supporter numbers, and sizing inside the same 10-piece order without incurring setup surcharges. For large franchise orders, our facility scales seamlessly to produce over 300,000 units annually.
Dye-sublimation infuses eco-friendly inks directly into the polyester fabric fibers using intense heat and pressure. This results in zero added weight, 100% breathability, and an infinitely soft hand-feel. Unlike screen printing or heat-seal vinyl, sublimated designs will never crack, peel, bubble, or fade over time, even after repeated industrial laundering and prolonged exposure to tropical sunlight.
We provide 24 to 48-hour turnarounds on digital 3D vector artwork mock-ups. Once artwork is approved, physical pre-production samples are completed in 5 to 7 working days. Bulk production orders of 300 to 1,000 pieces typically ship in 12 to 18 working days following signed sample approval.
Yes. We offer complete ODM and private-label OEM manufacturing solutions. This includes woven neck labels, heat-transfer inner tagless size labels, customized hangtags, barcoded polybags, custom-branded zippers, and branded master cartons ready for direct retail distribution.
We regularly export under EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid) terms. We ship worldwide via express courier (DHL, FedEx, UPS), air freight, and sea freight. Payment options include T/T wire transfer, Western Union, and secure Alibaba Trade Assurance.
Discover our complementary athletic product range, engineered with the same quality and precision craftsmanship.
Partner with China’s leading custom sportswear and fanbase apparel factory. Receive free digital 3D vector mock-ups, factory-direct bulk pricing, and full sample assistance within 24 hours.
Request Factory Quote & Catalog