GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct factory options built for U.S. clubs, university leagues, distributors, and private brands utilizing high-precision digital sublimation and technical fabrics.
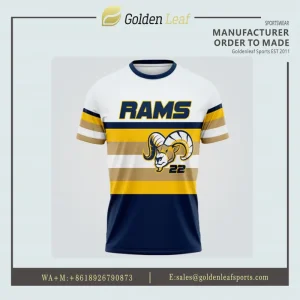
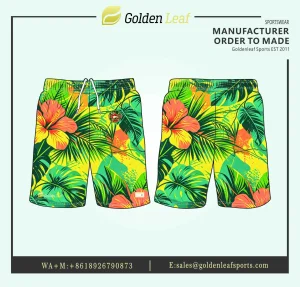
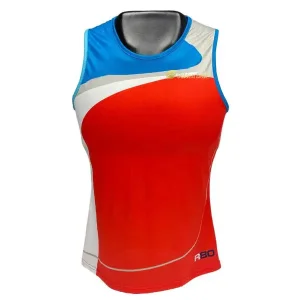
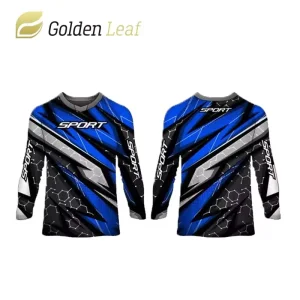
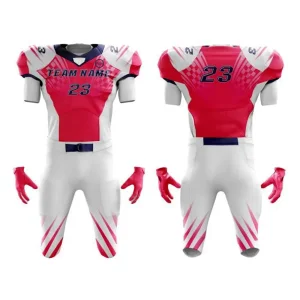
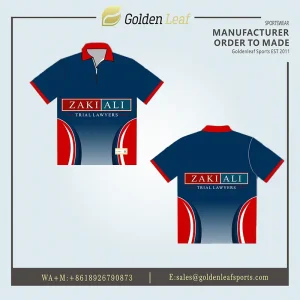
As North American athletic leagues, high school associations, and professional club organizations demand rapid-turnaround customization, traditional screen printing and vinyl applique are giving way to edge-to-edge digital sublimation technology.
The athletic apparel market in the United States is undergoing a structural transformation. Driven by shifts in athlete performance science, direct-to-consumer brand agility, and corporate sustainability mandates, American sports apparel companies are recalibrating their supply chain partnerships. Buyers are moving away from stock, pre-dyed blanks toward fully customized OEM/ODM digital sublimation lines manufactured with precise structural engineering.
For the 2025–2026 competitive seasons, U.S. collegiate and club athletic programs are establishing strict technical baselines for thermoregulation. Single-layer standard polyesters are rapidly being replaced by multi-channel bird-eye mesh, 145–180 GSM polyester interlock, and 4-way stretch poly-spandex (88/12) fabrics. These modern materials feature enhanced capillary wicking rates exceeding 0.18 g/s, keeping athletes cool during high-intensity play while ensuring lightweight structural integrity.
High holding costs and unpredictable roster changes have forced U.S. sports apparel distributors to abandon large-volume pre-printed inventory models. Brands are transitioning to agile sublimation pipelines where rosters, individualized player names, numbers, and sponsor arrangements can be adjusted on demand. Manufacturing facilities like GoldenLeaf Sports, equipped with digital RIP software and laser-cutting technology, can execute individualized 10-piece team runs without imposing setup surcharges or extended lead times.
The boundary between high-performance on-field uniforms and urban daily wear has blurred. Products initially engineered for specific disciplines—such as performance frisbee shorts, breathable racing polos, and tailored baseball jerseys—are being adopted into casual streetwear catalogs. U.S. apparel companies are ordering athletic garments built with flatlock anti-chafing seams, ergonomic side-split hems, and refined rib-knit collars that transition seamlessly from competitive arenas to lifestyle spaces.
Environmental compliance regulations across North America—including FTC green guidelines and California Proposition 65—require sports apparel companies to verify non-toxic chemical usage throughout their supply chains. Leading factories now utilize OEKO-TEX certified, imported water-based sublimation inks. These inks bond at a molecular level with high-grade polyester fibers, maintaining vibrant pantone fidelity (Grade 4+ wash fastness) while emitting zero heavy metals or volatile organic compounds (VOCs).
Diversity in body morphology demands flexible pattern engineering. Custom team wear programs require precise size scaling to accommodate diverse athlete profiles without sacrificing comfort or hydrodynamic silhouette. Advanced pattern libraries now feature separate female-specific contours, youth-graded proportions (6Y–14Y), and extended plus-size blocks (up to 5XL) with modified shoulder pitches and armhole depth controls.
How GoldenLeaf Sports aligns enterprise OEM/ODM capabilities with North American compliance standards and technical performance criteria.
Comprehensive raw material stock including 100% polyester interlock (145-180 GSM), open bird-eye mesh, micro-porous cool-max knits, heavyweight rugby twill, and 4-way stretch poly-spandex blends tested for color fastness and anti-pilling durability.
5-person dedicated QA inspector line executing pre-print paper alignment checks, temperature-controlled sublimation monitoring (200°C–215°C), laser-cut registration accuracy, and 100% finished garment needle/stitch integrity verification.
End-to-end global trade support under EXW, FOB Shenzhen/Yantian, CIF, and DDP terms with direct air express delivery to U.S. distribution hubs within 3-5 business days post-production completion.
| Performance Characteristic | Legacy Screen Print / Vinyl Transfer | GoldenLeaf Sublimation Standard (2025–2026) | U.S. Enterprise Procurement Benefit |
|---|---|---|---|
| Graphic Breathability | Blocks mesh pores; causes heat build-up | Zero pore blockage; ink fuses at molecular level | Enhanced athlete endurance & thermal control |
| Peeling & Cracking Risk | High after 15-20 industrial wash cycles | Zero peeling; Grade 4.5 wash/light fastness | Extended garment lifespan; zero warranty claims |
| Roster Personalization | Expensive screen setups per name/number | Included dynamically in single digital print run | Simplified ordering; low-MOQ viability (10 pcs) |
| Production Lead Time | 3-5 weeks requiring multi-step physical setups | 12-18 days direct from 3,000 m² Shenzhen campus | Accelerated time-to-market for sport seasons |
Pioneering smart manufacturing technologies to deliver unparalleled precision, sustainability, and dynamic custom teamwear.
Integrating direct CAD-to-RIP software pipelines that map vector graphics across complex 3D human body scans. This cuts pre-production digital proofing times down to 24–48 hours while eliminating artwork distortion across seams.
Deploying automated optical cameras on laser-cutting tables to track registration marks in real time. This guarantees alignment of dynamic side-panel stripes and geometric team logos down to the millimeter.
Essential operational details regarding minimums, production timelines, custom private labelling, and material standards.
From casual practice gear to technical multi-sport apparel, review our factory-direct custom options engineered for performance and endurance.