GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our precision-engineered custom apparel solutions, built with high-grade sublimation, moisture-wicking polymers, and ergonomic fits for global brands and sports clubs.
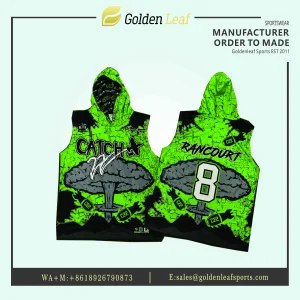
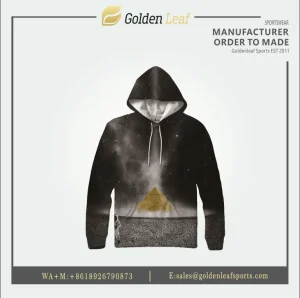
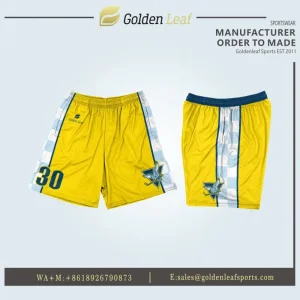
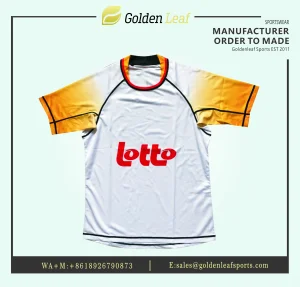
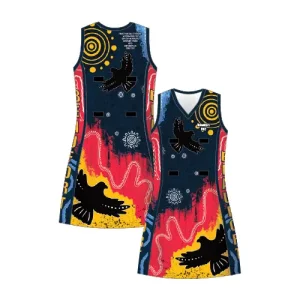
The global market for custom hoodies and bespoke teamwear has undergone a structural transformation. Driven by the convergence of streetwear aesthetics, e-sports branding, corporate promotional merch, and elite athletic training wear, hoodies are no longer simple leisure garments. They have evolved into complex functional apparel items demanding high technical precision in fabric weight (GSM), fiber elasticity, digital color calibration, and structural durability.
For global apparel distributors, streetwear labels, and sports organizations, sourcing from professional custom hoodies suppliers requires a deep evaluation of production methodologies. Modern buyers demand seamless integration between **Heavyweight Cotton Fleece (350–500 GSM)**, **Performance Poly-Spandex Interlock**, and high-precision **Digital Sublimation Printing** that withstands hundreds of commercial wash cycles without color degradation or fabric pilling.
GoldenLeaf Sports (ShenZhen) Co., Ltd., operating from a state-of-the-art **3,000 m² modern manufacturing hub** in Shenzhen, China, stands at the forefront of this industrial shift. With over 14 years of OEM/ODM expertise, an elite workforce of 160 specialized garment technicians, and an annual production capacity exceeding **300,000 customized pieces**, GoldenLeaf bridges the gap between low-volume boutique customization and scalable industrial mass production.
Our integrated supply chain matrix guarantees strict adherence to international quality standards, offering flexible Minimum Order Quantities (MOQs starting at just 10 pcs/design), rapid 24–48 hour digital proofing, and comprehensive private-label package solutions for corporate and athletic buyers worldwide.
Why tier-1 global apparel brands and professional sports clubs rely on Shenzhen's specialized textile clusters for OEM/ODM hoodie production.
Located within the Pearl River Delta apparel mega-cluster, our facility accesses premium combed cotton, French Terry, brushed fleece, and eco-friendly recycled polyester (rPET) yarns within hours. This proximity reduces raw material lead times by up to 60% compared to secondary apparel hubs.
We utilize imported, non-toxic, eco-friendly dye-sublimation inks mated with high-resolution Japanese printing heads. Our precise RIP color calibration guarantees exact Pantone color matching (Grade 4+ color fastness), zero color fading, and odorless, skin-safe finished products.
Our cutting floor employs automated optical-registration laser cutters that read edge alignment markers directly off printed panels. This eliminates human cutting variance, ensuring side-seam alignment, seamless pocket stitching, and perfect panel assembly across size S to 5XL.
Tailored apparel engineering adapted to distinct regional demands, market regulations, and sub-cultural aesthetics across key global territories.
High demand for heavy-weight 400–450 GSM organic French Terry hoodies featuring drop-shoulder silhouettes, double-layer lined hoods, puff printing, embroidery patches, and custom dip-dyed drawstrings for streetwear brands and college sports fanwear.
Focus on sustainable GOTS-certified organic cotton blends, minimalist high-density rubber print logos, subtle tone-on-tone embroidery, REACH compliance, and tailormade slim-fit cuts suited for corporate tech companies and European football club travel gear.
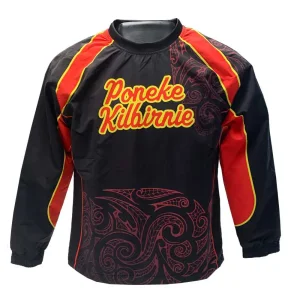
Performance-focused lightweight (260–300 GSM) moisture-wicking fleece and poly-spandex blend hoodies built for rugby, netball, and outdoor sports clubs requiring vibrant sublimated club artwork, anti-UV protection, and reinforced flatlock stitching.
How GoldenLeaf Sports is driving innovation in smart textile engineering, AI-powered pattern generation, and closed-loop sustainable manufacturing.
Integrating CAD auto-nesting software and 3D digital simulation engines to generate virtual 3D garment samples within 24 hours. Reduces physical sampling fabric waste by over 75% and drastically accelerates client pre-production approvals.
Pioneering phase-change thermal fleece fabrics and hydrophobic outer coatings that offer waterproof performance without sacrificing breathability. Incorporating 100% biodegradable micro-polyester to eliminate micro-plastic shed during washing cycles.
Upgrading sewing workstations with computer-guided robotic sewing arms for complex panel assembly, automated pocket setters, and real-time AI vision quality inspection to achieve near-zero defective rates during high-speed production runs.
Eliminating risks for international buyers through end-to-end quality control, global certifications, and private-label full package services.
Every individual hoodie passes through 5 dedicated QA/QC checkpoints: raw fabric inspection, print alignment verification, pre-sewing dimension checking, needle-detector scanning, and final packaging audit before factory clearance.
We provide comprehensive shipping terms including EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid). Through strategic partnerships with DHL, FedEx, and international ocean freight lines, customs clearance is hassle-free.
Elevate your brand with full turnkey customization: custom woven neck tags, heat-transfer size labels, branded hangtags, custom polybags with barcode printing, and personalized master-carton packaging tailored for direct-to-retail fulfillment.
In-depth answers to critical procurement, production, and technical queries directly from our apparel engineering desk.
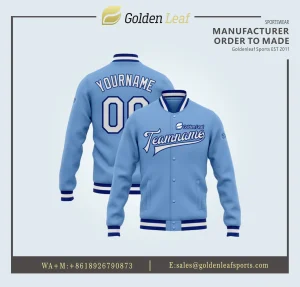
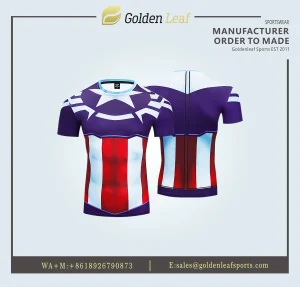
Discover our specialized lines for baseball jackets, rugby gear, training t-shirts, frisbee wear, and high-visibility athletic apparel.