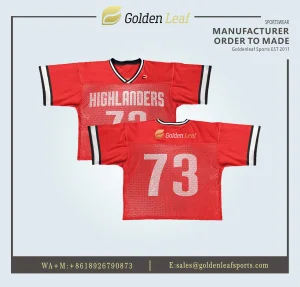
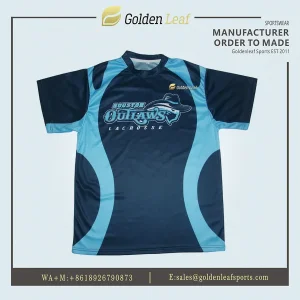
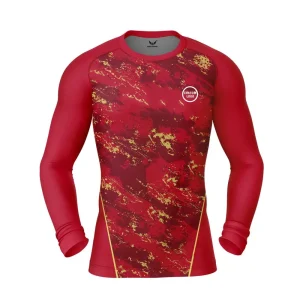
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our top-tier precision sublimated gear engineered for professional performance, dimensional stability, and vivid color permanence.
Modern athletic wear manufacturing has undergone a seismic shift from traditional screen printing and vinyl application to full-bleed digital dye-sublimation. Modern basketball organizations demand lightweight, highly breathable apparel that retains structural integrity under rigorous physical gameplay while delivering unlimited visual customization.
The global demand for custom logo sublimation basketball jerseys is anchored by a convergence of sports apparel technology, decentralized digital brand scaling, and the rapid expansion of professional, semi-professional, and academic athletic leagues. Unlike legacy garment customization techniques—where rubberized inks block fabric pores and deteriorate after repetitive washing—dye sublimation represents a molecular chemical bonding process. Disperse dyes transition directly from a solid state into a gas under controlled thermal calibration (typically 190°C to 210°C) and pressure, fusing directly into the synthetic polymer chains of polyester fibers.
From an industrial supply chain standpoint, the modern factory must function not merely as a cut-and-sew workshop, but as an integrated high-tech digital print and textile engineering hub. The ecosystem encompasses high-resolution vector artwork rasterization, color management profiles optimized for specific fabric densities (ranging from 145 GSM featherweight bird-eye mesh to 220 GSM heavyweight interlock poly-spandex), automated laser cutting to prevent fraying, and ergonomic multi-needle flatlock stitching. Factories that master this end-to-end pipeline deliver unmatched information gain to brand owners: total design freedom, zero weight addition from logos or numbers, and perfect moisture-management functionality.
How advanced material science, eco-conscious chemistry, and automated digital workflows are defining the next generation of sublimated athletic uniforms.
Transitioning from virgin polyester to post-consumer recycled PET bottles. High-tensile rPET micro-mesh engineered specifically to withstand sublimation temperatures without fiber degradation or thermal yellowing.
Utilization of non-toxic, eco-certified Italian Kiian/Kian dye inks. Delivers ultra-wide color gamuts, deep rich blacks, and crystal-clear neon gradients while meeting OEKO-TEX Standard 100 toxicological safety standards.
Automated vision-guided laser cutting machines read printed registration marks on heat-transferred panels. Eliminates human error in panel sizing, ensuring 100% pattern consistency across XS to 6XL sizing.
A crucial technical metric in basketball teamwear is moisture management. Standard sublimated fabrics often lose breathability if low-grade inks create a film on top of the weave. Advanced sublimation factories utilize capillary-action engineered fibers combined with high-purity disperse inks. This maintains 100% open pore structures in the polyester weave (such as bird-eye or pinhole mesh), allowing sweat to wick rapidly away from the athlete’s skin to the outer surface for flash evaporation during peak intense physical play.
Tailored manufacturing setups optimized for diverse global markets, athletic organizations, and retail channels.
Requires strict adherence to athletic league rules (e.g., NCAA, NFHS size and placement specifications for player numbers, team logos, and manufacturer tags). Demands high durability to endure multi-season laundry cycles and physical contact.
Demands custom tailored athletic fits, body-mapped mesh paneling, anti-bacterial treatments, and complex sponsor integration. Features high-resolution sponsor placement across chests, backs, and shorts without added weight.
Focuses on heavy vintage aesthetics, oversized 90s basketball cuts, metallic/neon sublimation elements, and retail-ready private labeling including custom woven neck tags, hangtags, and custom printed polybags.
Requires fast-turnaround batch orders (often 7–10 days) with vibrant, hyper-graphic visual themes. Reversible single-layer sublimated pinnies and lightweight tank tops are dominant choices.
Requires cost-effective bulk production paired with soft, non-abrasive fabrics for young players. Easy re-order capability for individual player roster replacements throughout the season.
Custom co-branded uniforms featuring high-precision corporate identity vector matching (Pantone matching), relaxed fit blocks, and matching accessory bundles (socks, caps, hoodies).
Anticipating the convergence of artificial intelligence design tools, zero-water thermal printing, and smart athletic apparel.
Implementation of generative AI engines that render instant 3D virtual garment mockups. Integration of automated pattern grading software that automatically adjusts logo scale dynamically according to jersey sizes (from 3XS to 6XL) to preserve precise visual proportions.
Near-zero carbon emission production lines utilizing waterless dye sublimation systems. Direct-to-fabric disperse printing with zero chemical runoff, reducing factory environmental footprint by over 80% while increasing color vibrancy.
Embedded phase-change materials (PCM) inside the poly-spandex matrix for active micro-climate body temperature regulation. Seamless integration of flexible RFID micro-chips into heat-sealed hem tags for real-time inventory tracking and authentic game-worn validation.
How a leading B2B basketball jersey factory solves supply chain bottlenecks, quality volatility, and ordering friction for global buyers.
For global sportswear distributors, apparel brands, and league procurement managers, working with a factory requires more than just manufacturing capacity—it demands comprehensive operational reliability. A superior custom logo sublimation basketball jersey supplier acts as an extension of your own engineering team. Below is our blueprint for macro-level manufacturing solutions:
Eliminating traditional high minimum order requirements. Offering flexible MOQs starting at 10 pieces per design, allowing brands to test niche markets or quickly restock individual roster slots without maintaining excess inventory carrying costs.
Utilizing spectrophotometers to calibrate ink output against Pantone Solid Coated standards. Ensures that brand colors remain 100% consistent across different fabric weights, orders, and production seasons.
Turnkey OEM/ODM fulfillment including custom sublimated or woven neck labels, branded barcode hangtags, individual eco-friendly polybag packaging, and custom master carton labeling ready for direct warehouse dispatch.
Deep technical clarity on vector artwork specifications, fabric GSM selection, durability benchmarks, and international shipping.
Browse our comprehensive OEM/ODM line spanning training gear, multi-sport uniforms, hoodies, and event merchandise.