GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered to meet rigorous athletic standards, our core product series leverage zero-bleed digital sublimation, optimized GSM polyester knits, and anti-friction flatlock seam construction.
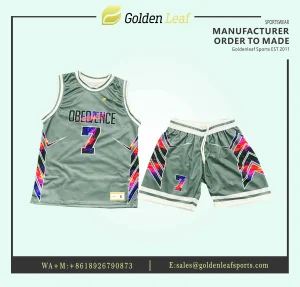
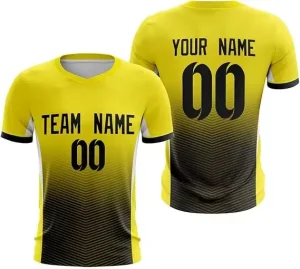
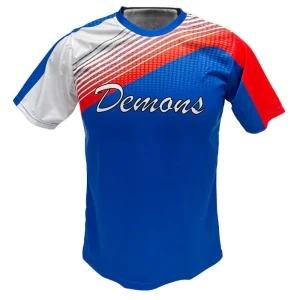
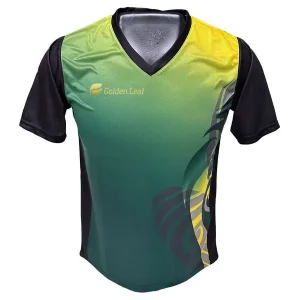
The global educational sports apparel industry has transitioned from standardized, bulk-dyed cotton garments to highly technical, digitally customized polymer systems. Institutional athletic directors, school boards, and regional teamwear distributors face unprecedented requirements: uniforms must deliver professional-grade thermoregulation, survive severe commercial laundering cycles, comply with stringent regional safety standardizations (CPSIA, REACH), and incorporate intricate institutional branding without inflating procurement budgets.
As a specialized Custom School Sports Uniforms Manufacturer & Factory, GoldenLeaf Sports operates at the intersection of digital textile engineering and agile manufacturing. Based in Longgang District, Shenzhen, our vertical production paradigm addresses the classic procurement dilemma—balancing low Minimum Order Quantities (MOQs), ultra-fast turnaround times, precise color matching (Pantone PMS integrity), and zero-defect structural craftsmanship.
Information Gain Metric: Standard screen-printed school uniforms lose structural elasticity and experience ink degradation after 20 to 30 industrial washes. Molecularly bonded sublimation printing into high-multi-filament polyester matrices maintains 100% tensile strength and color vibrancy beyond 150+ high-temperature wash cycles.
School sports apparel is not a one-size-fits-all commodity. Global regional mandates dictate specific dimensional, safety, and visual design parameters for school kits across K-12 and collegiate levels.
Focus: NFHS & NCAA Rulebook Compliance
US High School athletic programs demand strict adherence to National Federation of State High School Associations (NFHS) rules. Basketball uniforms mandate solid-color torsos and contrast number borders; soccer jerseys require clear home/away color separation. All youth sizes must pass CPSIA tests for lead content (<100 ppm) and zero phthalates in elastic waistbands.
Focus: Multi-Sport Durability & REACH Standards
British boarding schools and European multisport academies prioritize heavy-duty, multi-sport utility kits. Rugby shirts demand heavyweight 280-300 GSM interlock fabric with reinforced twin-needle collars to withstand extreme tackle friction. All materials must strictly comply with EU REACH Annex XVII regarding AZO dyes and heavy metals.
Focus: Solar Radiation Protection (UPF 50+)
Oceania educational institutions enforce stringent sun-safety policies. School uniforms for cricket, netball, and athletics require certified UPF 50+ UV protection rating. Base fabrics must incorporate micro-mesh air channels to prevent overheating in humid, high-solar environments.
GoldenLeaf Sports invests directly into research and development across polymer composition, digital sublimation machinery, and automated manufacturing systems. Below is our technical operational roadmap.
Implementation of 100% recycled PET (rPET) derived post-consumer polyester matrix. Using high-pressure thermal gas-phase dye dispersion at 200°C (392°F), liquid dye sublimation molecules permanently anchor into the amorphous regions of the synthetic fibers, eliminating chemical effluent water waste completely.
Integrating 3D body scanning data from over 5,000 student-athletes globally into CAD grading tools. Our automated grading algorithms adapt chest-to-waist ratios dynamically, guaranteeing unrestricted range-of-motion for youth, junior, and senior varsity athletic body types.
Deposition of non-leaching Silver-Ion (Ag+) nano-coatings onto inner core yarns, achieving 99.9% bacterial growth reduction (AATCC 100 test protocol) to eradicate post-training odors. Capillary action micro-grooves draw moisture away from the epidermis to the outer garment surface for sub-10-minute dry rates.
Why do overseas brands, educational procurement desks, and club suppliers partner directly with our Shenzhen factory? The answer lies in the concentrated industrial cluster of the Pearl River Delta.
Within a 50km radius of our Shenzhen campus, we access world-class knitting mills, dye synthesis facilities, and trimming manufacturers. Raw material leads that take weeks in other nations occur within 24–48 hours in our local ecosystem, allowing immediate response to rush academic tournament schedules.
Every uniform lot undergoes strict QA/QC testing prior to carton closure: Tensile Seam Load Testing (ISO 13935-2), Color Fastness to Rubbing/Crocking (Grade 4.5+ via ISO 105-X12), Dimensional Variation Control (<0.5cm variance), Trim Security Check, and Individual Polybag Barcode Matching.
For educational procurement leads, sportswear brands, and tenders, physical garment quality is only half the contract. Secure packaging, exact labeling, and hassle-free door-to-door logistics define full compliance.
We provide complete private label packaging services: custom woven neck tags, heat-applied care labels, branded hangtags with barcodes, individual player-named polybags, and custom master carton marks.
Eliminate customs headaches. We support EXW, FOB Yantian, CIF, and DDP (Delivered Duty Paid) via air or sea freight directly to school campus warehouses across North America, Europe, Australia, and the Middle East.
All fabrics and inks are independently tested and certified under OEKO-TEX Standard 100 Annex 4 (Class I for direct contact with adolescent skin), CPSIA Section 101/108, and EU REACH regulations.
Expert, factory-level clarity on technical specifications, minimal order economics, and production engineering.
Our baseline MOQ for custom sublimated team uniforms is 10 pieces per design block. Because we utilize computerized digital sublimation printing prior to panel cutting, each garment within that 10-piece run can feature unique player names, numbers, and individual body sizes at zero additional setup charge.
We work with standardized Pantone Matching System (PMS) color codes mapped through customized RIP software profiles. Before bulk printing, our color technicians perform physical strike-offs on actual target fabric substrates. We guarantee a Delta E color variance of < 1.0 under standard D65 viewing conditions.
Digital 3D CAD mock-ups are delivered within 24–48 hours. Physical pre-production samples require 5–7 working days. Once the physical sample or digital swatch is approved, bulk production of 300 to 1,000 units is completed in 12–18 working days inside our 3,000 m² Shenzhen facility.
Screen printing lays heavy ink layers over fabric pores, choking breathability and cracking over time. Vinyl heat transfers peel off under commercial high-heat drying. Dye sublimation converts dye directly into gas, permanently fusing it inside the polyester fiber core. The fabric retains 100% of its native breathability, softness, and stretch with zero color fading.
Yes. Our pattern library contains fully graded sizing specs spanning Youth 4Y to 14Y, Women's XS to 4XL (including tailored athletic busts and modified inseams), and Men's/Unisex XS to 6XL. We also build custom length modifications (+2 inches body/sleeve) for specialized varsity sports like basketball.
Explore our secondary lineup including lightweight shorts, custom gym tracksuits, compression tops, and digital print outerwear engineered for total school program alignment.