GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Wholesale Customized Team Baseball Shirt Sublimation V-Neck Jersey Manufacturer, Companies
View Product Details
China Quick Dry Fit Coolmax Promotional Custom Polyester Marathon Sport Running Dye Sublimation T Shirt
View Product Details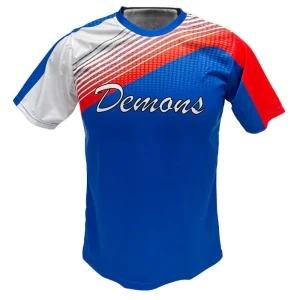
High-Quality Custom Private Label Gym Wear - Tailored Activewear Solutions Supplier, Exporters
View Product Details
Wholesale Custom New Sublimation Polyester Elastic WaitBand Shorts Supplier, Factory
View Product DetailsThe international cricket athletic kit ecosystem is experiencing a structural technological transition. Historically reliant on traditional heavy cotton weaves and cut-and-sew polyester panels with screen-printed graphics, the global market for professional teamwear has overwhelmingly shifted toward custom digital dye-sublimation unisex cricket uniforms. Driven by the global expansion of T20 leagues, franchise tournaments (such as the IPL, Big Bash League, Major League Cricket US, and the Hundred), and grassroots club infrastructure, cricket apparel has evolved from simple sporting whites into high-performance, brand-critical technical wear.
Modern procurement officers, club directors, and sportswear brands require apparel that yields uncompromising durability, complex full-bleed vector graphics, multi-sponsor logo placements, and precision moisture management. Dye-sublimation technology chemically bonds micro-pigments directly into the synthetic polymer matrix under high temperatures (190°C–210°C), resulting in zero added weight, perpetual color fastness, and unobstructed fabric breathability. Furthermore, the industry-wide mandate for unisex ergonomic patterning addresses the operational need for standardized, scalable inventory that comfortably fits both male and female athletes across junior, collegiate, and professional tiers.
Achieving peak performance in custom cricket uniform manufacturing requires a rigorous understanding of textile physics, surface tension, and sublimation ink behavior. Unlike static field sports, cricket exposes garments to diverse physical stressors—ranging from explosive movements while bowling to prolonged sun exposure, friction against protective padding, and heavy perspiration during day-long matches.
Utilizing specialized 140 GSM to 180 GSM 100% micro-polyester and CoolMax bird-eye knits. The engineered capillary network wicks liquid sweat off the skin onto the fabric exterior, accelerating evaporative cooling by up to 35% compared to standard interlock knits.
Industrial manufacturers utilize eco-friendly, non-toxic Italian J-Teck and Kian ink systems. Under high heat transformation, dye molecules permeate deep into the synthetic fiber, ensuring the print never cracks, fades, peels, or blocks micro-ventilation pores.
Engineered using 3D digital CAD pattern grading. Features multi-panel raglan sleeves, modified athletic drop-tails, dynamic gussets, and stretchable waistband constructions that provide unrestricted range-of-motion for both male and female body structures.
| Performance Metric | Technical Benchmark / Standard | Operational Benefit |
|---|---|---|
| Fabric Weight (GSM) | 145 GSM – 160 GSM (Jerseys), 200 GSM – 240 GSM (Trousers) | Optimal balance of lightness, durability, and opacity under white/light colors. |
| Moisture Absorption Rate | < 1.5 seconds (AATCC 79 standard testing) | Instant perspiration pull prevents fabric cling during high-intensity play. |
| Color Fastness Rating | Grade 4-5 (ISO 105-B02 Light Fastness & Wash Testing) | Resists severe UV degradation and fading after 50+ industrial wash cycles. |
| Tensile & Bursting Strength | > 750 N (ISO 13938-1 pneumatic method) | Prevents tearing during athletic sliding, diving, and equipment friction. |
| UV Protection Factor (UPF) | UPF 50+ Certified Treatment | Blocks over 98% of harmful solar UVA/UVB rays during full-day matches. |
When global sports brands, regional distributors, and cricket leagues search for custom sublimation cricket uniform suppliers, China—specifically the Shenzhen apparel manufacturing cluster—stands out as the benchmark for scale, speed, precision, and cost efficiency. As demonstrated by enterprise leaders like GoldenLeaf Sports (ShenZhen) Co., Ltd. (est. 2011), China's integrated vertical supply chain delivers end-to-end solutions that decentralized overseas production facilities cannot match.
From raw yarn spinning and knitting to digital RIP color management, laser pattern cutting, flatlock seam assembly, and final QC inspection—everything operates under a single 3,000 m² footprint. This eliminates multi-vendor friction and reduces production lead times to just 12–18 working days.
Automated visual-registration optical laser cutters read sublimation alignment marks directly off the printed fabric roll. This guarantees 100% pattern consistency, perfect geometric alignment across seams, and clean, heat-sealed edges that prevent fraying.
Because digital printing requires no physical screen setup or plate changes, Chinese OEM factories can economically support MOQs as low as 10 pieces per design. Squads can order fully customized uniforms with unique player names, numbers, and sizes without paying setup surcharges.
Experienced quality assurance teams (over 80% senior apparel technicians) perform 100% inline measurement audits, seam tension tests, color calibration checks, and trim verification before dispatching poly-bagged shipments globally.
Demands for customized cricket uniforms vary significantly depending on geography, climate conditions, league formats, and target demographics. Expert manufacturers must adapt fabric weights, patterns, and features to fit specific market requirements.
Key Requirement: Dual-use Traditional Whites + Vibrant T20 Kits.
Match play in wet, cool, or variable European climates requires slightly heavier 160-180 GSM moisture-wicking interlock fabrics that retain thermal comfort while offering high soil-release properties during wet outfield sliding.
Key Requirement: Maximum UV Block & Extreme Heat Management.
Under harsh Southern Hemisphere sun conditions, uniforms must feature certified UPF 50+ solar protection, open-mesh ventilated side panels, and moisture-transporting polymer formulas to protect long-form and short-form players alike.
Key Requirement: High-Impact Design & Rapid Turnaround.
With the rapid rise of Major League Cricket (MLC), minor leagues, and university clubs, American buyers demand bold, neon-accented, multi-sponsor sublimated kits delivered fast for seasonal tournaments.
For commercial buyers, brand managers, and procurement leads, selecting the right custom cricket uniform manufacturer requires looking beyond unit pricing. To ensure product performance and protect your brand's reputation, evaluate your offshore OEM partner against these technical standards:
Verify that base fabrics carry OEKO-TEX Standard 100 certifications, guaranteeing freedom from harmfulazo dyes, heavy metals, and formaldehyde. Confirm that sublimation inks meet global REACH and CPSIA safety standards.
Ensure the manufacturer utilizes professional Ergosoft or Wasatch RIP software mapped to Pantone Matching System (PMS) color charts. This eliminates color variance between re-orders and ensures exact brand-sponsor color replication.
Confirm full ODM capabilities: woven inner neck tags, heat-transfer size labels, customized hangtags, barcode polybagging, and custom master carton marking for seamless integration into direct-to-consumer (D2C) fulfillment centers.
Cricket trousers and jerseys require reinforced flatlock 4-needle 6-thread or double-needle cover-stitching across high-stress zones (crotch gussets, armholes, and collars) to prevent seam failure during competitive matches.
The custom sublimation teamwear industry is evolving rapidly. Forward-thinking manufacturers are integrating sustainable materials and digital production tools to meet the next generation of athletic demands.
Transitioning from virgin polyester to 100% post-consumer recycled poly (derived from recycled PET plastic bottles). Recycled polyesters deliver identical tensile strength and sublimation print clarity while reducing carbon footprints by up to 45%.
Replacing static 2D flat proofs with interactive 3D virtual rendering engines. B2B buyers can inspect realistic digital drape, seam placement, and sponsor scaling on dynamic athletic models before approving physical pre-production samples.
Adopting waterless digital transfer processes. Unlike traditional wet dyeing, dry-sublimation produces zero toxic liquid runoff, fully aligning with global ESG compliance standards for international sports brands.
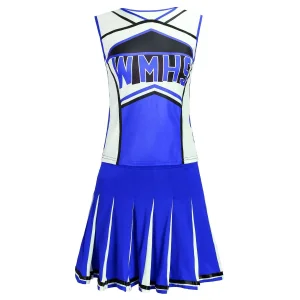
Wholesale High Quality Cheerleading Dresses Custom Cheerleading Uniforms for Women’s Exporters
View Product Details
OEM Custom sublimation Rugby Jeresy with 4 way streching making Manufacturer, Companies
View Product Details