GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our export-grade sublimated athletic apparel, built for global clubs, distributors, and brands.
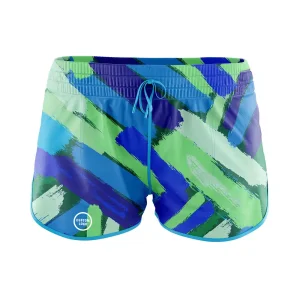
Analyzing the shift from traditional screen-printed activewear to engineered digital dye-sublimation solutions in international B2B markets.
The international market for professional athletic apparel has undergone a structural paradigm shift over the past decade. Within the niche of high-performance court sports, custom sublimation volleyball shorts have transitioned from a luxury team wear item to an absolute industry standard for professional leagues, collegiate athletic departments, and commercial sportswear brands. Unlike traditional cut-and-sew methods or vinyl heat-transfer applications, dye-sublimation technology embeds color pigments directly into the synthetic polymer matrix of the fabric. This creates an unyielding fusion of high-definition visual customization and uncompromising mechanical performance.
From an enterprise procurement perspective, the global market demand is driven by three critical factors: high-frequency friction resistance, demand for complex localized branding (sponsor logos, player rosters, club emblems), and the mandatory requirement for micro-climate heat dissipation during explosive athletic maneuvers. Global sports apparel exporters and OEM factories are increasingly tasked with providing seamless, end-to-end manufacturing solutions capable of maintaining rapid design iteration cycles while fulfilling strict environmental compliance benchmarks such as OEKO-TEX® Standard 100 and ISO 9001 quality management standards.
Modern sports equipment buyers—ranging from regional importers in North America and Western Europe to institutional distributors in Australia and South America—are phasing out legacy inventory models in favor of agile OEM/ODM manufacturing. Custom dye-sublimation eliminates the financial friction of maintaining post-production decorating setups. By transferring graphics, numbering, and color-blocking simultaneously during panel-stage pressing, factory unit costs drop significantly at scale while eliminating decorative cracking, peeling, or weight addition.
Deep-dive analysis into textile formulation, sublimation physics, color-matching RIP software, and automated precision cutting.
The structural integrity of custom volleyball shorts relies heavily on the substrate composition. Sublimation chemistry requires synthetic fibers—primarily Polyethylene Terephthalate (PET) or blended Poly-Spandex matrices—where heat opens the polymer structure, allowing disperse dyes to transition from solid to gaseous phases and bind inside the filament cross-section at temperatures reaching 190°C to 215°C.
Engineered with an 88/12 or 85/15 Polyester to Elastane balance. Delivers 4-way stretch capabilities necessary for explosive diving, blocking, and rapid lateral accelerations without yarn distortion.
Hydrophobic filament profiles push perspiration away from the skin surface to the outer garment surface via capillary channels, facilitating rapid evaporation during high-intensity indoor rallies.
Interlock fabric structures rated at 180 to 240 GSM prevent floor burn, fiber pilling, and mechanical tearing during repeated court slides, meeting ISO 12945-2 pilling standards.
Customized garment construction tailored to male, female, indoor court, and beach volleyball performance requirements.
Volleyball demands distinct movement dynamics compared to traditional field sports. Athletes experience high frequency jumping, lateral shuffling, and ground contact. Consequently, specialized exporters and ODM manufacturers adjust block patterns depending on gender, division, and surface environments.
| Application Profile | Inseam Standard | Fabric Weight (GSM) | Structural Features | Primary Market Segment |
|---|---|---|---|---|
| Women's Indoor Pro Shorts | 2" to 4" Compression | 220 - 260 GSM (Poly-Spandex) | Wide non-roll waistband, seamless crotch gusset, anti-ride leg hem. | NCAA, CEV, Professional Leagues |
| Men's Indoor Match Shorts | 5" to 7" Loose / Fitted Cut | 160 - 190 GSM (Micro-Interlock) | Reinforced drawcord channel, side slit vents, multi-panel flex zone. | FIVB, High School & Collegiate Clubs |
| Beach Volleyball Performance | 3" Fitted / Low Inseam | 200 - 240 GSM (UPF 50+ Poly) | UV-protective finish, sand-resistant weave, quick-dry hydrophobic coat. | AVP Tour, Global Beach Volleyball Series |
| Youth & Academy Training | 4" to 6" Unisex Cut | 150 - 180 GSM (Bird-Eye Mesh) | Elastic waistband, double-stitched stress zones, stain-release treatment. | Regional Youth Academies & Schools |
A critical vulnerability in mass-produced sports shorts is seam failure along the crotch apex during deep squatting defensive postures. Tier-1 sublimation factories integrate an anatomical teardrop or diamond gusset. This panel redistributes tension away from primary seam intersections, increasing garment lifespan while maintaining complete movement freedom for the athlete.
How established Chinese exporting facilities streamline B2B manufacturing, private labeling, and direct global fulfillment.
Clients submit AI/PDF vector templates. Factory design technicians generate 3D digital renderings within 24 hours to confirm Pantone scaling, panel positioning, and sponsor placement.
Pre-production physical samples are output in 3 to 5 business days. Color swatches are transferred directly to chosen bulk fabrics to ensure exact visual matching prior to mass cutting.
Integrated production lines process bulk orders over 12 to 18 working days. Inline QA inspectors check tensile seam strength, dimension scaling against size charts, and print consistency under AQL 2.5 standards.
In response to international regulatory shifts and consumer expectations, leading sublimated sports shorts exporters have integrated Recycled Polyethylene Terephthalate (rPET) options. Derived from post-consumer recycled plastic bottles, rPET maintains identical tensile strength, dye receptor affinity, and moisture-wicking properties while reducing carbon footprint metrics by up to 45%. Furthermore, custom packaging solutions—including eco-friendly polybags, woven brand labels, silicone size tags, and barcoded hangtags—are fully managed at the factory floor for ready-to-shelf delivery.
Direct technical guidance from factory production supervisors addressing critical B2B buyer questions.
Explore our extended line of performance sportswear engineered for global team supply chains.