GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
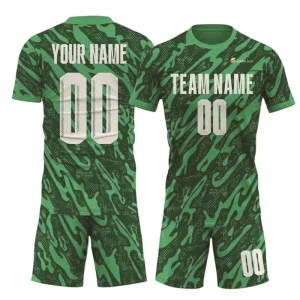
Explore our high-performance custom teamwear manufactured with precision digital sublimation, engineered to withstand high-impact competitive environments.
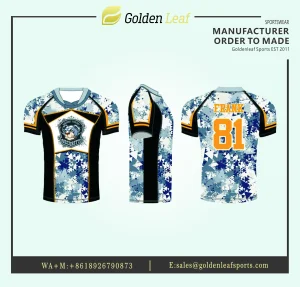
Rugby Union and Rugby League represent two of the most physically demanding team sports in existence. Consequently, sourcing custom team rugby uniform wholesale suppliers & exporters requires a transition from standardized apparel sourcing to advanced textile engineering. Unlike conventional sports apparel (such as soccer or basketball uniforms), rugby team kits undergo intense kinetic strain, extreme friction, grab-and-tackle forces, and continuous atmospheric exposure. Institutional B2B buyers—ranging from regional sports brand distributors to national league suppliers—demand apparel that balances high tensile strength with dynamic thermal management.
As a primary China-based custom sportswear manufacturer operating out of Shenzhen since 2011, GoldenLeaf Sports operates a specialized 3,000 m² vertical production enterprise. We deploy specialized digital dye-sublimation machinery, reinforced flatlock stitching systems, and rigorous QA protocol matrices to deliver export-grade rugby match kits, training wear, and fan apparel across North America, Europe, Australia, and the Pacific Rim.
The global rugby apparel market is undergoing a structural shift driven by fabric innovations, digital supply chain acceleration, and sustainable textile regulations.
Traditional heavy cotton rugby jerseys (350+ GSM) have been completely phased out of competitive play. Modern elite teams use high-tensile 280–320 GSM polyester-elastane blends. These technical knits feature 4-way elastic memory, preventing tackles from gaining momentum while giving athletes full freedom of movement.
Professional, university, and academy rugby uniforms now require internal GPS tracking pouch integration located behind the upper back panel. Manufacturers must engineer seamless internal neoprene pockets that house movement telemetry hardware without irritating the player's upper spine.
Global buyers, especially across the UK, EU, and Australasia, require compliance with environmental standards. Modern sublimated teamwear leverages rPET (recycled Polyethylene Terephthalate) derived from post-consumer plastic bottles, meeting GRS (Global Recycled Standard) benchmarks without sacrificing burst strength.
Understanding geographic specifications allows exporter networks to deliver tailored manufacturing solutions.
| Target Region | Primary Buyers | Key Fabric & Pattern Specs | Compliance & Logistics Focus |
|---|---|---|---|
| Oceania (AU / NZ / Pacific) | State Leagues, School First XV, Club Retailers | 280-300 GSM Poly Spandex, Silicone Grip Prints, GPS Pockets, Aboriginal Artwork Sublimation | Fast Air-Freight Turnarounds, OEM Private Labeling, Tariff Optimization (ChAFTA / RCEP) |
| Europe (UK / FR / IE / IT) | Professional Academies, University Sports Unions, Retail Brands | Reversible Match Kits, Weather-Resistant Thermal Outerwear, Eco-Poly Interlock | OEKO-TEX Standard 100 Class I, REACH Chemical Compliance, ISO 9001 Audit Trail |
| North America (US / CA) | Major League Rugby (MLR) Affiliates, High School Associations | Athletic Form-Fit Blocks, Heavy-Duty Reinforced Collar Loops, Moisture-Wicking Mesh Shorts | Custom Sizing Charts (US Sizes 2XS to 5XL), Low MOQ Batch Replenishment, DDP Logistics |
| Emerging (Japan / South Africa) | Corporate Teams, Multi-Sport Training Centers | Lightweight 220 GSM Sevens Rugby Kits, Ultra-Flexible Flatlock Stitching | Pantone Precision Color Accuracy (Delta E < 1.0), Customized Individual Polybag Packing |
How GoldenLeaf Sports engineers high-end custom rugby uniforms built for elite performance.
Rugby jerseys experience immense pulling forces during scrums and rucks. Standard athletic knits tear under 250 Newtons of force. We utilize dynamic warp-knit interlock fabrics rated to withstand pull forces exceeding 450 Newtons. Reinforced cross-tack stitching at stress points (armpits, neckplackets, side seams) eliminates mechanical failure during competition.
Surface-level sublimation can result in visible white fabric show-through when the garment stretches. We utilize high-pressure, deep-penetration heat presses calibrated at 210°C for 30 seconds, using imported Eco-friendly inks. This guarantees that deep pantone hues penetrate up to 80% of the fiber matrix, preventing color fading or stretch whitening.
Traditional thick fold-down collars are easily grabbed by opposing players. We engineer low-profile technical collars including Grandad Collars, Split-V Collars, and GPS Loop Collars. Every seam is constructed using 6-needle 4-thread flatlock machines, creating smooth, chafe-free interior lines against the player's skin.
We provide end-to-end ODM and OEM private label services. Brand owners can specify custom woven neck tags, heat-transfer inner size labels, anti-counterfeit holographic hanging tags, and branded polybag packaging. Our graphic team prepares 3D virtual renderings within 24 to 48 hours for immediate buyer sign-off.
Quality control is fully integrated into our production floor. Five specialized QA inspectors inspect raw fabric density, sub-print registration, seam strength, dimensional tolerance (<1cm deviation), and garment cleanliness. Shipments adhere strictly to ISO-compliant Acceptable Quality Limit (AQL) 2.5 standards.
To reduce inventory risk for sports apparel distributors, our core sublimated teamwear starts at just 10 pieces per design. Because we print directly onto un-cut panels, individual player names, numbers, and custom sizes can be included in a single batch without extra setup costs.
Looking toward 2030, rugby apparel manufacturing will converge with advanced automation and smart textile technology. Key innovations currently entering our R&D roadmap include:
Explore our full lineup of custom sublimated teamwear, performance activewear, and club accessories.