



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our top-tier OEM & ODM sublimated athletic apparel line engineered for global distributors, professional clubs, and regional sports programs.
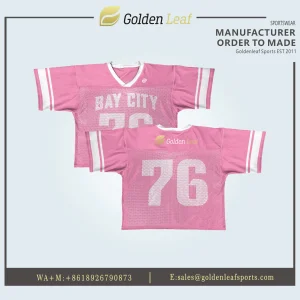
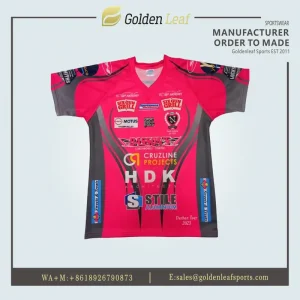
Understanding the macro-economic forces, shift toward digital dye-sublimation, and procurement requirements for institutional buyers worldwide.
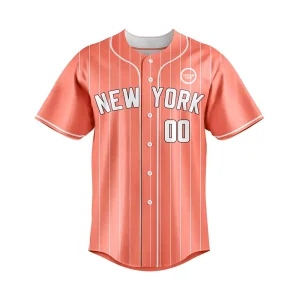
Traditional screen-printed baseball uniforms are rapidly being phased out by professional leagues, NCAA divisions, and youth academies. Modern athletic organizations require full digital dye-sublimation that integrates player names, numbers, gradient patterns, and sponsor vector logos directly into the synthetic fabric matrix without adding structural weight or compromising breathability.
Baseball uniforms experience harsh mechanical stress, sliding abrasion, and intense UV exposure. Global brand buyers demand high-tensile 180 to 220 GSM interlock polyesters equipped with elastane blends, anti-microbial treatments, and UPF 50+ ultraviolet radiation defense. Factory-level stitching must utilize reinforced double-needle cover-stitching to ensure zero seam blowout during gameplay.
The rise of micro-tier sports leagues and corporate team building has forced wholesalers to pivot away from massive minimum order quantities (MOQs). Leading Chinese manufacturing facilities now leverage automated CAD pattern-grading and high-speed digital printers to fulfill custom orders from as few as 10 units up to 100,000 units while maintaining flat unit costs.
Deep dive into polymer composition, fabric weight options, thread counts, and printing technologies utilized in high-grade OEM baseball shirt manufacturing.
| Fabric Type | GSM Weight | Composition | Performance Traits | Recommended Usage |
|---|---|---|---|---|
| Pro-Grid Bird-Eye Mesh | 160 - 180 GSM | 100% Micro-Polyester | Maximum ventilation, quick-dry capillary structure, anti-snag. | Sublimated practice jerseys, hot-climate tournament wear. |
| Heavyweight Performance Interlock | 190 - 220 GSM | 100% High-Tenacity Poly | Superior tensile strength, high opacity, soft-hand texture. | Official league match jerseys, full-button custom team shirts. |
| Flex-Tech Spandex Blend | 200 - 240 GSM | 88% Polyester / 12% Elastane | 4-way elastic stretch, ergonomic form-fit, zero drag resistance. | Pro-fit athletic baselayers, elite competition baseball shirts. |
| Classic Tackled Twill Hybrid | 210 GSM Base | Poly-Twill + Sublimated Trim | Vintage aesthetic combined with digital lightweight side panels. | Heritage team uniforms, championship commemorative apparel. |
Unlike conventional screen printing or vinyl heat-transfers which deposit a physical layer of PVC or ink film over the fabric—blocking pore ventilation and peeling after repeated washings—our industrial dye-sublimation process operates at 215°C (419°F). Under precise thermal pressure, disperse solid dyes convert directly into gas, vaporizing deep into the core of the polyester micro-filaments. The solid polymer matrix locks the pigments permanently inside the fiber, guaranteeing 100% colorfastness (Grade 4.5+ standard test compliant) and preserving complete breathability across all custom panels.
Why leading global apparel brands, teamwear dealers, and e-commerce companies partner with our 3,000 m² Shenzhen manufacturing complex.
Leveraging automated vector mapping software and direct-to-fabric continuous printing lines, our design desk delivers complete 3D digital proof mock-ups within 24 hours. Physical sample garments are cut, sublimated, sewn, and quality-inspected within 5 to 7 working days, cutting traditional lead times by over 60%.
Situated in Longgang District, Shenzhen, our facility sits at the center of the world's dense textile, dyeing, zipper, and packaging ecosystem. Raw polyester yarn, Swiss Kian inks, high-tensile threads, and custom woven tags are sourced locally within a 15-minute supply radius, drastically lowering procurement friction and raw material waste.
Every bulk order undergoes rigorous internal QC standard procedures: 1) Raw fabric grammage and elasticity inspection; 2) RIP color spectrum calibration; 3) Laser pattern alignment check; 4) Tension and seam stress testing; and 5) Final individual packing measurement verification by our 5 dedicated QA inspectors.
Tailored design blocks, sizing scales, and aesthetic conventions optimized for specific regional sports markets.
For US & Canadian buyers (USSSA, Little League, NCAA, Senior Softball), garments feature relaxed, athletic cuts with room for protective under-pads. Designs emphasize full-button v-neck fronts, traditional raglan sleeves, multi-color braid trims, and tackle-twill feel sublimation for high-school and collegiate team compliance.
Serving professional winter leagues and elite youth development academies across the Dominican Republic, Venezuela, and Puerto Rico. Focus is placed on ultra-lightweight 150-160 GSM open mesh construction to dissipate extreme heat and humidity, featuring vibrant neon gradients and reinforced knee/shoulder impact zones.
Catering to NPB/KBO amateur divisions in Japan/Korea and WBSC European federations. Pattern blocks utilize modern slim-fit Asian & European slim-grading, 2-button henley collar profiles, integrated stretch side-mesh panels, and private-label woven neck tags tailored for local boutique sports retailers.
Optimizing unit margins, duty tariffs, shipping logistics, and OEM private-label integration for maximum profitability.
By eliminating overseas brokers, trading intermediaries, and regional sales agents, purchasing buyers deal directly with our Shenzhen manufacturing floor. This reduces landed product costs by 30% to 50%, enabling higher distributor markups and competitive retail pricing.
Elevate your private apparel label with comprehensive OEM custom detailing: customized neck heat-seal transfers, high-density woven brand labels, custom hangtags with barcoding, anti-counterfeiting holographic stickers, and custom printed eco-polybags per jersey set.
We provide full-service logistics compliance across EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid) terms. Whether utilizing express air courier for rapid 4-day delivery or ocean container shipping for bulk seasonal orders, custom duties and taxes are managed smoothly.
How ecological policies and smart automation are redefining custom wholesale baseball jersey production.
To align with global ESG guidelines and corporate sustainability targets, our factory offers 100% Recycled Polyethylene Terephthalate (rPET) fabrics made from post-consumer plastic bottles. These recycled fibers deliver identical tensile strength, moisture-wicking rates, and dye absorption as virgin synthetic yarns while reducing carbon footprint by 45%.
Traditional wet dyeing techniques consume over 100 liters of water per kilogram of fabric. Thermal transfer sublimation is an eco-friendly dry printing process that uses zero liquid water during color application, eliminating toxic chemical wastewater discharge and complying with strict international OEKO-TEX Standard 100 certification.
Our Shenzhen cutting room utilizes artificial intelligence nesting algorithms that automatically optimize panel placement on paper rolls before thermal transfer. This reduces fabric scrap waste to under 2.5%. Subsequent automated laser cutting lines deliver millimeter-precise panel alignment matching exact digital sizing charts.
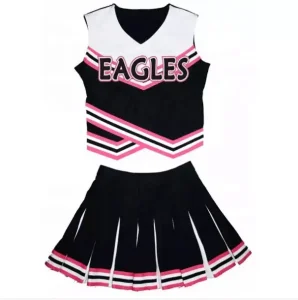
Browse additional customized sports uniforms, training gear, and performance apparel manufactured directly by GoldenLeaf Sports.
Direct answers addressing intent, factory compliance, production logistics, and customization options for commercial buyers.