GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our core technological platforms engineered for maximum durability, heat dissipation, and customizable squad identity.
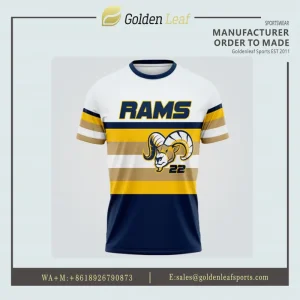
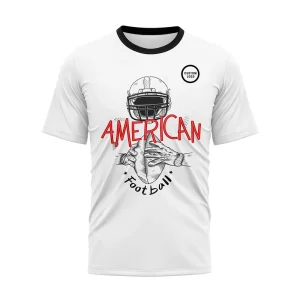
The global sports apparel ecosystem is experiencing an unprecedented structural transformation. Driven by advancements in polymer textile engineering, digital color management, and real-time agile manufacturing, high-quality American football jerseys are no longer mere branding vehicles—they are critical athletic hardware engineered to optimize player ergonomics, thermal regulation, and structural elasticity.
Modern gridiron football demands equipment capable of enduring extreme mechanical force while retaining tactical comfort. Professional sports leagues, NCAA collegiate programs, regional high schools, and commercial apparel distributors are rapidly recalibrating their sourcing strategies. Procurement departments are migrating away from traditional heavy cotton-poly blends toward multi-paneled, hyper-breathable, full-sublimation polyester matrixes engineered specifically for impact resistance and friction mitigation.
Furthermore, consumer purchasing behavior across sports fan merchandising has shifted. Retail brands require authentic, stadium-grade replica jerseys manufactured under strict quality compliance frameworks (ISO9001, OEKO-TEX Standard 100). Consequently, tier-1 global buyers seek OEM/ODM manufacturing partners equipped with digital vertical integration, flexible minimum order quantities (MOQs), and transparent supply chain logistics.
High-performance American football jerseys require sophisticated material composition to withstand high-velocity collisions, jersey-pulling tackles, and ambient heat build-up. Premium manufacturers utilize specific technical textiles mapped to distinct body heat zones and structural stress points.
Utilizing 100% high-grade polyester interlock with bird-eye micro-perforations (145–180 GSM), this fabric draws perspiration away from the athlete’s epidermis via capillary action, expediting evaporative cooling during intensive play cycles.
Constructed from 4-way stretch poly-spandex blends (88/12 ratio, 250+ GSM), providing high elasticity around shoulder pads to lock gear into place while prohibiting opposing defenders from establishing leverage holds.
Engineered for front and back torso panels, featuring high-density shiny weave structures that offer exceptional tear resistance under severe mechanical stress, coupled with fade-resistant color-holding capacities.
The following technical matrix outlines the material specifications utilized by modern high-end football uniform factories to meet international athletic standards:
| Garment Zone | Primary Material | Weight (GSM) | Key Performance Attribute | Stitching Protocol |
|---|---|---|---|---|
| Chest & Back Panels | Dazzle / Heavy Polyester Interlock | 180 - 220 GSM | Abrasion Resistance & Number Stability | Double-Needle Flatlock Stitching |
| Shoulders & Sleeves | 4-Way Poly-Spandex Blend | 240 - 280 GSM | High Elasticity over Shoulder Pads | Reinforced Bar-Tack Strain Points |
| Side Venting Panels | Bird-Eye Micro Mesh | 145 - 160 GSM | Maximum Airflow & Thermal Release | Four-Needle Six-Thread Seams |
| Collar & V-Neck Inserts | Ribbed Elasticized Knit / TPU | 260 - 300 GSM | Shape Retention & Snug Fit | Heavy-Duty Anchor Threading |
As global sports brands face volatile market demands and shortened product development lifecycles, China’s advanced apparel manufacturing ecosystem—centered in high-tech industrial hubs like Shenzhen—delivers unmatched competitive advantages through digital automation and industrial integration.
Industrial-scale digital printers powered by high-resolution Raster Image Processor (RIP) software utilize eco-friendly imported sublimation inks. This guarantees color fastness (Grade 4.5+ standard) that prevents color bleeding, fading, or peeling even after 100+ commercial wash cycles.
Automated optical camera laser-cutting systems scan registration marks directly on printed fabrics, executing clean panel separation with ultra-narrow tolerances. This eliminates frayed edges and guarantees pristine vector design alignment across complex sleeve-to-chest transitions.
From yarn testing and greige cloth inspection to thermal press sublimation, line assembly, and final stitch integrity verification, dedicated QA teams inspect 100% of finished orders, eliminating defects prior to export packaging.
Operating inside Shenzhen’s mature textile hub enables immediate access to specialized raw materials, custom elastic trims, high-grade tackle twill patches, and hardware within a 50-kilometer radius. This geographic concentration reduces component lead times from weeks to hours, giving international clients rapid turnarounds on both low-MOQ custom runs and mass production batches.
Sourcing requirements for custom American football gear vary significantly depending on regional league rules, business models, and end-user demography. Specialized custom apparel factories design customizable workflows to cater specifically to these distinct commercial vectors.
Key Priority: Extreme Durability & Precise Player Fitting.
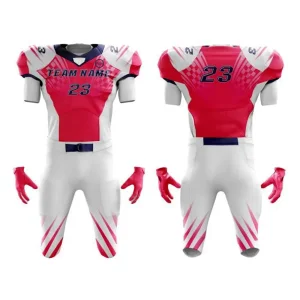
Professional athletic clubs demand custom anatomical cuts (Cowl neck, elasticized sleeve cuffs, silicone waistband grippers) that integrate seamlessly with pad systems. Sublimated player names and numbers must meet strict optical clarity guidelines for broadcast and stadium tracking visibility.
Key Priority: Cost Efficiency, Scale & Fast Re-Order Processing.
School athletic departments demand durable, multi-season uniforms capable of undergoing repeated industrial laundering. OEM manufacturers support school colors with standardized Pantone color matching systems to ensure uniform consistency year-over-year when replacing individual player kits.
Key Priority: Vibrant Aesthetics, Lightness & Speed.
Non-tackle and non-padded variations emphasize lighter fabrics (145-160 GSM full sublimation mesh) with bright, trendy graphic designs, full-custom sponsor logos, and flexible sizing ranges spanning 6Y to 5XL.
Key Priority: ODM Branding, Retail Packaging & Compliance.
Independent streetwear lines and official team merchandise retailers require OEM/ODM services including woven neck labels, custom hang tags, individual barcode polybags, and retail-ready folding services.
Direct responses to critical engineering, manufacturing, and supply chain questions from prospective bulk purchasers and teamwear distributors.
Explore our broader line of specialized custom apparel designed, printed, and manufactured within our integrated production facilities.