



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our engineering-grade custom team apparel designed for collegiate programs, athletic departments, and commercial apparel distributors worldwide.
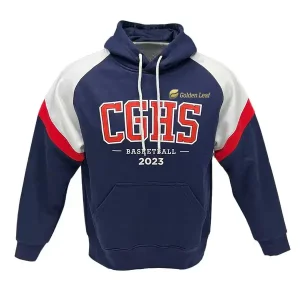
A comprehensive technical report on high-volume OEM/ODM team kit manufacturing, fabric science, regulatory compliance, and international procurement logistics for university athletic departments.
In the modern global sports economy, collegiate athletic apparel procurement has evolved far beyond basic garment assembly. University procurement departments, equipment managers, and sports apparel distributors demand high-tenacity, moisture-wicking, and visually striking uniforms that withstand the rigorous demands of multi-season competition. As a premier High-Quality College Team Uniforms Supplier & Company, GoldenLeaf Sports (ShenZhen) Co., Ltd. combines specialized material science, digital dye-sublimation precision, and direct-factory manufacturing control to deliver elite performance kits across North America, Europe, Australia, and the Asia-Pacific region.
Founded in 2011 within the advanced technological hub of Longgang District, Shenzhen, GoldenLeaf Sports operates an integrated 3,000 m² production infrastructure. Supported by over 160 skilled technicians—80% of whom hold senior apparel engineering credentials—our factory processes everything under one roof: artwork vectorization, RIP color management, digital sublimation printing, precision laser cutting, ergonomic flatlock sewing, and multi-stage QA/QC inspection. This vertical integration allows institutional buyers to achieve unparalleled customization without compromising on structural integrity or delivery schedules.
Addressing the strategic supply chain requirements of University Athletic Associations, NCAA/NAIA programs, and B2B apparel brands.
Collegiate brand guidelines demand exact Pantone hex-code matching across different garments, re-orders, and sports disciplines over multiple athletic seasons.
Mid-season roster changes require rapid-turnaround replacement jerseys with individual player names, numbers, and custom tailored sizing without setup penalties.
Contact sports like rugby, lacrosse, and American football require heavy-duty polyester twill and reinforced twin-needle flatlock seams to resist tearing under stress.
Strict academic and competition calendars require guaranteed manufacturing timeframes and direct air-freight dispatch to arrive prior to season kick-off.
When procurement officers evaluate custom teamwear vendors, the primary focus centers on total cost of ownership (TCO), garment longevity, and operational responsiveness. Off-the-shelf stock uniforms decorated via post-production screen printing or vinyl transfers often fail after repeated commercial laundering. Screen inks crack, heat-applied numbers peel, and stock garments suffer from inventory stockouts when replacement sizes are urgently needed.
GoldenLeaf Sports eliminates these friction points through full digital sublimation technology. By infusing Eco-friendly imported sublimation inks directly into the polymer matrices of synthetic fabrics at high temperatures, the artwork, logos, sponsor panels, player numbers, and names become an indelible part of the cloth. The garment remains fully breathable, light, and flexible, with guaranteed colorfastness (Grade 4 or higher) across 50+ commercial wash cycles.
Leveraging South China's advanced textile ecosystem, automated hardware, and skilled workforce to deliver superior performance sportswear.
High-speed optical laser systems cut printed fabric panels along visual registration marks, guaranteeing sub-millimeter precision across complex athletic patterns.
Direct access to elite raw mills producing 145-180 gsm interlock, 4-way poly-spandex blends (88/12), micro-mesh, and heavyweight tear-resistant rugby twill.
Dedicated quality control inspectors review raw material tension, print color fidelity, stitch density, measurement tolerances, and packaging integrity.
Seamless customs clearance, optimized tariff classification, and multi-modal logistics (DDP, FOB, CIF, Express Courier) to over 50 countries.
The Greater Bay Area of Guangdong, specifically Shenzhen, represents the world’s most concentrated athletic apparel manufacturing hub. This proximity allows GoldenLeaf Sports to source high-grade technical polyesters, specialized spandex trims, custom knit ribbing, and eco-certified inks within hours, drastically reducing lead times compared to inland or overseas apparel factories.
Our facility houses high-precision Japanese digital inkjet printers operating under calibrated ICC color profiles. Combined with continuous-roll heat sublimation presses, we maintain absolute saturation depth and precise edge definition for intricate school crests, mascot graphics, and gradients. Once sublimated, panels move to our automated laser-cutting stations, ensuring every size—from Youth 6Y to Adult 5XL—is cut to exact pattern specifications.
Ensuring compliance with international safety standards, athletic association rules, and environmental regulations.
All fabrics, inks, zippers, and threads undergo rigorous screening to ensure zero toxic substances, heavy metals, or harmful azo dyes touch student-athlete skin.
Fully compliant with North American CPSIA requirements for youth athletic gear and European REACH regulations for environmental chemical security.
Pattern blocks engineered to adhere strictly to collegiate uniform rules: contrast home/away guidelines, number size ratios, and logo placement boundaries.
Complete OEM/ODM customization including woven neck labels, silicone heat-seal branding, polybag barcodes, and custom hang-tag packaging for distributors.
Collegiate institutions operate under strict vendor compliance protocols. GoldenLeaf Sports maintains a comprehensive audit-ready operational standard. Our eco-solvent and water-based sublimation inks pass stringent international chemical safety evaluations, ensuring non-toxicity and zero skin irritation during intense physical exertion.
Furthermore, our engineering team regularly updates pattern libraries to comply with changing athletic association rulebooks—such as NCAA Rule 1 Section 22 regarding uniform contrast ratios and solid-color zone rules in soccer and basketball. We provide pre-production visual proofs detailing dimensioned logo placement, seam allowances, and letter heights to ensure complete compliance before physical production commences.
How digital twins, recycled polymers, and automated production are reshaping collegiate teamwear manufacturing.
Transitioning to 100% recycled polyester yarns spun from post-consumer plastic bottles, reducing carbon footprint while maintaining elite strength.
Utilizing 3D CAD visualization tools to render true-to-scale virtual samples in 24-48 hours, eliminating physical sample iterations and speeding up approvals.
Integrating zoned breathability mesh panels and quick-dry hydrophobic yarn structures to maximize moisture evaporation during elite athletic exertion.
Replacing bulk warehouse inventory models with agile, low-MOQ sub-assembly manufacturing that supports just-in-time team order fulfillment.
The athletic apparel sector is undergoing a massive transformation toward environmental sustainability and digital manufacturing integration. GoldenLeaf Sports is at the forefront of this shift, offering sustainable fabric alternatives constructed from GOTS- and Global Recycled Standard (GRS)-certified recycled polyesters (rPET). These fabrics deliver identical tensile resistance, burst strength, and moisture-wicking indices as virgin polyester while reducing energy consumption by up to 30% during yarn synthesis.
On the design front, our implementation of AI-assisted 2D-to-3D pattern mapping enables athletic directors and brand owners to preview realistic 360-degree digital twins of their custom teamwear line before cutting fabric. This workflow eliminates wasted physical proto-samples, reduces lead times by up to 5 days, and guarantees that sponsor logos, player typography, and seam lines align across every uniform size.
Tailored garment engineering for collegiate programs across diverse regional leagues and sports disciplines.
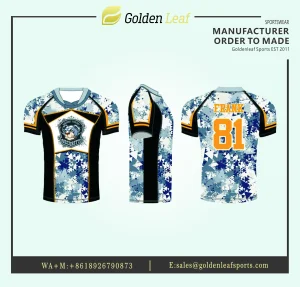
High-impact Lacrosse and American Football kits constructed from heavy-duty 220-280 gsm polyester twill and 4-way stretch mesh inserts. Reinforced armholes, shoulder yoke panels, and stretch waistbands engineered for pad integration.
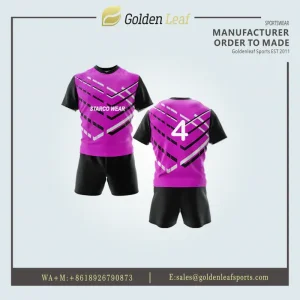
Rugby, Soccer, and Netball uniforms built with moisture-wicking 150-180 gsm interlock fabrics. Features reinforced collar plackets, ergonomic raglan sleeve cuts, and anti-friction flatlock stitching designed for damp field conditions.
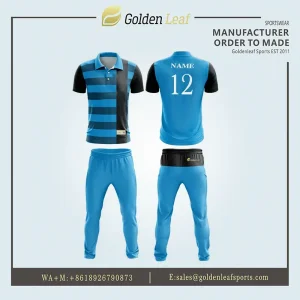
Basketball, Cricket, and Volleyball uniforms optimized for warm-weather ventilation. Open bird-eye mesh fabric bodies combined with lightweight micro-interlock side panels provide max airflow and UPF 30+ UV protection.
Every athletic discipline places unique physical stresses on sportswear. A generic jersey pattern cannot meet the performance criteria of specialized sports. For instance, lacrosse jerseys require cut-outs that accommodate thick protective shoulder pads without restricting arm rotation, while competitive volleyball tops require 4-way spandex stretch to allow unrestricted overhead spiking and diving movements.
Our pattern engineering team has created calibrated pattern libraries tailored specifically for each sport discipline. By analyzing player mechanics, we place high-density breathability zones under the armpits and lower back, while utilizing high-tenacity double-stitched seams along heavy-wear stress points. This meticulous attention to sport-specific ergonomics ensures that every athlete experiences maximum comfort and mobility on game day.
Transparent operational milestones combined with real-world feedback from coaches, team managers, and sports apparel buyers.
Detailed consultation on sport type, quantity, fabric selection, and target lead time with 24h response.
Confirmation of regional size charts (US, EU, AU, Youth) and pattern grading before printing.
In-house graphic artists prepare 2D/3D visual proofs with unlimited vector revisions.
Color-calibrated digital printing onto high-release transfer paper using eco-friendly inks.
High-temperature deep dye transfer bonding ink permanently into white polyester fibers.
Optical laser cutting of sublimated panels ensuring precise edge alignment across all sizes.
Precision flatlock and overlock stitching with options for custom neck tags and labels.
5-point quality inspection, individual polybagging, sorted sorting, and worldwide dispatch.
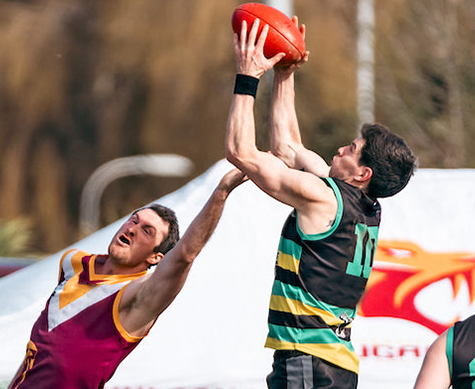
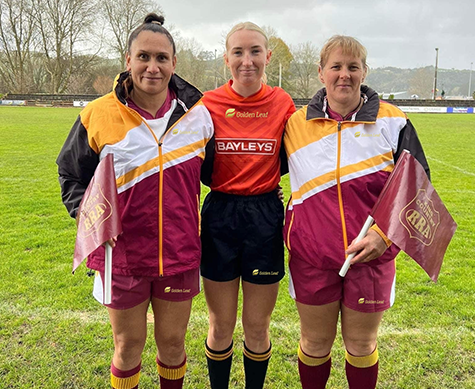
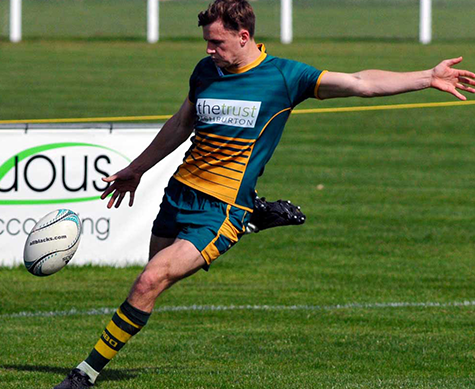
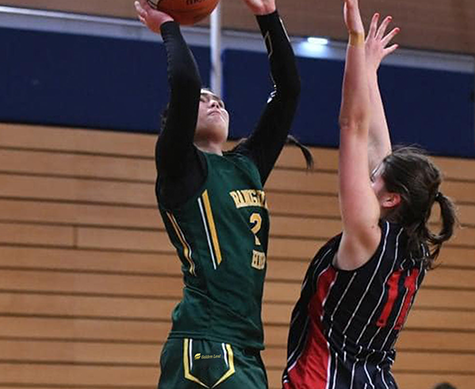
Explore actual production footage from our Shenzhen manufacturing plant demonstrating vector layout, dye-sublimation heat pressing, automated laser panel trimming, and garment assembly lines.
“We ordered these for our youth basketball league. The quality is amazing — washes and wears well. We were able to have both sides printed easily and without issues. We would definitely order these again.”
Austin Wilde — Youth League Director, USA“I bought this for my son and he loved it. It is comfortable and true to sizing — definitely worth what I paid, especially for the quality. The colours are nice.”
Kayla — Junior Soccer Parent, Canada“Material is light and keeps the body fresh while playing. Took a bit to arrive, but absolutely worth it for a fully custom uniform set.”
Alicia — Club Soccer Organiser, USA“Great orange colour and the design came out great. The shirt quality is nice — very cute volleyball shirt for those looking for team jerseys.”
HDC — Volleyball Coordinator, AustraliaDirect technical answers addressing minimum order requirements, turnaround schedules, fabric engineering, and global logistics.
Our standard low-MOQ requirement is 10 pieces per design for full-sublimation jerseys, shorts, and pinnies. Because each piece is digitally printed before laser-cutting, individual player names, numbers, and sizes can be mixed freely within the same 10-piece run at no extra charge. Accessories such as custom knit socks and caps have separate minimum production runs depending on machinery setup.
Initial 2D vector digital proofs are generated within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Full bulk production runs ranging from 300 to 1,000 units are completed in 12 to 18 working days post artwork sign-off. Air express courier delivery (DHL, FedEx, UPS) requires an additional 4 to 7 business days worldwide.
We stock a wide variety of engineered synthetic fabrics: 100% polyester interlock (145-180 gsm) for multi-sport versatility; open bird-eye mesh and micro-mesh for high-ventilation sports like basketball; 4-way poly-spandex elastane (88/12) for compression volleyball and wrestling gear; and heavy-duty 220-280 gsm woven polyester twill for high-contact rugby and lacrosse uniforms.
We utilize digital RIP (Raster Image Processor) color calibration systems linked with standardized Pantone solid coated color books. Every batch of imported eco-solvent sublimation ink is tested against master reference color swatches under standard D65 light booths to ensure less than Delta E 1.0 color variance between re-orders.
Yes. We offer complete white-label and private-label manufacturing services. This includes custom woven neck tags, heat-sealed transfer labels, custom branded size tags, barcode-labeled polybags, custom hang tags, and branded outer master cartons tailored to your enterprise distribution requirements.
Explore our secondary lineup of custom sportswear, specialized athletic apparel, and club equipment.
Partner directly with Shenzhen's premier custom sportswear factory. Get digital vector mock-ups in 24 hours, custom fabric samples, and transparent factory-direct pricing.