


GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore precision-manufactured teamwear featuring Italian eco-sublimation pigments, advanced interlock knits, and automated laser panel grading.
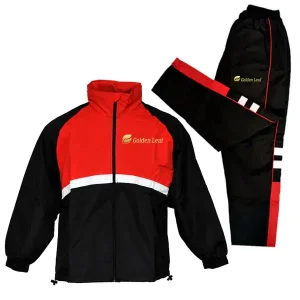
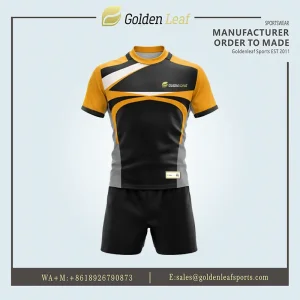
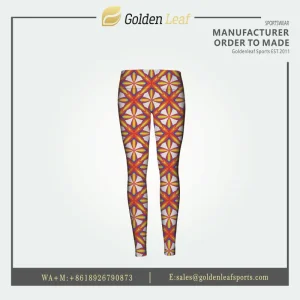
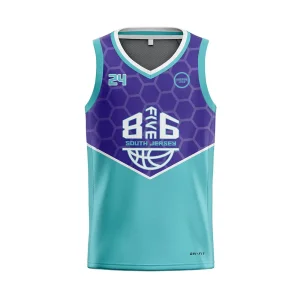
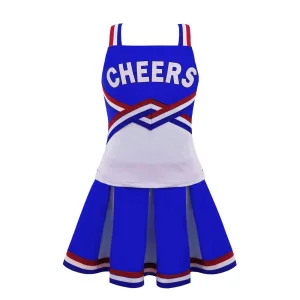
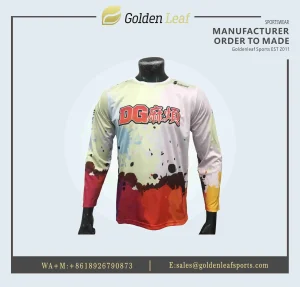
In modern sports gear procurement, a "good kit" goes beyond basic visual styling. It represents a fully integrated engineering system balancing thermodynamic breathability, mechanical tensile elasticity, high-definition sublimation fidelity, and abrasion resilience.
Unlike screen printing or thermal transfers that sit atop fabric fibers and seal off ventilation pores, our 210°C gas-phase dye-sublimation process bonds imported non-toxic ink directly into the polyester polymeric chain. The result is zero cracked prints, absolute breathability, and lifelong pigment durability through intense weekly laundering.
Good kits demand precision GSM targeting. From ultralight 140 GSM bird-eye mesh for high-cardio ultimate frisbee and basketball, up to rugged 280 GSM poly-spandex interlock for collision rugby and contact team wear, our textile blends are optimized to maintain rapid moisture capillary action without structural breakdown.
Every pattern block in our CAD library is digitized with kinetic anatomical motion mapping. We integrate raglan sleeve systems, flatlock friction-free seams, and laser-perforated thermal discharge zones that eliminate athlete chafing while granting uninhibited shoulder rotation during competitive play.
The Greater Bay Area textile ecosystem combines raw yarn manufacturing, advanced chemical dyeing labs, high-throughput digital RIP printing, and skilled artisan sewing within a tightly integrated supply radius.
By housing digital pre-press, automatic continuous roll-fed transfer heat presses, and automated CNC laser tables within our 3,000 m² Shenzhen campus, 3D digital mockups are rendered within 24–48 hours, with physical pre-production master samples shipped in only 5 to 7 business days.
Legacy factories penalize buyers with plate and film setup surcharges for individual names and numbers. Our industrialized print-before-cut sublimation pipeline supports 100% individual personalization across every jersey, short, or pinnie within a standard 10-piece production run at zero penalty.
Five dedicated quality control inspectors evaluate 100% of finished orders prior to packing. We cross-verify delta-E color consistency against Pantone spot masters, run tensile stress tests along sleeve joins, and enforce zero-defect size measurement tolerances before boxing.
Strategic analysis of consumer demands, environmental regulations, and athletic uniform technologies driving commercial tenders across North America, Europe, and Australasia.
Global athletic organizations and school districts increasingly mandate circular supply chains. We offer high-performance circular-knitted yarns extruded entirely from post-consumer recycled plastic bottles. These match virgin polyester in color saturation and tensile rupture thresholds while slashing carbon footprints.
In response to stringent EU REACH directives and zero-discharge standards, our digital transfer operations utilize waterless sublimation dispersion dyes. This eliminates industrial wastewater effluents while securing Oeko-Tex Standard 100 Class I child-skin safety certifications across all team uniforms.
The boundary between matchday sportswear and everyday lifestyle apparel has dissolved. Clubs and corporate sponsors demand good kits that function seamlessly during heavy training, yet offer the refined drape, sleek silhouettes, and comfort required for street wear, fan merchandise, and travel apparel.
Engineered teamwear manufactured to withstand the distinct mechanical stressors and regulatory requirements of diverse sports environments.
High school and varsity leagues require high-durability kits capable of enduring repeated slide tackles, stick checks, and aggressive machine washing. Reinforced double-needle hem seams and snag-resistant bird-eye polyester fabrics ensure jerseys retain their shape and structural integrity throughout grueling multi-month championship seasons.
Rugby scrums, tackles, and rucks generate violent tensile loads along collars and armholes. Our custom rugby kits employ heavy 280–300 GSM stretch-twill panels joined by twin-needle reinforced overlock stitching and tear-proof elastane collars that resist failure under intense physical confrontation.
High-volume corporate activations and charity fun runs prioritize lightweight comfort, reflective safety markers, and high-visibility digital gradients. Our custom running kits utilize 135 GSM micro-interlock knit with 3M Scotchlite reflective transfer piping to ensure athlete safety during low-light dawn and evening runs.
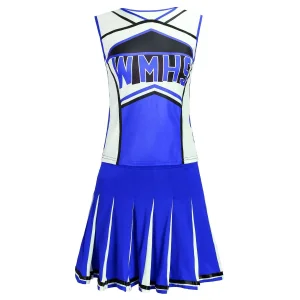
Acrobatic routines necessitate absolute 4-way flexibility with squat-proof opacity. Our cheer and fitness line is engineered with high-gauge 250 GSM poly-spandex blends (88/12) treated with moisture-wicking and quick-drying finishes that eliminate cling, maintain shape recovery, and guarantee non-see-through coverage.
Every batch of technical fabric used in our good kits undergo systematic laboratory testing in accordance with international ASTM and ISO performance criteria.
| Performance Parameter | Test Standard | Our Factory Benchmark | Industry Standard Minimum | Operational Benefit |
|---|---|---|---|---|
| Color Fastness to Washing | ISO 105-C06 / AATCC 61 | Grade 4.5 – 5.0 | Grade 3.5 | Zero bleeding into whites; retains neon intensity after 50+ wash cycles. |
| Fabric Bursting Strength | ASTM D3786 (Hydraulic) | ≥ 380 kPa (Rugby ≥ 520 kPa) | ≥ 250 kPa | Resists ripping, seam blowing, and player jersey grabbing during contact sports. |
| Moisture Wicking Speed | AATCC 197 / JIS L 1907 | ≤ 1.8 seconds | ≤ 5.0 seconds | Transports sweat away from skin instantly, keeping athletes light and cool. |
| Dimensional Stability (Shrinkage) | AATCC 135 (3 Washes @ 40°C) | ± 1.5% Maximum | ± 4.0% | Jerseys and shorts maintain certified size-chart grading without sleeve distortion. |
| Martindale Abrasion Resistance | ISO 12947-2 (Pilling & Wear) | ≥ 25,000 cycles | ≥ 10,000 cycles | Resists Velcro snagging, sports bag friction, and turf pilling over multiple seasons. |
From vector art creation to master container loading, our ISO-compliant manufacturing stages guarantee accountability, traceability, and on-time shipment fulfillment.
Our graphic technicians dissect client vector mockups into 3D CAD pattern pieces, grading curves, scaling sponsors proportionally, and assigning calibrated Pantone spectral values.
Ultra-wide plotters print variable roster numbers, names, and team crests using high-density Italian sublimation inks onto 90 GSM heat-resistant coated transfer paper.
Continuous rotary oil-drum heat calenders press the transfer paper against white polyester panels at 210°C, gaseous-infusing pigments deep into the core fiber yarn matrix.
Vision-equipped laser cutting beds detect printed registration marks automatically, slicing fabric panels with sealed, fray-free edges and zero pattern stretch deviation.
Skilled sewing operators build garments using specialized 4-needle 6-thread flatlock machines, heavy overlock units, reinforced bar-tacking, and custom neck binding tape.
Garments pass through metal detection, loose-thread trimming, full dimension verification, custom poly-bagging, and barcode tagging ready for global DDP air/sea freight.
Purchasing directors and sports brand executives evaluate potential good kits suppliers against strict operational risk metrics to guarantee zero season delays.
For sporting leagues, delivery delays equal canceled games and forfeited seasons. A top-tier factory must provide guaranteed contract fulfillment windows: standard bulk runs of 300 to 2,000 units completed within 12 to 18 operational working days, backed by real-time production status dashboards.
Commercial brand equity relies on proprietary packaging. We supply fully customized woven neck tags, eco-friendly heat-press inner size labels, branded hang tags, custom barcodes, and printed bio-degradable frosted polybags tailored for automated Amazon FBA or central distribution warehouse scanning.
Whether navigating FOB Shenzhen container consolidation, CIF sea freight, or rapid door-to-door DDP (Delivered Duty Paid) air freight via DHL/FedEx, our logistical team handles customs declarations, duty payments, and direct-to-club dropshipping across the US, UK, Australia, and EU.
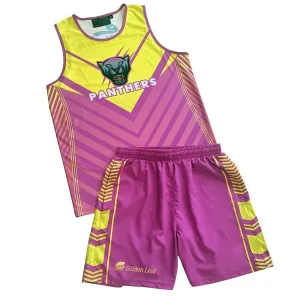
Direct factory manufacturing for competitive basketball programs, running apparel, technical cheer uniforms, and high-compression fitness apparel.
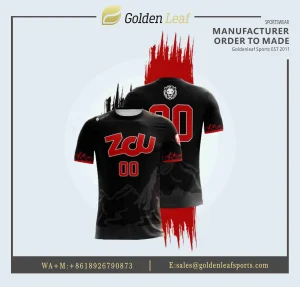
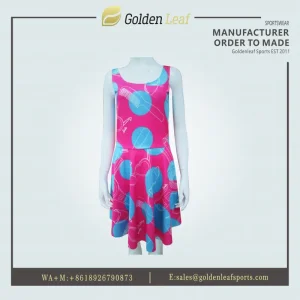
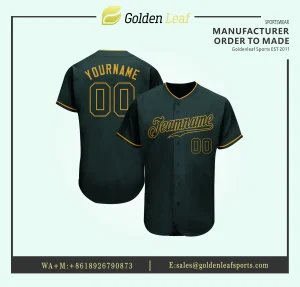
Real-world insights directly from our apparel engineering and export fulfillment teams answering critical questions on specifications, minimums, lead times, and quality control.