GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our engineered apparel inventory developed across high-density interlock, moisture-wicking synthetic matrix, and high-tensile sublimation frameworks.
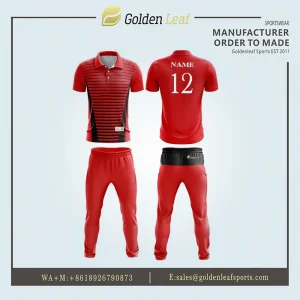
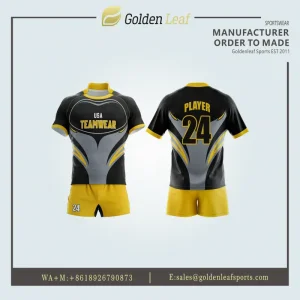
The global sportswear and activewear sector has experienced a paradigm shift over the past decade. Modern consumer expectations, driven by the convergence of high-performance athletics and streetwear fashion ("athleisure"), have forced a structural re-engineering of the conventional menswear supply chain. Sourcing managers, private-label distributors, and corporate apparel buyers searching for premier Men's Tracksuit Companies & Company entities no longer evaluate vendors based purely on unit cost; today's competitive advantage hinges on high information-gain metrics—technological agility, fiber science, structural seam integrity, and end-to-end supply chain transparency.
Historically, tracksuit manufacturing relied on basic cotton-fleece or low-grade polyester blends with rudimentary cut-and-sew operations. Modern activewear demands multi-functional performance fabrics capable of dynamic thermal regulation, advanced moisture management via hydro-wicking capillary channels, 4-way mechanical stretch, and high color-fastness ratings under aggressive laundering cycles. As a result, premier enterprise solutions now integrate digital workflow ecosystems, automated CAD pattern grading, RIP color-management software, and laser registration panel cutting directly into the primary manufacturing line.
Ergonomic 3D panel construction engineered specifically for male anatomical movement, reducing friction zones and optimizing range of motion during athletic performance.
Molecular-level fiber bonding utilizing Eco-friendly imported sublimation inks, preventing graphic degradation, peeling, or cracking across prolonged UV exposure.
Complete ODM/OEM integration including customized woven neck tags, high-density silicone heat-transfers, custom zipper pullers, and retail polybag packaging.
The global activewear market size surpassed USD 380 Billion in recent evaluations, with the specialized men’s tracksuit, hoodie, and team wear segment expanding at a Compound Annual Growth Rate (CAGR) of 6.4%. Sourcing hubs within Southern China—specifically the Shenzhen apparel innovation corridor—lead the industrial ecosystem due to vertical supply integration: yarn spinning, mill dyeing, digital paper printing, laser cutting, and automated assembly operate within tight regional proximity.
Selecting the optimal textile substrate is fundamental to product longevity, breathability, and brand equity. Premier manufacturers offer distinct fabric architectures engineered for specialized wear environments:
| Fabric Composition | Weight (GSM) | Key Performance Property | Optimal Application Scenario |
|---|---|---|---|
| 100% Poly Interlock | 145 - 180 GSM | High tensile strength, maximum dye-sublimation vibrancy | Lightweight active tracksuits, match warmup kits |
| Poly-Spandex Blend (88/12) | 220 - 280 GSM | 4-Way mechanical stretch, multi-directional memory retention | Slim-fit athletic tracksuits, performance joggers |
| Micro-Mesh / Bird-Eye Knit | 130 - 160 GSM | High airflow permeability, rapid moisture evaporation channels | Side paneling, high-perspiration ventilation zones |
| Heavyweight French Terry Poly | 300 - 360 GSM | Thermal insulation, structured silhouette retention | Winter streetwear tracksuits, luxury oversized hoodies |
The roadmap for next-generation tracksuit manufacturing involves deep integration of smart automation, micro-fiber recycling, and digital twin prototyping. Industry-leading OEMs are moving away from traditional physical sampling loops to accelerated digital sample sign-offs, significantly compressing product launch cycles for global brands.
Traditional manual die-cutting often introduces 3-5mm marginal errors across graded size sets. Automated optical camera laser cutting reads printed registration marks on sublimated rolls, ensuring 0.5mm precision across collar curves, sleeve raglans, and pant leg tapers. This eliminates misalignments when sewing multi-panel garments.
Future-focused manufacturing demands strict environmental governance. Transitioning to waterless digital sublimation printing reduces environmental impact. Utilizing OEKO-TEX Standard 100 certified non-toxic inks ensures that activewear pieces coming into direct skin contact are completely free of harmful heavy metals or volatile organic compounds (VOCs).
Tracksuit pants and jackets endure substantial structural strain during intense physical workouts. Utilizing 4-needle 6-thread flatlock seam machinery ensures flush, chafe-free interior stitching, while twin-needle topstitching along high-stress areas (crotch gussets, armholes) extends garment service life under industrial washing routines.
Implementing 3D CAD digital sample renders allows procurement teams to verify vector logo placements, gradient transitions, and sleeve panelling within 24-48 hours. Combined with low Minimum Order Quantity (MOQ) flexibilities (starting at 10 pcs), brands can test micro-trend capsules without committing capital to excessive inventory.
Operating from a state-of-the-art 3,000 square meter industrial campus in Shenzhen, China since 2011, GoldenLeaf Sports represents the operational standard for specialized OEM & ODM teamwear and tracksuit manufacturing. With over 160 skilled apparel technicians—over 80% holding senior certifications in garment pattern construction—GoldenLeaf seamlessly bridges technical engineering with scalable global export capacity.
Every batch undergoes strict inspection by 5 dedicated QA/QC specialists covering fabric tension, ink transfer calibration, seam pull stress, measurement tolerance check, and final packaging audit.
By controlling pattern grading, RIP color profile management, heat-press transfer, laser cutting, sewing lines, and trimming under a single facility, lead times are compressed to 12-18 working days.
Serving premier sporting clubs, high school athletics programs, and commercial brands across North America, Europe, Australia, and the Middle East under flexible EXW, FOB, CIF, and DDP terms.
High-quality tracksuits are engineered to perform across diverse operational environments. Modern manufacturing requires customized design specifications tailored to specific end-use cases:
Designed for athletic squads traveling between venues. Requires comfortable 4-way stretch poly-spandex blends that maintain a pristine, wrinkle-free appearance straight out of team gear bags. Features deep zipped pockets to secure travel credentials and personalized player numbering via high-definition sublimation.
Engineered for cold-weather field sessions in rugby, soccer, or lacrosse. Utilizes brushed fleece back interiors for thermal insulation combined with wind-resistant outer interlock facings. Reinforced collar stands and elasticized sleeve cuffs prevent cold wind penetration while retaining metabolic body heat.
Tailored for high-end gym brands and personal training academies. Emphasizes modern tapered cuts, concealed aesthetic zips, minimalist matte silicone logos, and ultra-soft touch hand-feel to appeal to contemporary fitness consumers seeking versatile gym-to-street apparel.
Built for extreme durability to survive multi-season student use and heavy institutional laundry cycles. Uses heavy-duty 100% polyester interlock with double-stitched stress points, anti-pilling fabric treatments, and colorfast sublimation that resists fading after 50+ commercial washes.
Global apparel sourcing requires strict adherence to international trade regulations, environmental standards, and regional sizing profiles. Professional tracksuit manufacturing platforms provide multi-layered guarantees to safeguard international buyers against import bottlenecks or technical non-compliance:
Detailed answers to fundamental questions asked by commercial apparel buyers, team distributors, and sourcing managers.
Expand your brand line-up with our specialized sublimation athletic wear built to international technical standards.