



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our top-tier custom manufactured teamwear line engineered for elite physical resilience, optimal thermoregulation, and vivid color retention.
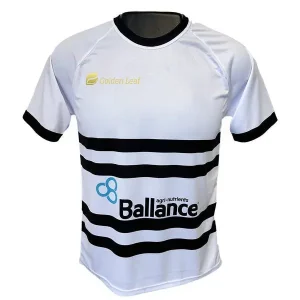
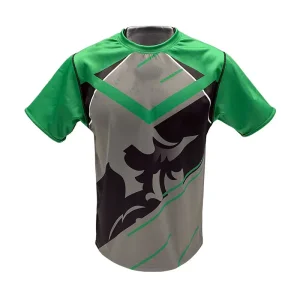
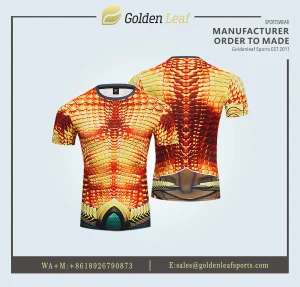
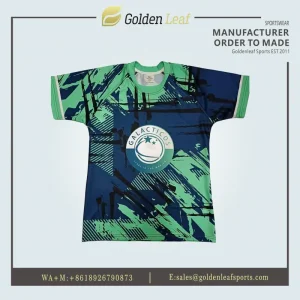
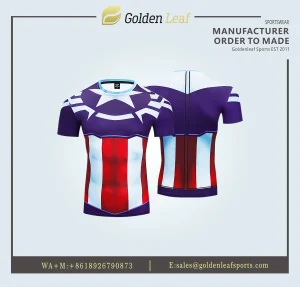
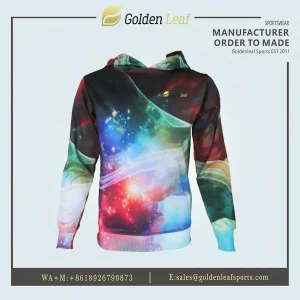
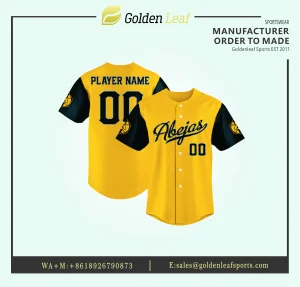
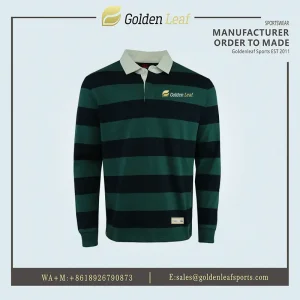
From heavy, water-logged cotton jerseys to ultra-resilient, ergonomic 4-way stretch synthetic textiles.
Traditional 300+ GSM cotton rugby shirts dominated the 20th century. However, under high humidity or rainfall, cotton absorbs up to 27% of its weight in moisture, adding kinetic drag and reducing player speed by up to 4.2%. Modern athletic science has rendered unfunctional fabrics obsolete.
Modern professional rugby demands second-skin athletic block designs. High-tensile poly-spandex blends reduce loose fabric margins that opposing players can grab during tackles, significantly improving pitch mobility while maintaining structural seam integrity under intense physical strain.
Legacy screen printing and vinyl heat transfers add weight, crack under stress, and block fabric breathability. Eco-friendly digital sublimation heat-bonds pigments directly into the polyester core at 210°C, guaranteeing zero added weight, infinite visual customization, and 100% breathability.
Investing in engineered 4-way stretch polyester (220–280 GSM) with reinforced flatlock twin-needle stitching extends garment operational lifespans across competitive seasons by 300% compared to standard promo-grade athletic apparel. This drastically lowers overall replacement expenditure for professional clubs and educational sports bodies.
A granular look at high-tensile fabric matrixing, seam dynamics, and smart moisture management.
| Performance Metric | Standard Retail Athletic Shirt | GoldenLeaf Commercial Rugby Shirt | Elite Pro-Match Specification |
|---|---|---|---|
| Fabric Composition | 100% Standard Polyester (140 GSM) | 100% Poly Interlock / Bird-Eye Mesh (180–240 GSM) | 88% High-Tenacity Poly + 12% Spandex (260–300 GSM) |
| Tensile Strength (Burst Test) | < 350 N (Prone to tearing under tackle) | 650 N - 850 N (High contact endurance) | > 1100 N (Max professional grade contact force) |
| Moisture Evaporation Rate | Slow (> 45 mins dry time) | Rapid (< 15 mins dry time, Cool-Max Hydrophobic) | Instant Active Dry Technology (< 10 mins dry time) |
| Seam Architecture | Basic Single-Needle Overlock Stitch | Reinforced Twin-Needle + Flatlock Seams | 6-Thread Flatlock + Bar-Tack Stress Points |
| Print Technology | Screen Print / Rubber Transfer | Full Digital Italian Sublimation Ink | Full Digital Sublimation + UV Protection Filter |
Rugby training shirts require omnidirectional stretch to accommodate rapid upper-body rotations, scrums, and explosive tackles. GoldenLeaf integrates high-density elastane filaments into micro-polyester knits, delivering 360-degree dynamic movement recovery without fabric deformation or sagging after prolonged washing cycles.
Modern sports analytics rely on player telemetry data. Our OEM manufacturing facility crafts internal elasticized neoprene GPS harness pockets directly into the upper back interior panel of rugby shirts, safeguarding sensitive biometric tracking equipment against direct collision shock during training drills.
Combining automated precision cutting, Eco-friendly sublimation, and zero-defect QA inspection under one roof.
Manual textile cutting leads to pattern misalignments up to 15mm. Our optical camera-assisted CNC laser cutting machines scan printed sublimation registration marks automatically, ensuring 100% seam alignment accuracy across all chest stripes, team logos, and player numbers from size 6Y to 5XL.
GoldenLeaf maintains five dedicated, full-time QA/QC inspectors inside our 3,000 m² Shenzhen plant. Every production batch undergoes rigorous check-points: fabric tension verification, color swatch matching under D65 standard lighting, flatlock seam pull tests, size grading checks, and final single-unit packaging audits.
We eliminate conventional B2B supply chain delays. Virtual digital mock-ups are delivered within 24–48 hours; physical pre-production samples are completed in 5–7 working days; bulk orders of 300 to 1,000 units are fully manufactured and packed within 12–18 working days.
Customized OEM/ODM fulfillment adapted to climate conditions, regional compliance, and club requirements.
Designed for damp, muddy terrain, our UK/European rugby kits utilize DWR (Durable Water Repellent) coated poly-interlock fabrics (240+ GSM). Moisture sheds quickly from the garment surface, keeping players warm without absorbing heavy rainwater during late-autumn and winter fixtures.
For Australian, New Zealand, and South African rugby clubs, solar heat management is critical. We deploy high-gauge micro-mesh polyester featuring UPF 50+ ultraviolet protection. Open-cell airflow channels facilitate rapid heat dissipation during intense pre-season training sessions.
Aligning with global ESG directives, GoldenLeaf offers 100% recycled polyester (rPET) derived from post-consumer plastic bottles. Fully certified under GRS (Global Recycled Standard), our eco-friendly fabrics match virgin polyester in tear strength, dye absorption, and softness.
Direct, factory-level technical guidance written by senior sportswear production technicians.
Our baseline factory MOQ is just 10 pieces per design for custom sublimated rugby shirts. Because every panel is digitally printed on high-speed Italian equipment prior to laser cutting, individual player names, squad numbers, and specific sizing can vary within the same 10-piece run at zero extra fee.
We mandate high-tenacity 6-thread flatlock stitching combined with twin-needle overlocking along all sleeve armholes and side panels. Furthermore, critical high-stress zones such as collar corners and plackets receive automated bar-tack reinforcement to withstand intense physical pulling.
GoldenLeaf uses color-calibrated RIP software combined with imported Eco-friendly inks. We archive digital master print files along with physical fabric swatch target profiles under standardized D65 light boxes, guaranteeing continuous color consistency (Grade 4.5+ fastness) across multi-year reorders.
Yes. Full OEM and ODM private-label customization is standard: heat-transfer inner neck branding, custom woven side tabs, custom hangtags, individual eco-friendly printed polybags, and customized outer carton shipping marks tailored to your distribution warehouse system.
Pre-production physical samples require 5–7 working days. Bulk production (300–1,000 pcs) completes in 12–18 working days. We support EXW, FOB Shenzhen, CIF, and DDP terms via DHL/FedEx express couriers, air freight, or ocean logistics depending on urgency and budget.
We maintain an extensive, pre-graded pattern block library tailored specifically to US, European, Australian, and Asian sizing demographics. Brands can either select our proven regional fit standards or provide custom tech packs for precision pattern grading.
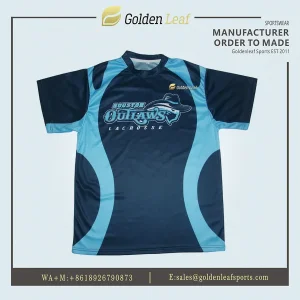
Expand your brand offerings with our full range of sublimated team apparel, hoodies, polos, and daily wear.
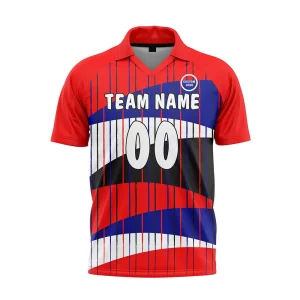
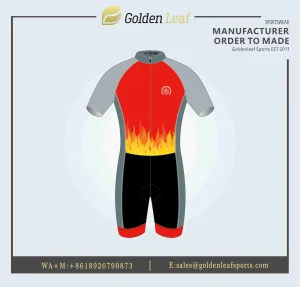
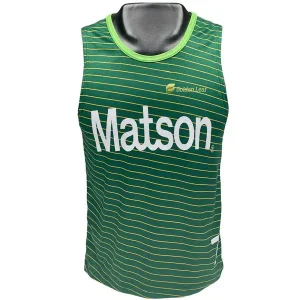
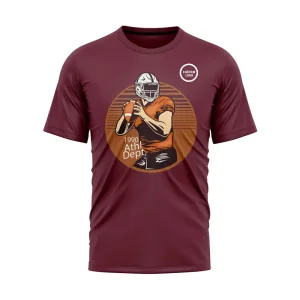
Direct factory pricing, complete OEM/ODM private label customization, and fast 12-18 day bulk manufacturing from our 3,000 m² Shenzhen campus.