GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
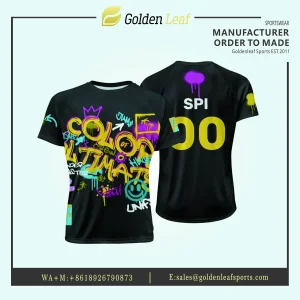
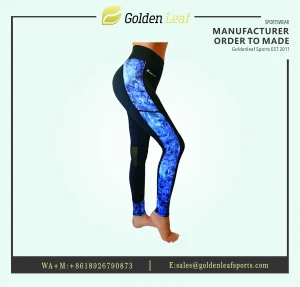
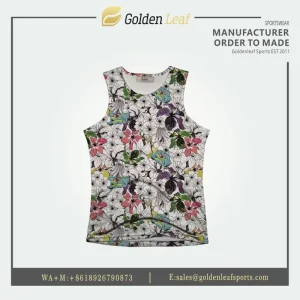
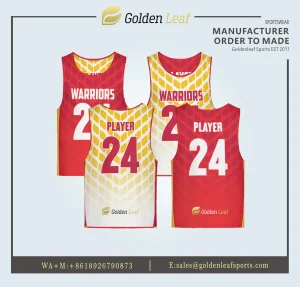
Explore our elite OEM/ODM custom sublimated apparel lines designed for high-intensity athletic performance and commercial wholesale requirements.
Analysis of search intent, structural shifts in athletic teamwear, and why North American brands are migrating toward high-gain OEM manufacturing models.
The athletic apparel ecosystem across North America is experiencing an irreversible shift from traditional screen-printed and vinyl-tackled twill uniforms toward high-definition, thermal-bonded sublimation basketball sets. Modern athletic organizations—ranging from high-profile Amateur Athletic Union (AAU) circuit teams to National Federation of State High School Associations (NFHS) member programs and NCAA collegiate outfits—demand lightweight, non-restrictive, highly durable, and infinitely customizable team kits.
While domestic US companies excel at client management, branding, and local sports league distribution, their on-shore manufacturing capabilities often suffer from high labor overheads, limited textile substrate variations, and capacity bottlenecks during peak season demand (August through November). Consequently, leading US sportswear suppliers increasingly partner with expert Chinese manufacturing hubs—such as Shenzhen-based GoldenLeaf Sports—to execute precision digital sublimation, pattern grading, and automated sewing assembly under rigorous Quality Assurance standards.
Sublimation is not merely printing on fabric; it is a thermal molecular gas-bonding process requiring microscopic precision.
Unlike screen printing, which deposits a thick layer of plastisol ink on top of the fabric (blocking ventilation pores and causing cracking over time), dye-sublimation transforms disperse inks into a gaseous state under high heat (200°C–220°C) and pressure. The ink gas penetrates the open polymer chains of the polyester fiber, becoming an integral part of the yarn structure.
We utilize 100% virgin high-tenacity polyester substrates ranging from 145 GSM to 220 GSM. Choice fabrics include Bird-Eye Mesh for maximum ventilation, Interlock Poly-Knit for smooth compression and structure, and 4-Way Stretch Poly-Spandex Blends (88/12) for elite athletic mobility.
Utilizing imported Japanese fluo inks and Italian Kiian digital sublimation inks paired with ErgoSoft RIP calibration software, our production line guarantees exact Pantone matching (PMS System) with a Delta-E variance below 1.0. Colors remain vibrant wash after wash.
| Performance Metric | Traditional Screen Printing | Tackled Twill (Embroidered) | GoldenLeaf Sublimation Standard |
|---|---|---|---|
| Breathability / Air Permeability | Poor (Blocked by plastisol layer) | Moderate (Heavy patch areas) | Optimal (100% unblocked mesh pores) |
| Garment Weight (Jersey + Shorts) | Approx. 480 - 520 grams | Approx. 650 - 800 grams | Ultra-lightweight (310 - 360 grams) |
| Color / Graphic Limits | Cost increases per color pass | Limited to pre-cut fabric colors | Unlimited colors, gradients, vector art |
| Longevity & Durability | Peels & cracks after 20-30 washes | Fraying edges over 1-2 seasons | Lifetime guarantee (Zero fading/peeling) |
| Player Personalization Cost | High fee per player name/number | Very high labor expense | Included in base cost (0 additional fee) |
Why US sports exporters and apparel brands rely on GoldenLeaf Sports' integrated 3,000m² Shenzhen infrastructure for scalable production.
Shenzhen, located within the Greater Bay Area of China, is recognized globally as the center of high-tech digital manufacturing and textile engineering. Unlike traditional textile regions focused purely on manual cut-and-sew labor, Shenzhen integrates modern digital workflows, high-speed automated laser cutting, and computerized dye-sublimation technology.
At GoldenLeaf Sports (ShenZhen) Co., Ltd., we control every step of the garment cycle. From pattern grading and virtual 3D rendering to wide-format Mimaki printing, heat calender transfer, precision optical laser cutting, flatlock assembly, and final QC inspection—nothing is outsourced to secondary subcontractors. This guarantees absolute quality control and eliminates production delays.
By sourcing raw performance polyester directly from strategic mill partners in Guangdong and utilizing high-speed ocean and air routes out of Shenzhen/Hong Kong ports, we pass substantial cost savings onto US exporters. You receive premium-tier sportswear constructed with top-tier materials at a fraction of North American domestic production costs.
Understanding how custom sublimated basketball sets fit into key American athletic sectors.
AAU programs play dozens of games over weekend tournaments. They require lightweight, quick-drying reversible sublimation jerseys that allow teams to switch between home and away colors instantly without doubling bag weight. Our dual-layer mesh bonding ensures complete opacity with maximum thermal regulation.
High school athletic directors must strictly comply with NFHS uniform guidelines regarding number placement, jersey sizing, side panel dimensions, and manufacturer logo sizing. Our technical team works from pre-approved NFHS block patterns to ensure 100% referee and league compliance.
University athletic departments demand extreme wash-and-wear resilience. Our heavy-duty interlock polyester fabrics survive industrial laundry washing cycles without losing color brilliance, shrinking, or seam unraveling over multi-year varsity use.
Modern streetwear fashion increasingly merges basketball uniforms with urban fashion. We supply custom lifestyle apparel brands with full-print oversized basketball jerseys, retro mesh shorts with custom ribbing, matching warm-up jackets, and luxury hoodies.
How high-volume US apparel companies mitigate inventory risk through Agile Manufacturing & Just-In-Time (JIT) fulfillment.
Traditional sportswear distribution forced US companies to purchase tens of thousands of dollars in blank inventory, tying up capital and taking on major mark-down risks for unsold sizes. Through GoldenLeaf's B2B On-Demand Manufacturing API/Fulfillment Workflow, US dealers can take online team orders first, and then submit accurate digital vector files directly to our factory.
We produce exact team quantities (e.g., 12 jerseys in specific sizes with custom names/numbers) and ship directly to your door within 14 calendar days, turning supply chain liabilities into high-margin profitability.
Navigating international trade regulations requires strategic classification. By accurately categorizing performance knit apparel under specific HTS code classifications (e.g., HTS 6109.30 for synthetic performance shirts) and optimizing master carton packaging densities, we help US importers reduce landed freight expenses by 12% to 18%.
Furthermore, our flexible delivery terms (FOB Shenzhen, CIF Los Angeles, or DDP direct to warehouse) provide complete agility over your custom logistics pipeline.
Pioneering eco-friendly textiles, smart moisture management, and AI-driven pattern customisation.
Sustainability is now a core requirement for US high school and university athletic bids. We lead the industry by offering 100% post-consumer recycled polyester yarn (rPET derived from recycled plastic bottles) that retains identical wicking, softness, and sublimation color vibrancy while reducing carbon footprint by 45%.
Modern high-end basketball kits incorporate embedded silver-ion antimicrobial coatings into the fiber matrix. This inhibits odor-causing bacteria growth during multi-game tournament play, maintaining freshness over extended wearing hours.
Next-generation basketball kits combine full sublimation with laser-cut micro-perforations located strategically along high-heat body zones (underarms, back spine, and lower side panels) to maximize airflow velocity while maintaining structural garment integrity.
In-depth technical and operational answers to support procurement, quality control, and supply chain decisions.
Discover additional multi-sport custom sublimated products engineered in our Shenzhen manufacturing hub.