



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered for high-intensity athletics, tournament play, and branded merchandise distribution worldwide.
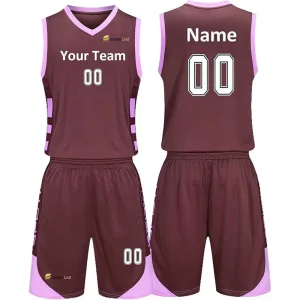
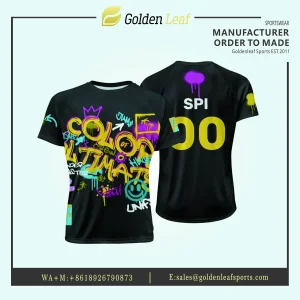
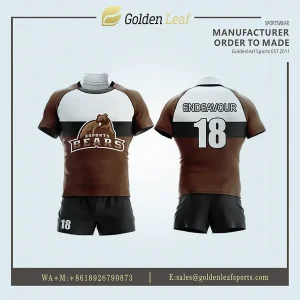
Understanding the transition from traditional screen printing to end-to-end digital dye-sublimation for thermal sportswear.
Unlike traditional screen printing or direct-to-garment (DTG) applications that deposit ink layers on top of fabrics, digital dye sublimation transforms disperse dyes into a gaseous state under high heat (190°C–215°C) and pressure. The ink fuses directly into the polyester polymer core, guaranteeing zero peeling, cracking, or color degradation over extended commercial laundry cycles.
Sublimation sweatshirts offer unlimited edge-to-edge artwork positioning. Enterprise buyers can integrate complex gradients, photographic illustrations, high-definition vector motifs, sponsor arrays, and individualized player names/numbers across sleeves, hoods, kangaroo pockets, and back panels without incurring setup costs per additional color.
Heavyweight fleece and brushed poly-interlock fabrics retain 100% of their natural breathability, moisture-wicking capillary action, and thermal insulation. Because sublimation leaves no rubberized ink barrier, micro-fleece structures remain soft, flexible, and completely unimpeded for athletic movement.
A comparative evaluation of apparel manufacturing methodologies for enterprise buyers evaluating long-term product performance.
| Evaluation Parameters | Digital Dye-Sublimation | Screen Printing | Direct-to-Garment (DTG) | Heat Transfer Vinyl (HTV) |
|---|---|---|---|---|
| Color Fastness (ISO 105-B02) | Grade 4.5 - 5.0 (Maximum) | Grade 3.5 - 4.0 | Grade 3.0 - 3.5 | Grade 2.5 - 3.0 |
| Fabric Breathability | 100% Unaffected | Blocked at print zones | Slightly stiffened | 100% Non-breathable film |
| Setup Cost / Plate Fees | $0 (Fully Digital) | $25 - $50 per color/screen | $0 (Digital) | $0 (Cutting setup) |
| Individualization (Names/Numbers) | Seamless (0 extra cost) | Cost-prohibitive | Moderate speed limit | Manual labor intensive |
| Durability & Peel Resistance | Permanent (Fibre level) | Prone to cracking over time | Gradual fading after 20 washes | Prone to edge peeling |
| Optimal Fabric Composition | 100% Poly / Poly-Spandex Blends | Cotton, Blend, Polyester | 100% Cotton / High-Cotton Blends | Universal application |
GoldenLeaf Sports utilizes premium-grade white polyester fleece ranging from 260 GSM to 340 GSM. Our proprietary double-knit brushed fleece features a high-density 100% polyester smooth face optimized for vibrant RIP-managed transfer, backed by a soft, lofted inner micro-fleece surface designed for static reduction and optimal thermal insulation in cold-weather conditions.
Our digital printing arrays employ OEKO-TEX ECO PASSPORT certified dye-sublimation disperse inks. Free from alkylphenol ethoxylates (APEO), heavy metals, formaldehyde, and banned azo dyes, our ink systems achieve precise Pantone matching (Delta E < 1.0) while adhering to strict EU REACH and US CPSIA environmental standards.
Why sourcing custom sportswear from specialized Pearl River Delta production clusters offers unmatched scalability, speed, and cost efficiency.
Housing end-to-end capabilities under one roof: artwork RIP proofing, large-format printing, continuous roll heat presses, automatic laser cutting, precision sewing, and 5-stage quality assurance.
Over 80% of our production staff possess 10+ years of technical apparel craftsmanship, operating specialty machinery such as 4-needle 6-thread flatlock machines for zero-chafe seams.
Digital proofing delivered within 24–48 hours. Pre-production physical samples completed in 5–7 days. Full bulk production cycles (300 to 1,000+ pieces) dispatched in 12–18 working days.
Five dedicated full-time QA/QC inspectors check greige fabric stability, print registration, panel dimensions against tech packs, seam tensile strength, and packing accuracy.
A standardized, transparent 8-stage production timeline engineered for international sportswear brands, distributors, and teamwear suppliers.
Specification of sweatshirt silhouettes (hoodie, crewneck, quarter-zip), fabric weight (GSM selection), ribbing style, and accessory requirements.
Selection or creation of regional size charts (US, EU, AU, Asian, Youth) with custom sleeve length, chest drop, and shoulder seam adjustments.
Placement of high-resolution vector artwork onto 2D pattern flat templates. Color calibration according to target Pantone TCX/PMS codes.
High-speed digital inkjet output onto specialized coated transfer paper, followed by deep calendar heat transfer press processing.
Optical camera registration software guides high-precision laser cutters to slice sublimated fabric panels along exact seam allowances.
Assembly using heavy-duty thread, reinforced neck taping, lined fleece hoods, reinforced kangaroo pockets, and custom rib cuffs.
Application of custom woven neck labels, heat-transfer wash tags, barcode hangtags, individual eco-polybagging, and SKU sorting.
Final 100% inspection pass, pre-shipment photographic reporting, and expedited air, express, or sea container dispatch under FOB/DDP terms.
Ensuring seamless international import compliance, regional sizing alignment, and strict environmental safety standards.
Our apparel exports fully comply with stringent Western import directives. Fabrics and dyes are regularly audited to ensure compliance with EU REACH Regulation (EC No 1907/2006), OEKO-TEX Standard 100 Class I (safe for skin contact), and US CPSIA lead and phthalate limitations for youth apparel.
Standardized Asian sizing frequently leads to high return rates in Western markets. GoldenLeaf Sports maintains dedicated, pre-graded pattern libraries specifically scaled for North American (US/CA), European (EU), and Australasian (AU/NZ) anatomical proportions, ensuring true-to-fit sizing for adult and youth teams.
We provide comprehensive trade terms including EXW, FOB Shenzhen / Yantian, CIF, and DDP (Delivered Duty Paid). Our integrated freight forwarder network streamlines customs brokerage, import duty handling, and door-to-door delivery directly to enterprise warehouses or retail fulfillment centers.
Delivering high-performance fleece garments customized for specialized vertical sectors across global markets.
Ideal for sideline travel hoodies, warm-up hoodies, and off-field team kits for Lacrosse, Rugby, Football, Basketball, and Volleyball organizations. Sublimated hoodies resist weather exposure and continuous locker-room laundering without fading squad colors or sponsor logos.
Custom university bookstores and high school athletic departments require complex mascot art, detailed vintage typography, and vibrant school colors. Dye sublimation allows high-density heraldic crests and multi-tone sleeve striping at accessible price points.
Esports teams demand high-tech, cyber-aesthetic apparel with hyper-detailed graphics, futuristic color gradients, and extensive sponsor logo arrangements across the chest, shoulders, and back panels. Sublimation delivers crisp line definitions down to 0.5pt.
Emerging apparel brands leverage our flexible 10-piece MOQ to launch limited-edition drops, all-over print (AOP) graphic hoodies, and abstract artistic collections without locking up working capital in heavy inventory holding costs.
Enterprise tech firms, automotive brands, and promotional agencies utilize custom sublimated quarter-zips and hoodies for trade shows, product launches, and employee gifts, matching exact corporate brand color identity systems.
Heavy-duty poly-fleece sweatshirts designed for pit crews, motocross racers, and outdoor fishing clubs requiring high visibility, wind-resistant outer shell fabrics, and vibrant fade-resistant high-visibility fluorescent inks.
Pioneering technical innovations shaping the next decade of performance thermal sportswear.
The industry is rapidly shifting toward 100% Recycled Polyethylene Terephthalate (rPET) derived from post-consumer plastic bottles. Modern rPET fleece offers identical tensile strength, dye acceptance, and soft hand-feel while reducing carbon footprint by up to 45% per garment produced.
Integration of artificial intelligence pattern nesting software optimizes fabric utilization rates up to 94%. Paired with automated vision-guided laser cutting systems, textile waste is drastically minimized while panel edge-sealing prevents fabric fraying during assembly.
Reducing physical sample iterations from weeks to hours: 3D CAD draping software allows enterprise clients to inspect fabric stress heatmaps, stitch tension simulations, and real-time lighting previews of customized sublimated sweatshirts prior to cutting fabric.
Detailed answers to technical, operational, and financial inquiries posed by sportswear buyers, procurement directors, and brand owners.
Our standard Minimum Order Quantity (MOQ) is 10 pieces per design for custom sublimated sweatshirts, hoodies, and team pullovers. Because every garment panel is digitally printed on high-speed inkjet arrays prior to cutting and sewing, individual player names, squad numbers, and specific size variations (from 6Y to 5XL) can be mixed within the same 10-piece run at no extra charge.
We utilize specialized 280 GSM to 340 GSM 100% polyester double-knit fleece with anti-pilling outer face finishing. The inner lofted fleece traps dead air to create exceptional thermal insulation, while the outer face undergoes an anti-friction process that resists surface pilling caused by backpack straps, velcro, or washing friction. Unlike cotton, polyester fleece does not absorb moisture, keeping athletes warm and dry in wet or freezing environments.
Yes. Our in-house design team utilizes calibrated ErgoSoft and Wasatch RIP (Raster Image Processor) software to convert vector artwork into precise color profiles matching Pantone Matching System (PMS / Solid Coated & Uncoated) standards. We conduct mini color-strike-off press tests on actual production fabric prior to bulk printing, guaranteeing a color accuracy margin within Delta E < 1.0.
Digital 2D/3D mock-ups are delivered within 24 to 48 hours. Once artwork is approved, physical pre-production samples require 5 to 7 working days. Standard bulk orders (300 to 1,000+ pieces) complete production within 12 to 18 working days inside our own 3,000m² Shenzhen facility. Expedited rush services are available upon request for critical tournament deadlines.
We offer complete Original Design Manufacturing (ODM) private-label packaging packages. This includes custom woven neck labels, heat-transfer satin wash care labels, branded cardstock hangtags with plastic barbs, printed eco-friendly polybags, metal aglets/drawstring tips, custom branded zipper pulls, and outer carton marking tailored to your logistics requirements.
No. Because dye-sublimation infuses disperse dye directly into the synthetic polyester microfibers at a structural level, the print becomes an integral part of the fabric itself. It is chemically impossible for sublimated artwork to peel, crack, or flake off. Furthermore, synthetic polyester exhibits superior dimension stability, undergoing less than 1% thermal shrinkage under standard warm water wash cycles.
All textiles and inks used at GoldenLeaf Sports undergo rigorous international safety testing. Our materials comply with OEKO-TEX Standard 100 Class I guidelines, European REACH chemical regulations, and American CPSIA standards ensuring zero hazardous heavy metals, organotin compounds, or toxic azo dyes are present in finished garments.
Explore our extended manufacturing capabilities spanning multi-sport uniforms, reversible kits, and specialized outerwear.
Connect directly with our Shenzhen technical team for rapid fabric sampling, 24-hour virtual vector proofing, and competitive OEM/ODM factory-direct quotations.