GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
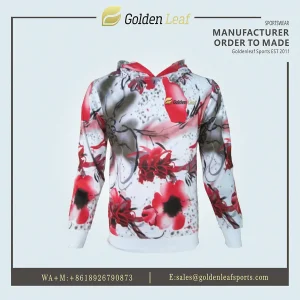
Explore our export-grade sublimated apparel manufactured at our 3,000 m² Shenzhen facility using imported Eco-friendly inks and automated panel cutting.
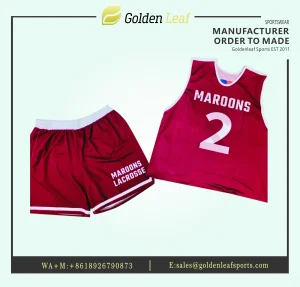
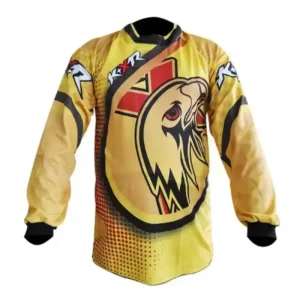
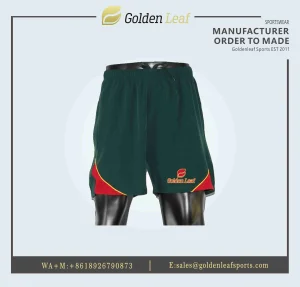
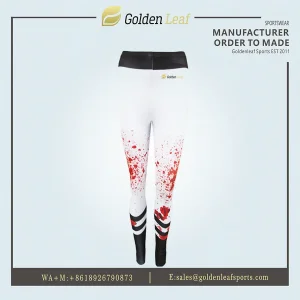
Analyzing the paradigm shift from traditional screen-printed teamwear to high-tension digital dye-sublimated performance apparel.
Unlike screen printing which deposits a thick coat of PVC paste over fabric pores, dye sublimation binds color at the molecular level. This preserves maximum garment breathability, zero added weight, and lifelong color fastness under rigorous commercial wash cycles.
Sublimated volleyball shorts, compression tights, and spandex pants must survive extreme friction against hardwood indoor courts and abrasive beach sand. Tensile strength and seam elasticity are essential to prevent tear failures during intense play.
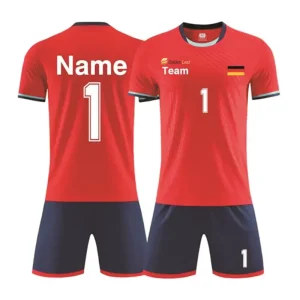
By printing cut panels digitally prior to assembly, complex gradient patterns, high-definition club crests, individual player names, and numbers can be rendered in a single print run with zero extra cost per customization detail.
How specialized poly-spandex blends and moisture-management capillary structures optimize player efficiency and garment longevity.
Engineered with 180 to 260 GSM high-multi-filament polyester intertwined with premium DuPont Spandex. This ratio offers 4-way mechanical stretch, returning to original garment dimensions instantly without sag or distortion.
Utilizing micro-groove yarn profiles (such as Cool-Max and Bird-Eye mesh structures), liquid sweat is wicked from the player’s skin surface to the outer fabric face, speeding up evaporation by over 40% compared to standard cotton or low-grade polyester.
Constructed using 6-thread 4-needle flatlock sewing machinery. Seams lay completely flat against skin tissue, virtually eliminating friction abrasion during continuous floor dives, sliding maneuvers, and repetitive jumps.
Examining the speed, raw material ecosystem, technological integration, and cost efficiencies of Chinese custom teamwear production.
Factories utilize eco-friendly, non-toxic sublimation inks (such as Kian and J-Teck) that comply with OEKO-TEX Standard 100. Colors stay vibrant through 50+ industrial washes, achieving Level 4-5 color fastness ratings.
Digital RIP software and automated laser cutters allow factory technicians to output virtual mock-ups in 24 hours, physical samples in 5 days, and bulk orders starting at an accessible 10 pcs/design minimum threshold.
Every garment undergoes stringent Quality Assurance checks across size-grading accuracy, stitch tension, color hue reproduction, waist elasticity, and seam pull-stress before polybag sealing.
Customizing sublimated volleyball shorts, tights, and team apparel for regional rules and regional play styles.
Strict NCAA and NFHS guidelines dictate solid Libero contrast colors, uniform number dimensions (minimum 4-inch front, 6-inch back), and specific non-abrasive waistband construction. Sublimation ensures compliance without heavy patches.
European buyers prioritize sleek, ergonomic European block patterns, multi-sponsor logo integration, high elastane compression ratios, and eco-certified sustainable polyester yarns (rPET).
Outdoor sand volleyball gear requires UPF 50+ ultraviolet solar protection, salt-water and chlorine resistance, quick-dry micro-fibers, and reinforced anti-sand elastic waistbands.
Key technologies driving the future of sublimated sportswear export and wholesale manufacturing.
Factories are replacing manual paper pattern grading with AI-assisted vector mapping. 3D virtual simulation allows overseas brand managers to audit garment draping, seam stress points, and pattern alignment prior to physical sampling.
Environmental regulations and consumer demand are driving the adoption of 100% post-consumer recycled polyester yarns derived from plastic bottles. When paired with water-based eco-sublimation inks, the carbon footprint drops by up to 30%.
Modern volleyball shorts feature anatomical zone compression to reduce muscle oscillation and delay fatigue. Silver-ion anti-odor treatments are embedded directly into yarn matrices to combat odor-causing bacteria growth.
Essential verification steps for global sportswear importers, distributors, and custom apparel brand owners.
Verify that the factory utilizes standardized Pantone (PMS) matching libraries and calibrated RIP software. This guarantees that your brand’s custom team colors remain consistent across separate production batches worldwide.
Ensure your factory supplier provides detailed sizing specs (US, European, and Youth blocks). Proper elastane stretch allowance must be calculated into digital vector files before panel laser cutting begins.
Look for established production metrics: a minimum 3,000 m² clean facility footprint, 100+ skilled sewing technicians, third-party audit capability, and AQL 2.5 final inspection protocols prior to carton dispatch.
Explore additional customized sportswear items manufactured with low MOQs, custom branding, and quick global shipping.
Comprehensive answers regarding minimum order quantities, lead times, sublimation ink safety, and custom branding services.
Our flexible standard MOQ is 10 pieces per design for sublimated teamwear including volleyball shorts, pants, and jerseys. Because each panel is printed digitally prior to laser cutting, player names, numbers, and custom sizes can vary across the 10-piece run at no extra charge.
Digital vector mock-ups are produced within 24 to 48 hours. Physical pre-production samples require 5–7 working days. Standard bulk production runs (300 to 1,000 pieces) ship within 12 to 18 working days directly from our Shenzhen facility.
We stock 100% polyester interlock (145–180 GSM), micro-mesh, bird-eye mesh, and high-elastic 4-way stretch poly-spandex blends (88% Polyester / 12% Spandex; 180–260 GSM). All fabrics are pre-tested for color fastness and tensile strength.
Yes. We offer complete OEM/ODM solutions: customized woven neck labels, heat-transfer inner sizing labels, custom hang tags, barcode stickers, printed polybags, and master-carton markings tailored to your brand specifications.
We log every client design with precise Pantone (PMS) color codes inside our color-managed RIP software profiles. This ensures color matching accuracy across repeat bulk production orders season after season.