



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our high-performance custom teamwear engineered with premium moisture-wicking fabrics, digital sublimation printing, and reinforced stitching for extreme athletic performance.
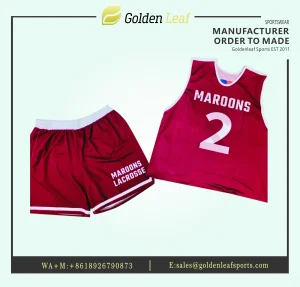
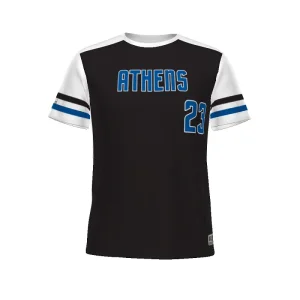
From Heavyweight Cotton-Wool Twill to Bio-Engineered Synthetic Polymers: Sourcing Trends for 2025–2030.
The global market for wholesale baseball uniforms is experiencing a structural shift driven by modern athletic demands, rapid custom team wear turnarounds, and advances in textile chemistry. Historically dominated by heavyweight woven polyesters and embroidered tackle twill, today’s professional clubs, high school leagues, and youth travel organizations demand ultra-lightweight, 4-way stretch, and moisture-regulating athletic gear.
Commercial buyers—ranging from independent team wear brands to international distributors—now prioritize integrated supply chain hubs capable of seamlessly managing digital dye-sublimation printing, pattern grading, and low-MOQ rapid re-orders without compromising garment integrity under friction and intense game play.
Enterprise athletic apparel procurement officers face mounting pressure to eliminate stockouts during peak spring training and fall tournament seasons. Conventional supply chains with 90-day lead times are increasingly deemed obsolete.
Modern B2B buyers require direct factory partnerships in specialized garment ecosystems like Shenzhen, China, offering agile manufacturing parameters. Key decision drivers include precise Pantone matching accuracy (ΔE < 1.0), zero color bleeding, reinforced double-needle seam strength, and guaranteed compliance with international labor and environmental benchmarks.
Established in 2011, GoldenLeaf Sports operates an end-to-end 3,000 m² apparel manufacturing facility engineered for precision B2B custom team wear production.
A granular breakdown of fabric selection, density calibration, stitching tech, and dye sublimation science.
Choosing the right fabric substrate dictates athlete comfort and garment lifespan. We utilize engineered 100% micro-polyester and poly-spandex blends specifically designed for high-abrasion outdoor sports.
Digital sublimation bonds ink directly into the molecular structure of the polyester fiber using thermal gas transfer at 200°C–220°C.
Baseball uniforms experience extreme strain at button plackets, shoulder seams, and waistbands during sliding and diving action.
Eliminating supply chain friction through custom packaging, low MOQs, and private label integration.
Traditional apparel factories require 500+ pieces per design, restricting small leagues and specialty sport shops. GoldenLeaf Sports solves this bottleneck by offering a flexible Minimum Order Quantity (MOQ) of just 10 pieces per design.
Because each garment panel is digitally printed prior to cutting and sewing, individual player names, numbers, and custom sleeve patches can be varied within the same 10-piece run at zero extra setup fee. This capability makes our production line ideal for rapid mid-season player replacements and roster updates.
We empower international team wear brands and sporting goods exporters to scale their private-label lines effortlessly. Our turnkey OEM/ODM services include:
Ensuring international compliance, sizing accuracy, and multi-stage factory quality control.
Different international markets have distinct athletic sizing profiles. GoldenLeaf Sports maintains fully calibrated block patterns for key export markets:
To guarantee zero defects upon arrival, our factory employs 5 full-time QA/QC inspectors stationed at key production bottlenecks:
We facilitate seamless global door-to-door delivery with flexible international shipping terms tailored to buyer preferences:
How Artificial Intelligence, Automated Cutting, and Recycled Polymers are Revolutionizing Teamwear Manufacturing.
GoldenLeaf Sports is integrating AI algorithmic nested marker software into our pre-production pipeline. This technology optimizes fabric utilization during laser cutting, reducing material waste by up to 14% while generating instant, hyper-realistic 3D garment proofs for enterprise buyer approval.
In response to global sustainability initiatives, our research and development unit has successfully tested 100% Recycled Polyethylene Terephthalate (rPET) yarns derived from post-consumer plastic bottles. These eco-friendly yarns exhibit identical tensile strength and dye uptake as virgin polyester, offering sports brands a clean environmental narrative.
Next-generation prototype team wear incorporates micro-channel hydrophilic fibers that actively adjust moisture evaporation rates based on skin micro-climate temperatures. This keeps baseball players cooler during hot summer double-headers while insulating against cold wind drafts during evening games.
Direct factory answers to common procurement questions asked by wholesale buyers, league directors, and brand owners.
Our standard factory MOQ is 10 pieces per design for sublimated baseball jerseys, pants, and team outerwear. Because each panel is printed digitally before laser cutting, individual player names, numbers, and sizes can be fully customized within the same 10-piece batch without incurring extra setup charges. Sample orders (1-3 pieces) are also available for physical quality and sizing evaluation prior to bulk production.
Digital artwork proofs and 3D mock-ups are delivered within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk orders ranging from 300 to 1,000 pieces are manufactured and packed within 12 to 18 working days after official proof approval, handled entirely within our 3,000 m² Shenzhen facility.
Dye sublimation infuses color directly into the polyester fibers under heat and pressure. Unlike screen printing, sublimated graphics will never crack, peel, or fade. Compared to traditional tackle twill embroidery, sublimated jerseys are up to 35% lighter, significantly more breathable, and eliminate heavy stiff backing behind logos and player numbers, maximizing player comfort and movement on the field.
Yes. We support all major structural styles, including full-button front, two-button placket, v-neck pullover, and sleeveless vest styles. We offer custom knitted braid piping along the placket, collar, and sleeve cuffs in standard 1/8", 1/4", or custom multi-color braid configurations to meet classic or modern team aesthetics.
Absolutely. Our turnkey private label services include custom woven or heat-transfer neck tags, custom branded hangtags with barcodes, size stickers, custom polybags, and outer master carton markings tailored to your brand's warehousing standards. We maintain strict confidentiality and IP protection for proprietary client artwork.
We utilize calibrated RIP digital printing software paired with imported high-chroma eco-friendly inks. Every color formula is archived under your master account with exact Pantone Solid Coated / TCX color codes. Before printing production runs, target swatches undergo digital colorimeter scans to ensure a Color Difference metric (ΔE) of less than 1.0.
Explore our multi-sport custom apparel solutions engineered for clubs, schools, and global distributors.
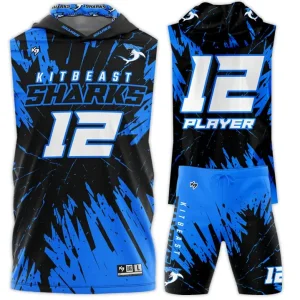
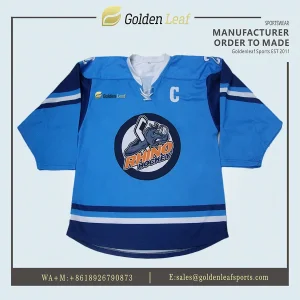
Partner directly with GoldenLeaf Sports (Shenzhen) for premium OEM/ODM team wear production, free 24-hour design mock-ups, and rapid 12-day bulk turnarounds.