GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our top-tier sublimation printed apparel lines manufactured with zero-fading tech and high-airflow structural fabrics.
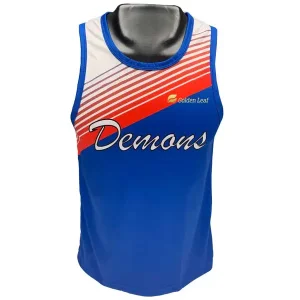
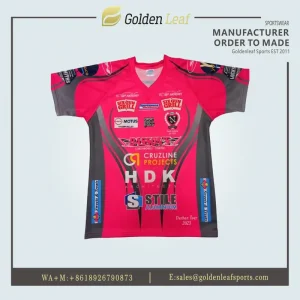
Analyzing the shift from heavy traditional riding apparel to ultra-lightweight, micro-perforated ergonomic racing kits in North America, Europe, and Oceania.
Modern off-road, Enduro, and MX riders demand extreme breathability. Traditional 200+ GSM solid polyester weaves have been replaced by multi-zone micro-perforated mesh fabrics with Cubic Feet per Minute (CFM) airflow ratings exceeding 180, significantly reducing heat exhaustion during multi-hour rally competitions.
With the universal adoption of chest protectors, neck braces, and back guards, OEMs must design jerseys with raglan sleeves and 4-way stretch poly-spandex zones. This guarantees unrestricted body movement while keeping sleeve cuffs tight to prevent snagging on trail vegetation.
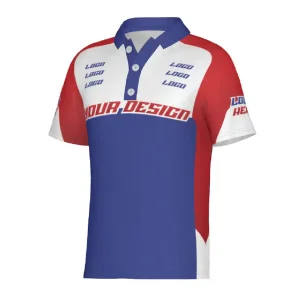
Screen printing and heavy vinyl transfers are obsolete in professional MX gear due to airflow blockage and peeling under mud pressure. Digital thermal sublimation infuses non-fading Italian inks directly into the polymer matrix, keeping the jersey 100% breathable across all printed panels.
How advanced OEM textile mills balance high-tenacity tear resistance with rapid capillary wicking systems for professional motocross brands.
During high-intensity Enduro races, human skin produces over 1.5 liters of sweat per hour. GoldenLeaf Sports utilizes specialized dual-surface knitted structures: an inner layer composed of hydrophobic micro-denier yarns that pull perspiration directly off the skin, and an outer hydrophilic layer that disperses moisture across a broad surface area for instant ambient evaporation.
Off-road environments subjects apparel to constant roost, branches, and soil friction. OEM engineering requires strategic fabric zoning: lightweight Bird-Eye mesh under armpits and chest for max air intake, reinforced 180GSM interlock polyester on the sleeves, and heavy-duty silicone tail-prints to keep the jersey tucked firmly into the racing pants.
| Fabric Grade / Structure | Weight (GSM) | Air Permeability (CFM) | Tensile Strength (N) | Primary Application Zone |
|---|---|---|---|---|
| Ultra-Air Micro Mesh | 135 - 145 GSM | 210 + CFM | 320 N | Underarm & Side Panels |
| Pro-Performance Bird-Eye Mesh | 150 - 165 GSM | 160 CFM | 450 N | Chest & Back Panels |
| Reinforced Poly-Interlock | 175 - 190 GSM | 95 CFM | 680 N | Sleeves & Shoulders |
| 4-Way Stretch Poly-Spandex (88/12) | 180 - 200 GSM | 120 CFM | 590 N | Collar & Ergonomic Cuffs |
How our 3,000 m² Shenzhen production plant ensures zero defects, accurate color matching, and fast B2B turnaround times.
Using high-resolution Japanese digital printers and imported eco-friendly inks, we match Pantone colors to within 99.5% accuracy. Panels are printed onto high-release transfer paper before high-temperature calendar press bonding.
Manual fabric cutting introduces panel variance. Our automated laser cutting systems scan optical registration marks on the printed fabric, ensuring precise pattern edge alignment across all sizes from Youth 6Y to Adult 5XL.
Every single jersey passes five dedicated quality checkpoints: raw material inspection, print color check, post-cut panel match, seam tension test, and final dimensional measure before individual polybagging.
Tailored supply chain strategies for international Motocross gear brands, distributors, teamwear agents, and e-commerce platforms.
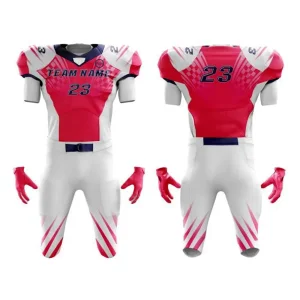
Traditional OEM factories demand 500+ units per colorway. GoldenLeaf Sports empowers growing brands and regional racing clubs with a flexible 10-piece Minimum Order Quantity (MOQ). Because every garment is digitally sublimated prior to cutting, individual rider names, numbers, and sponsor logos can be varied inside the same production run without setup surcharges.
We provide complete ODM, OEM, and private-label packaging support. Our fabrics and inks comply strictly with international environmental and chemical safety regulations, including REACH compliance in Europe and CPSIA standards in North America.
Pioneering sustainable smart textiles, bio-based synthetics, and automated pattern customization.
To meet strict corporate sustainability mandates in Europe and the Americas, our technical team is migrating base fabric lines to 100% post-consumer recycled ocean plastics and REPREVE® certified yarns without sacrificing tensile strength.
Integrating micro-encapsulated PCM treatments inside the yarn structures that absorb body heat when environmental temperatures spike, releasing stored heat when temperatures drop, stabilizing rider core body temperature.
Automating vector artwork scaling onto custom 3D body scans, ensuring perfect ergonomic alignment of graphics across all riders regardless of extreme body height or proportion variance.
Direct technical answers regarding OEM custom jersey manufacturing, minimums, color management, and global delivery.
GoldenLeaf Sports operates a dedicated 3,000 m² factory in Shenzhen with 14+ years of sublimated teamwear expertise. Over 80% of our 160 staff members are senior garment technicians. We engineer high-airflow fabrics (135–190 GSM), use imported non-fading inks, and maintain strict in-house QA/QC inspections without third-party outsourcing.
Our standard MOQ is just 10 pieces per design for custom sublimated jerseys, shorts, and pinnies. Because panels are printed individually before cutting, each player or team rider can have a different name, number, and size inside the same 10-piece order without incurring extra setup fees.
We utilize color-managed RIP software and calibrate printer profiles against the Pantone Matching System (PMS). Pre-production strike-off swatches are printed on actual target fabric and approved virtually or physically before initiating full roll printing.
Virtual 2D/3D mock-ups are completed within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production orders of 300 to 1,000 pieces are typically completed and ready for shipment in 12 to 18 working days post-sample sign-off.
Yes. We offer complete private-label OEM services, including heat-seal printed neck labels, woven collar labels, custom hang tags, barcodes, customized polybags, and branded master cartons.
Expand your brand's product lineup with our full suite of sublimated team apparel and activewear solutions.