



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our export-grade sublimated apparel manufactured under strict ISO9001 and OEKO-TEX Standard 100 protocols at our Shenzhen facility.
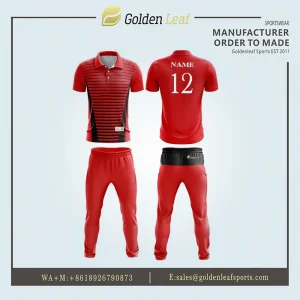
Analyzing the shift in global sportswear manufacturing toward high-wicking, digitally printed sublimation apparel across North America, Europe, and Oceania.
High demand for fast-turnaround, fully customized lacrosse, basketball, and scholastic athletic apparel. Buyers prioritize 100% polyester interlock fabrics with minimum 145–180 GSM weights, requiring vibrant pantone matching and zero minimal order quantities (MOQs) for player add-ons.
Stringent REACH regulation compliance, OEKO-TEX certification, and heavy emphasis on eco-friendly water-based sublimation inks. European club distributors mandate verified dye-fastness grade 4+ and recycled polyester (rPET) material matrices.
Severe structural stress on matchwear demands heavy-duty 4-way stretch poly-spandex (88/12) and reinforced double-stitched seams. Sublimation clarity must endure extreme physical abrasion and frequent UV exposure without color degradation.
Global athletic apparel procurement is transitioning rapidly from traditional screen-printed stock garments to 100% bespoke digital sublimation printing. Digital sublimation integrates design logos, player names, and numbers directly into the fabric molecular structure, eliminating graphic peeling while dramatically cutting inventory holding costs through on-demand manufacturing models.
Inside the physics of moisture-wicking polymers, cross-section yarn engineering, and high-temperature disperse dye sublimation.
Breathable sublimation T-shirts manufactured by GoldenLeaf Sports utilize specialized hydrophobic multi-filament polyester yarns. The capillary action engineered into the micro-mesh and bird-eye knit patterns channels perspiration rapidly away from the athlete's dermis to the outer fabric surface, speeding up evaporation by 42% compared to standard flat polyester.
Dye sublimation is a chemical process where imported eco-friendly disperse dyes transition directly from solid paper prints to gaseous states under controlled heat (200°C to 215°C) and mechanical pressure. The gaseous dye opens the synthetic polymer pore matrix, locking color deep inside the fiber structure upon cooling.
Operating a vertically integrated 3,000 m² facility in Longgang District, Shenzhen, engineered for scalable OEM and ODM export production.
| Operational Pillar | Factory Technical Capability | B2B Buyer Advantage |
|---|---|---|
| Factory Scale & Staffing | 3,000 m² modern workshop, 160+ full-time employees (80% senior apparel technicians). | Stable monthly capacity of 25,000+ custom pieces with low turnover operational stability. |
| Annual Export Volume | 300,000+ garments delivered annually across 30+ international markets. | Proven global export compliance, smooth customs documentation, and reliable shipping timelines. |
| In-House R&D & CAD | Dedicated pattern grading software, 24-48 hour digital mockup generation team. | Rapid prototyping; accurate regional fit adjustments (US, EU, Asian, & AU size charts). |
| Digital Printing Fleet | High-precision wide-format sublimation printers with automated RIP color correction. | Crisp photographic resolution prints with exact Pantone color matching for corporate logos. |
| Cutting & Assembly | Laser registration cutting paired with 4-needle 6-thread flatlock sewing lines. | Perfect panel-to-panel print alignment; ultra-durable smooth flat seams that prevent chafing. |
| Quality Assurance (QA/QC) | 5 dedicated full-time QC inspectors conducting 100% inline and pre-shipment inspections. | Zero defect tolerance; strict verification of sizing accuracy, stitch density, and print clarity. |
We provide complete private-label branding services. From custom woven neck labels, heat-transfer inner neck sizing marks, branded silicone hem grippers, to custom printed polybags and master cartons. Your brand identity is preserved with absolute fidelity from factory floor to retail shelves.
Understanding the modern need for lean inventory, our baseline MOQ starts at just 10 pieces per design. Because graphics are digitally sublimated prior to laser cutting, individual player names, numbers, and custom sizes can be seamlessly mixed within a single small batch without setup surcharges.
Every order follow strict standard operating procedures (SOPs) to guarantee zero defective units arrive at your distribution warehouse.
Receiving vector files (AI, PDF, EPS). In-house design team produces 2D high-res visual proofs within 24 to 48 hours for sign-off.
CAD pattern grading according to buyer’s target demographic (US Men’s/Women’s, Youth, European Fit) guaranteeing perfect garment proportions.
High-speed digital printing onto sublimation paper, followed by deep thermo-transfer onto raw white polyester base cloth at precise temperatures.
Automated optical camera laser cutters scan print registration marks to trim panel edges with micro-millimeter precision, sealing fabric edges.
Skilled seamstresses assemble garments using specialized flatlock, coverstitch, or overlock machines depending on stretch requirements.
Attachment of custom neck labels, care labels, size tags, swing tags, and silicone hem tapes according to customer tech packs.
Five full-time quality inspectors examine every garment for loose threads, color discrepancies, correct dimensions, and seam integrity.
Individual polybagging, barcode scanning, carton packing, and global shipping via DHL/FedEx Express, Air Cargo, or Sea Freight (DDP/FOB).
How GoldenLeaf Sports is pioneering waterless dyeing, recycled textiles, and automated manufacturing for the next generation of athletic apparel.
Traditional wet dyeing of cotton and synthetic fabrics consumes up to 100 liters of water per kilogram of cloth, generating vast quantities of chemical effluent. Dye sublimation is inherently a dry process. Water is used solely in closed-loop cooling circuits for machinery, cutting water waste by 98% throughout the production lifecycle.
Furthermore, our inks comply with strict European chemical safety standards, ensuring freedom from harmful heavy metals, azo dyes, and phthalates.
To support global brands in achieving their Scope 3 emission reduction targets, GoldenLeaf Sports offers performance yarns spun from 100% post-consumer recycled plastic bottles (rPET). These eco-polyesters deliver identical tensile strength, softness, and moisture-wicking metrics as virgin synthetic polymers while reducing carbon footprint by up to 45%.
Complete traceability documentation and GRS (Global Recycled Standard) certification reports are provided upon customer request.
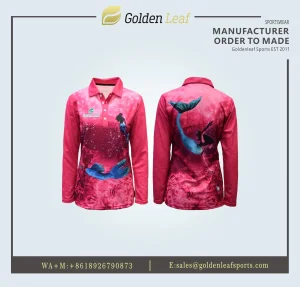
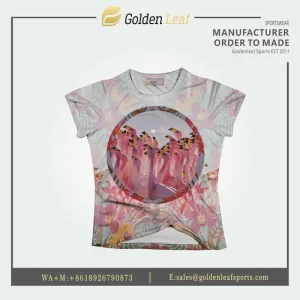
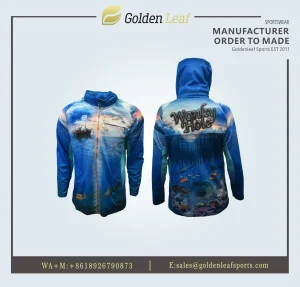
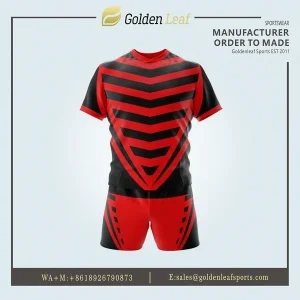
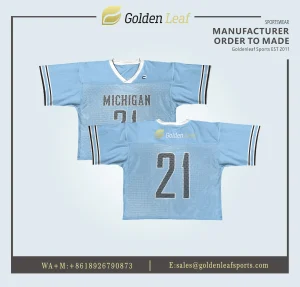
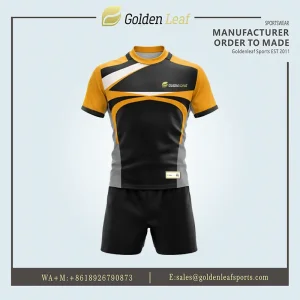
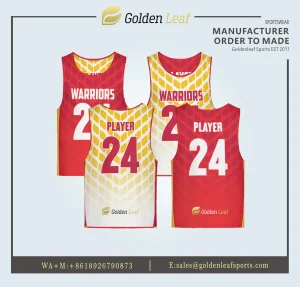
Explore additional OEM sublimated products built for extreme durability, ventilation, and style.
Comprehensive technical and commercial answers directly from GoldenLeaf Sports manufacturing directors.
Room 2309, Yingfeng Center, Jianxin Road South, Longgang District, Shenzhen, Guangdong, China · 518117