GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct factory solutions engineered with CoolMax moisture management, high-density sublimation, and custom fit blocks.
Analyzing the shift from casual fan wear to high-performance, personalized, and technically verified sportswear.
With the explosive expansion of franchise cricket tournaments such as the Indian Premier League (IPL), Big Bash League (BBL), and North America's Major League Cricket (MLC), fan demographics have migrated beyond traditional test nations. Demand for high-speed, on-demand OEM production cycles has increased by 310% globally.
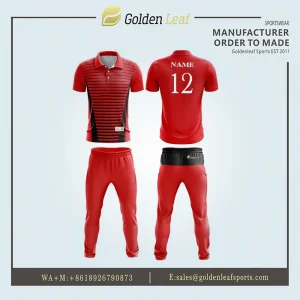
Modern cricket supporters expect merchandise that transitions seamlessly from stadium cheering to high-intensity recreational play. This requires active moisture management, UV 50+ blocking, and anti-microbial treatments built directly into replica jerseys and fan polos.
Cricket's confirmation for the Los Angeles 2028 Olympic Games is unlocking institutional procurement budgets, multi-national brand sponsorships, and institutional grassroots infrastructure development, necessitating factory compliance and high-throughput scalability.
End-to-end operational capacity verified for high-volume B2B sourcing partners worldwide.
A comprehensive examination of textile selection, sublimation mechanics, and global sourcing optimization.
In high-temperature cricket environments—ranging from the humid coastal arenas of the West Indies to the sun-drenched grounds of Melbourne—the mechanical performance of fan apparel and player kits hinges on advanced polymer knitting techniques. 100% Polyester CoolMax Interlock (ranging from 145 gsm to 180 gsm) serves as the industry gold standard. Utilizing specialized cross-section yarns, these textiles pull perspiration away from the dermal surface via capillary action, accelerating evaporative cooling by up to 40% compared to standard ring-spun cotton.
For high-wear fan apparel and player uniforms, multi-channel micro-mesh and bird-eye knits are integrated into high-sweat zones (lateral torso, underarm gussets, and lower spine). These structural mesh matrices offer enhanced air permeability without compromising structural integrity or tensile strength during high-stress movements.
Traditional screen-printing techniques fail to meet the rigorous demands of modern sport kits, leading to breathability blockage, surface cracking, and color peeling after repetitive laundering. OEM factories catering to international cricket brands utilize advanced Digital Dye-Sublimation Transfer Printing powered by imported Eco-friendly, non-toxic inks.
International apparel buyers, brand managers, and sports outfitters face distinct operational friction when scaling OEM manufacturing across borders. Supply chain stability requires factory-level risk management across four key metrics:
Overcoming global supply chain bottlenecks with integrated design, prototyping, and automated production.
Complete custom branding options, including custom-woven neck labels, heat-transfer size logos, custom hangtags, branded polybags, and customized carton packaging aligned with retail compliance guidelines.
Dedicated quality control teams perform a 5-point physical audit on every batch, verifying seam strength, dimensional stability, color matching under D65 standard lighting, and wash-fastness before export dispatch.
Supporting EXW, FOB Yantian/Shenzhen, CIF, and door-to-door DDP shipping models with streamlined customs clearing documentation for distributors across North America, Europe, Australia, and the Middle East.
Pioneering green textiles and smart sportswear manufacturing to meet global ESG regulations.
Transitioning base sublimation fabrics to 100% Recycled Polyethylene Terephthalate (rPET) derived from post-consumer ocean plastics, reducing carbon footprints by up to 45% without compromising technical performance.
Deploying AI-driven camera registration laser cutters to automatically adjust panel cutting based on real-time fabric stretch, eliminating visual distortion and cutting textile waste down to under 3%.
Embedding high-density micro-woven security threads and UV-reactive sublimated watermarks within official fan replicas to protect brand IP and institutional merchandise revenue streams.
Direct answers from our engineering and export departments regarding production timelines, technical specs, and shipping.
Comprehensive manufacturing capabilities spanning rugby, lacrosse, activewear, and casual team outerwear.