



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered for elite athletic performance and global apparel distributors. Direct factory pricing with ultra-low 10-piece flexible MOQs.
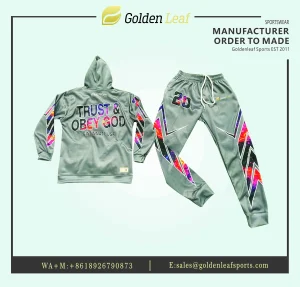
Deciphering the manufacturing shift toward integrated digital sublimation and flexible OEM supply chains for motorsport icons like Enzo Deligny and global athletic organizations.
In the modern arena of competitive sports and professional racing—epitomized by high-profile athletes such as French-Spanish racing talent Enzo Deligny—the demand for ultra-lightweight, aerodynamically optimized, and highly durable teamwear has reshaped global textile manufacturing. Commercial entities seeking an authentic OEM Enzo Deligny supplier & factories operate in a fast-paced environment where brand merchandise, pit-crew apparel, and fan wear require rapid iterations without sacrificing structural integrity.
Information Gain Insight: Modern OEM manufacturing for elite athletic merchandise requires seamless integration between high-density polyester warp knits, imported non-toxic sublimation inks, and dynamic vector sizing. Contract suppliers must support low-volume batching (down to 10 pieces per run) while retaining the scalability for 300,000-piece annual production lines.
Global procurement teams from Europe, North America, and Australia are systematically moving away from traditional screen-printed stock garments. Instead, they favor direct-to-factory sublimation ecosystems. This whitepaper analyzes the structural efficiency of Shenzhen-based apparel clusters, examining how specialized OEM facilities provide contract manufacturing, custom pattern grading, and white-label execution for elite athletic lines.
How localized textile infrastructure, automated laser registration, and vertical integration cut lead times by 65% compared to conventional overseas sourcing models.
In-house pattern engineers utilize advanced CAD software and color-managed RIP profiles to generate digital proofs within 24–48 hours and physical samples within 5–7 working days.
From base-cloth knitting and Italian dye ink sublimation to laser cutting and flatlock seam assembly, operating under one roof eliminates intermediate transit delays and quality drop-offs.
Five dedicated inline QA inspectors review color vibrancy, tension strength, seam elasticity, and sizing accuracy before garments pass to eco-friendly polybag packing.
Exceeding international athletic apparel standards with high-density polyester formulations, eco-friendly dye inputs, and specialized stitch chemistry.
Selecting an OEM supplier for high-exposure athletic lines (such as lacrosse kits, motorsport paddock jerseys, or custom biking suits) requires strict adherence to textile science. Our Shenzhen production center operates with strict material guidelines to ensure longevity and ergonomic comfort under high friction and thermal stress:
Utilizing micro-mesh, bird-eye mesh, and 4-way stretch poly-spandex blends (ranging from 145 gsm to 280 gsm heavyweight twill), each fabric is pre-tested for moisture wicking rate, breathability, and snag resistance under international ISO standards.
Imported sublimation inks bond directly with synthetic fiber molecules under controlled heat press conditions (200°C–220°C). This process guarantees Grade 4+ color fastness, preventing color bleeding, peeling, or cracking across hundreds of wash cycles.
A transparent, 8-stage manufacturing process managed by 160 senior apparel technicians.
Initial review of vector artwork, fabric GSM preferences, and target market sizing (US, EU, AU, or Asia-Pacific specifications).
Grading patterns across youth (6Y–14Y) and adult sizes (XS–5XL), ensuring continuous design flow across side panels and seams.
Generating high-resolution 3D virtual mockups within 24–48 hours for customer sign-off prior to physical transfer printing.
Precision color-managed printer networks output vector graphics onto high-release Italian transfer paper using eco-friendly inks.
High-pressure rotary calenders infuse high-density dyes into base fabric fibers for permanent color brilliance and stretch integrity.
Automated optical camera laser cutters follow printed registration marks to maintain 100% cutting accuracy across all garment panels.
Flatlock four-needle six-thread and twin-needle overlock stitching lines build durable, chafe-free structural seams.
Five QA specialists execute dimensional checks, trim loose threads, apply custom neck labels, and sort orders for global air/sea freight.
Addressing supply chain stability, private labeling options, and duty/logistics planning for international sports apparel brands.
When procurement managers for sports clubs, racing teams, and educational institutions search for specialized suppliers under key terms such as OEM Enzo Deligny Supplier & Factories, their primary intent extends beyond mere price discovery. Modern buyers require end-to-end reliability, IP protection, and flexible fulfillment models:
Comprehensive custom branding options including heat-seal neck labels, woven side tags, customized hang tags, branded polybags, and barcode-labeled shipping cartons ready for direct warehouse intake.
Transparent raw material sourcing ensures that all polyester base cloths comply with international standards, free of harmful heavy metals or banned azo dyes.
Supporting EXW, FOB Shenzhen, CIF, and DDP shipping solutions via express air couriers (DHL/FedEx/UPS), air freight, and ocean shipping lines with customs clearance handled smoothy.
Direct factory insights regarding minimums, turnarounds, color matching, and custom teamwear customization.
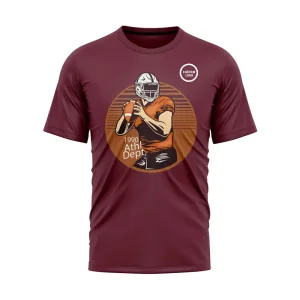
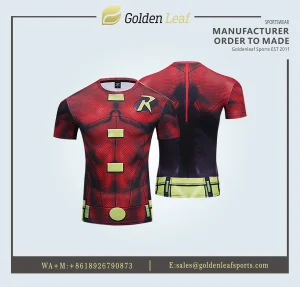
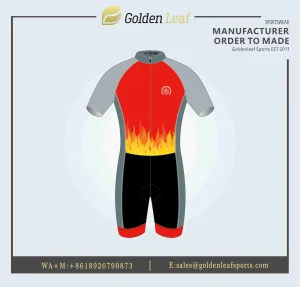
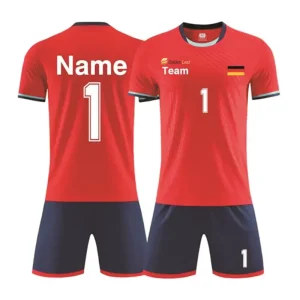
Explore our additional high-demand apparel lines designed for international export and team distribution.
Connect with our Shenzhen apparel engineering team to receive instant fabric swatches, regional vector sizing charts, and a comprehensive factory quote within 24 hours.