GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our core custom apparel categories engineered with advanced moisture management, high-density digital printing, and ergonomic sports patterning.
Strategic Insights for Brand Owners, Sports Leagues, Apparel Distributors, and Institutional Sourcing Directors
The global sports apparel landscape is undergoing a structural transition toward hyper-personalized, low-inventory, high-speed digital manufacturing. Specifically within the custom baseball jersey segment—ranging from traditional full-button down silhouettes to contemporary V-neck speed jerseys—global demand is driven by the expansion of collegiate leagues, amateur sports associations, high school athletic programs, and the booming lifestyle streetwear crossover market.
Historically, baseball shirt procurement was bogged down by high Minimum Order Quantities (MOQs), lengthy screen-printing lead times, and brittle vinyl heat-transfers that cracked under intensive washing. Modern institutional procurement now demands fully sublimated polyester matrices, ergonomic raglan or set-in sleeve patterns, fade-resistant Italian eco-inks, and rapid prototyping workflows.
As a leading OEM Personalized Baseball Shirts Supplier & Company operating out of China's premier apparel manufacturing hub in Shenzhen, GoldenLeaf Sports bridges the gap between high-end textile engineering and flexible agile supply chains. By vertically integrating digital pattern design, color-managed RIP software, automated laser panel cutting, and precision sewing lines under one roof, we empower global partners to achieve superior margin structures while reducing lead times to under 15 business days.
How Modern Infrastructure, Supply Chain Density, and Process Automation Drive Competitive Superiority
Situated in Guangdong Province, our factory gains direct access to world-class yarn spinners, specialized knitted mesh mills, customized button suppliers, and eco-friendly dye houses within a 50km radius. This hyper-local sourcing ecosystem drastically compresses pre-production lead times.
We leverage next-generation digital sublimators paired with automated flatbed heat presses operating at exact 200°C temperature profiles. This ensures deep molecular bonding of disperse dyes into polyester microfibers, creating fade-proof artwork without affecting fabric breathability.
Unlike third-party sourcing agents, our in-house 5-stage Quality Assurance team performs strict inline tensile, colorfastness (Grade 4+ standard), shrinkage, and dimensional tolerance checks on every batch prior to packing, minimizing return rates to near zero.
Custom-Engineered Polymers Designed for Maximum Durability, Thermal Control, and Athletic Mobility
Constructed specifically for full-button baseball jerseys, this heavyweight interlock fabric delivers structure, crisp drape, and exceptional abrasion resistance against dirt slides while maintaining soft skin-contact comfort.
Engineered with micro-perforations that create capillary action, drawing moisture rapidly away from the athlete's body to the garment surface for instantaneous evaporation during intense gameplay.
Integrating 8% to 12% elastane into high-tenacity polyester matrices allows complete range of motion for pitchers and batters, mitigating seam stress under repetitive rotational forces.
Utilizing OEKO-TEX® Standard 100 certified water-based inks imported from Japan and Italy. Free from heavy metals and harsh solvents, guaranteeing zero skin irritation and high vibrancy.
A Seamless 6-Stage Process Turning Digital Vector Artwork into Premium Finished Baseball Uniforms
Our graphic engineers translate customer logos, numbers, and sleeve stripes into precise 2D vectors, adjusting artwork automatically across all size scales (Youth 6Y to Men's 6XL) to maintain visual proportions.
High-resolution industrial plotters print vector graphics onto specialized high-release transfer paper. Color calibration profiles ensure 99% match with Pantone Matching System (PMS) codes.
Under uniform temperature and pressure, gaseous dyes penetrate deep into the polyester yarn. The print becomes an inseparable part of the fabric, ensuring zero cracking, peeling, or fading over time.
Optical registration cameras track print boundaries and guide high-speed lasers to slice panels with millimeter-level accuracy. Sealed edges prevent fraying during assembly.
Skilled seamstresses execute heavy-duty twin-needle cover stitching, reinforced buttonhole plackets, custom neck taping, and pro-style piped trim on full-button and two-button designs.
Every shirt is inspected for seam strength, loose threads, and player name/number accuracy. Individual poly-bagging with barcoded size labels prepares the stock for retail or league distribution.
Providing Specialized Patterning, Branding, and Production Frameworks for Global Buyers
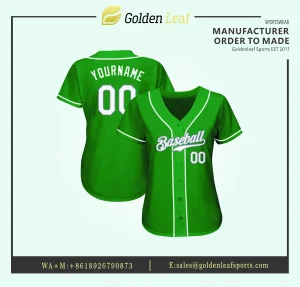
Designed to meet rigorous athletic federation standards. Our baseball jerseys feature traditional full-button plackets, double-stitched piping, low-friction flatlock seams, and extended back tails that stay securely tucked during play.
Modern fashion brands capitalize on baseball jersey silhouettes for casual streetwear collections. We offer contemporary oversized relaxed cuts, heavy mesh fabrics, custom woven neck labels, metal snap buttons, and embroidered chest patches.
Ideal for corporate team-building events, brand activations, and promotional giveaways. Cost-effective lightweight mesh options deliver maximum visual impact at competitive price points.
We provide seamless ODM/OEM fulfillment for Amazon, Shopify, and Etsy sports merchandise sellers seeking high-quality drop-ship or batch inventory with zero print defects.
How GoldenLeaf Sports Reduces Risk, Shortens Lead Times, and Ensures Brand Integrity
Sourcing athletic apparel internationally often introduces operational friction points: inconsistent sizing across regions, unexpected fabric shrinkage, print misregistration, and unreliable lead times. As an established OEM Personalized Baseball Shirts Supplier & Company, GoldenLeaf Sports solves these core vulnerabilities through systematic engineering controls:
Explore our complete product catalog designed for multi-sport organizations and private-label apparel distributors.
Technical and Logistics Clarifications for Procurement Managers and Brand Directors
Our standard MOQ is just 10 pieces per design. Because we utilize digital roll-to-roll sublimation printing, player names, numbers, and individual player sizing can vary across every single garment in a 10-piece order without incurring setup surcharges.
Digital vector proofing is completed within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production runs (300 to 1,000 units) ship in 12 to 18 working days following physical sample sign-off.
For classic full-button jerseys, we recommend our heavyweight 180-220 GSM Polyester Interlock or durable Dazzle Mesh. For lightweight speed jerseys and practice tees, we recommend our 150 GSM Bird-Eye Micro Mesh or 4-way stretch poly-spandex blends.
Yes. We offer complete private-label services including heat-transfer or woven neck labels, customized cardboard hangtags with barcodes, custom-printed polybags, and branded outer master cartons tailored to your retail specifications.
We log every client design with exact Pantone (PMS) color profiles and retain digital print files alongside physical fabric swatch master cuts. This guarantees identical color matching whether you order 10 pieces today or 5,000 pieces next season.
We support EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid) door-to-door terms via express air couriers (DHL/FedEx/UPS), air freight, and ocean shipping, serving clients across North America, Europe, Australia, and worldwide.