GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our precision-manufactured athletic gear, polo shirts, and customized sportswear built for global distributors, performance brands, and sports organizations.
In the contemporary B2B apparel landscape, corporate apparel buyers, sportswear brands, and institutional procurement teams are fundamentally shifting away from legacy decoration techniques. Traditional screen printing, direct-to-garment (DTG) overlays, and vinyl heat transfers present inherent structural flaws when applied to athletic polo shirts: surface cracking, breathability blockage, heavy hand-feel, and premature fading after commercial laundering cycles. As enterprise buyers demand higher longevity and superior thermoregulation, OEM polo shirts sublimation companies and exporters have become the primary growth engine for global sportswear supply chains.
Sublimation printing is not merely an aesthetic choice; it is a molecular chemical process. Under controlled thermal pressure (typically 200°C to 215°C), solid disperse dyes transition directly into a gaseous state without passing through a liquid phase. Concurrently, the synthetic polymer fibers of the polyester substrate expand, opening micro-pores that absorb the gaseous dye. As the fabric cools, the polymer structure locks the dye molecules permanently within the core filament. This yields an ultra-breathable, weightless garment where the graphic becomes an integral part of the fabric matrix rather than an additive surface layer.
Key Insight for OEM Procurement Directors: Digital dye-sublimation eliminates minimum-per-color setup charges, allows unlimited color variations within a single garment, and guarantees absolute zero thermal trap—preserving 100% of the underlying moisture-wicking capillary network of the synthetic fibers.
Understanding fiber cross-sections, GSM density, and elastomeric blends for technical sublimated polo manufacturing.
Engineered for corporate and golf polos (150 - 180 GSM). Features a 3D waffle structure on the exterior for classic aesthetics, combined with a smooth hydrophilic interior face for rapid moisture dispersal.
Utilizing 88% High-Tenacity Polyester and 12% Elastane (160 - 200 GSM). Delivers 360-degree dynamic stretch response, dynamic recovery, and zero motion resistance for elite athletic polo lines.
Ultra-lightweight open-cell matrix (130 - 150 GSM) engineered with micro-apertures. Maximum airflow efficiency for tropical climates, active workwear, and high-perspiration sports environments.
| Fabric Type | GSM Range | Composition | Hydrophilic Rate | Recommended Polo Application |
|---|---|---|---|---|
| Micro-Piqué Pro | 160 - 180 gsm | 100% Recycled Polyester | < 1.5 seconds | Corporate Uniforms, Golf Tournaments |
| Pro-Flex Spandex | 170 - 190 gsm | 88% Poly / 12% Spandex | < 1.0 seconds | Elite Tennis, Motorsport & Teamwear |
| Air-Flow Mesh | 135 - 150 gsm | 100% Micro-Polyester | < 0.8 seconds | Outdoor Workwear, Tropical Sports |
| Heavy-Twill Polo Knit | 200 - 220 gsm | 95% Poly / 5% Elastane | < 2.0 seconds | Rugby Polos, Premium Executive Wear |
Achieving international brand standards in sublimated polo production requires rigorous control over color reproduction, ink chemical purity, and registration precision. Leading Chinese OEM manufacturers like GoldenLeaf Sports employ integrated digital workflows that eliminate human error at each critical milestone.
Utilizing X-Rite Spectrophotometers and Ergosoft RIP software to ensure Pantone TCX / PMS color matching within an industry-leading Delta E threshold under 1.0.
Imported Italian (Kian) and Japanese (Epson UltraChrome DS) water-based disperse inks. Zero heavy metals, non-toxic, OEKO-TEX Eco Passport certified for skin safety.
Automated optical camera lasers scan printed registration dots to cut vector panel outlines with millimeter accuracy, maintaining perfect stripe and seam alignment.
The Guangdong-Shenzhen textile manufacturing cluster represents the most fully integrated apparel ecosystem in the world. For enterprise B2B buyers seeking OEM polo shirt sublimation exporters, partnering with a digitally transformed Chinese facility delivers distinct strategic advantages over alternative regional hubs:
Within a 30-minute radius of our Shenzhen facility, raw performance textiles, custom collar knits, branded buttons, anti-static threads, and eco-friendly poly-packaging are directly sourced—drastically reducing raw material lead times.
Real-time shop floor tracking allows seamless switching between high-volume corporate uniform orders (10,000+ units) and low-MOQ athletic team re-orders (10-50 units) without bottlenecking output capacity.
Digital dye sublimation requires zero water bath washing post-transfer, reducing liquid effluent to absolute zero and providing automated compliance with global ESG environmental standards.
Exporting performance polo shirts across North America, Europe, Australia, and the Middle East mandates compliance with stringent international quality standards, chemical safety protocols, and trade logistics frameworks.
All sublimated polo fabric blends comply with OEKO-TEX® Standard 100 (Class I/II), EU REACH Regulations, and ISO 9001 quality management procedures. Lab tests confirm Color Fastness to Washing (ISO 105-C06) at Grade 4.5+.
Complete OEM customization including high-density woven neck tags, tagless heat-seal care labels, custom branded placket buttons, laser-engraved zipper pulls, and barcoded retail polybags.
Flexible international shipping via Express courier (DHL/FedEx/UPS: 3-5 days), Air Freight (7-10 days), or Ocean/Rail DDP (20-35 days) with complete tariff classification (HS Code 6105.20) support.
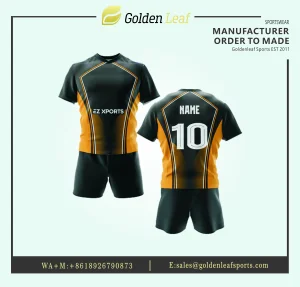
Browse our broader range of sublimated team wear, compression apparel, bottoms, and custom sportswear solutions.