



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our export-ready custom sportswear catalog manufactured with eco-friendly Italian sublimation inks and high-wicking polyester knits.
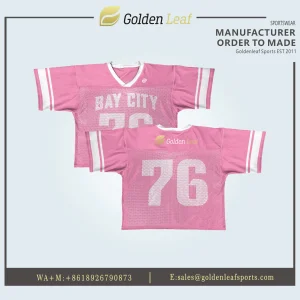
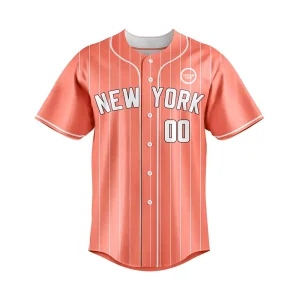
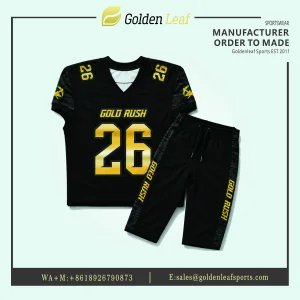
The global sportswear ecosystem has experienced a profound structural evolution over the past decade. Traditional apparel manufacturing—historically dominated by screen printing, vinyl heat transfers, and static stock inventory models—is no longer sufficient to meet the fast-moving requirements of contemporary athletic leagues, school programs, and international sports brands. Modern B2B athletic buyers now demand hyper-customized, high-durability, and ergonomically engineered performance apparel delivered on accelerated timelines.
At the center of this transformation lies digital dye-sublimation printing technology. When looking for premier OEM sublimation football jersey design companies & factory partners, global brands prioritize suppliers capable of merging chemical textile engineering with Industry 4.0 production agility. Dye-sublimation is not merely a surface decoration technique; it is a molecular bonding process where heat-sensitive disperse dyes vaporize into gas under precise heat and pressure, penetrating deep into polyester microfibers before reverting to a solid state. The resulting garment retains 100% of its native fabric breathability, offers zero surface friction, and completely eliminates cracking, peeling, or color fading across hundreds of high-intensity match cycles.
Unlike screen printing, which deposits a thick layer of plastisol ink on top of the fabric (blocking mesh pores and adding unnecessary weight), dye-sublimation integrates pigment directly into the polymer chain. This technical distinction maintains a constant Fabric Surface Porosity (FSP), reducing thermal strain on athletes during competitive matches.
As elite sports performance demands more from modern textiles, OEM design studios and factory tech teams are introducing sophisticated visual and structural innovations into custom football uniform design:
Utilizing differential mesh knits across high-heat zones (underarms, spine, side flanks). Sublimation artwork seamlessly flows over multi-panel vector cuts without alignment distortion.
Integration of RIP (Raster Image Processor) software mapped to Pantone TCX (Textile Cotton/Extended) color standards, ensuring 99.8% accurate reproduction from digital RGB/CMYK screens to physical polyester fabric.
The market demand for sustainable sportswear has driven factories to adopt GRS-certified (Global Recycled Standard) recycled polyester (rPET) derived from post-consumer plastic bottles paired with water-based non-toxic inks.
Sourcing directors for international sports brands, regional distributors, and professional club equipment managers evaluate OEM factories through a multi-dimensional risk-mitigation framework. B2B purchasing decisions are rarely based on unit cost alone; they are dictated by supply chain reliability, quality consistency, and operational transparency.
China remains the powerhouse of custom sportswear manufacturing due to its unmatched supply chain integration, raw material availability, and technological advancement in textile machinery. Nowhere is this more evident than in Shenzhen’s advanced manufacturing district, where GoldenLeaf Sports (ShenZhen) Co., Ltd. has operated as an industry leader since 2011.
The modern Chinese OEM factory utilizes an end-to-end digital workflow that connects vector artwork creation directly to automated cutting tables. This eliminates manual pattern drift and ensures precise sizing across youth (6Y-14Y) and adult sizes up to 5XL.
Inside an Industry 4.0 OEM Sportswear Facility
Reviewing sport specifications, GSM weight options, collar profiles, and target delivery windows with dedicated account managers.
Digitally grading base block patterns into regional size charts (US, EU, AU sizing standards) to ensure consistent garment ergonomics.
In-house design team generates high-resolution 3D virtual mock-ups within 24–48 hours, detailing sponsor layouts and color codes.
Printing sublimation artwork onto high-release transfer paper using high-speed industrial plotters and eco-friendly imported dyes.
Continuous-roll calender heat presses transfer pigment into raw fabric panels at 200°C–220°C under calibrated pressure.
Automated camera-guided laser cutters slice printed panels with millimeter accuracy, sealing edges against frayed threads.
Skilled sewing teams assemble garments using heavy-duty 4-needle 6-thread flatlock and twin-needle overlock stitching lines.
Five dedicated quality inspectors conduct dimensional verification, seam strength testing, color-fastness audits, and polybag packaging.
The application of custom sublimated athletic apparel extends across diverse sports codes, climate conditions, and commercial markets around the globe:
High demand for American Football kits, Youth Lacrosse jerseys, and Baseball jerseys. Key sourcing requirements center on heavy-weight mesh body fabrics (for pad coverage), extended body drops, reinforced double-layer shoulders, and rapid turnaround for seasonal high school and collegiate club leagues.
Dominated by Soccer club kits, Rugby union teamwear, and running apparel. Focus is placed on slim-fit performance blocks, eco-friendly rPET textiles compliance (OEKO-TEX Standard 100), lightweight micro-interlock fabric, and complex gradient club branding.
Rugby League, AFL (Australian Rules Football), Netball, and Touch Football dominate. Gear must feature high UV protection (UPF 50+ rating), extreme tensile tear-resistance for contact sports, and moisture-wicking capillary knits suited for hot, humid match environments.
See how our OEM sublimated team kits perform in real-world tournament conditions across major export markets.
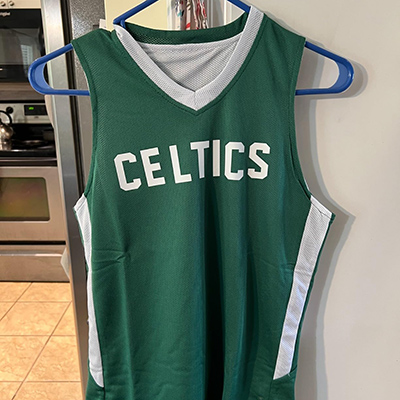
“We ordered these for our beginning youth basketball league. The quality is amazing — washes and wears well. We were able to have both sides printed easily and without issues. We would definitely order these again.”
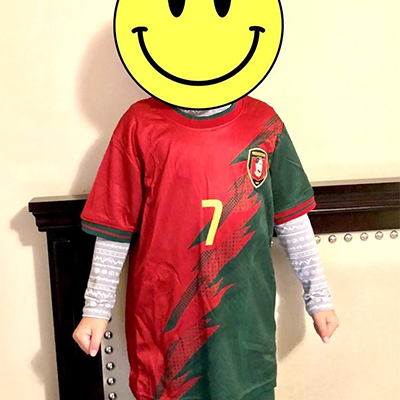
“I bought this for my son and he loved it. It is comfortable and true to sizing — definitely worth what I paid, especially for the quality. The colours are nice.”
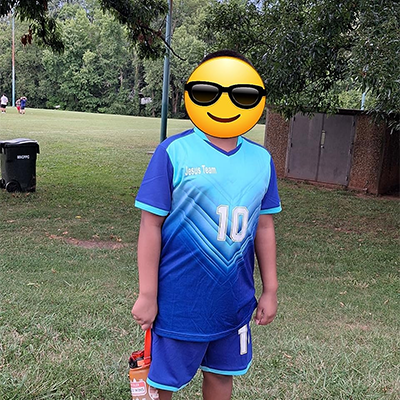
“Bought for my son who loves soccer and wanted a custom-made uniform. I really like the material because it is light and keeps the body fresh while playing. It took more than a week to arrive, but it was worth it.”
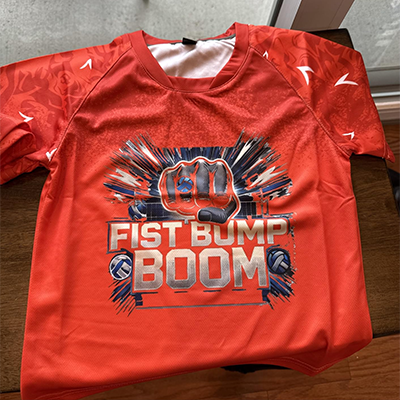
“Great orange colour and the design came out great. The shirt quality is nice — very cute volleyball shirt for those looking for team jerseys. Shipping was quick.”
Expand your product offerings with our full range of custom team kits, technical outerwear, and event accessories.
Expert answers regarding dye-sublimation mechanics, minimum order quantities, turnarounds, and custom branding support.
Partner with Shenzhen's premier sports apparel OEM factory. Get free 3D design mock-ups, factory-direct pricing, and rapid sample turnarounds within 24 hours.