GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct factory customized activewear, team kits, and performance sublimation apparel produced with eco-friendly digital dye technology.
An authoritative analysis of technical transitions, market valuation trajectories, and modern apparel chemistry.
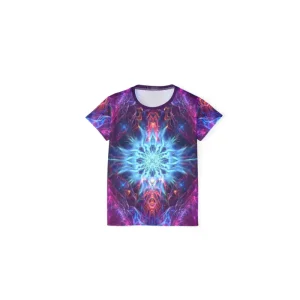
The global textile manufacturing sector has undergone a profound paradigm shift. Traditional direct-to-garment (DTG) and screen printing methodologies are rapidly giving way to high-precision digital dye-sublimation printing for short-sleeve T-shirts. Driven by rising international demand for hyper-personalized activewear, corporate event apparel, and high-performance athletic uniforms, modern OEM sublimation factories must integrate chemical expertise with digital speed.
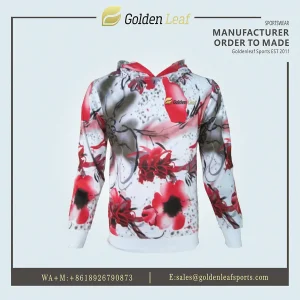
Unlike conventional pigment printing—where ink forms a physical layer atop the fabric face, restricting airflow and inducing cracking over repeated wash cycles—sublimation dye technology relies on molecular phase changes. Under precise thermal conditions (typically 190°C to 215°C) and calibrated mechanical pressure, solid disperse dyes transform directly into a gas without entering a liquid state. The gas penetrates the expanded pores of synthetic polymer fibers (primarily polyethylene terephthalate, or PET). Upon cooling, the polymer pores close, trapping the dye inside the fiber matrix permanently.
Dye particles reside inside the polymer core rather than surface layers, maintaining maximum breathability, lightweight properties, and friction-free skin contact critical for pro athletes.
Digital RIP (Raster Image Processor) software drives piezoelectric print heads to render millions of hues, photorealistic gradients, and intricate vector graphics without extra setup fees per color.
Boasting ISO 105-C06 Grade 4.5+ laundering fastness and Grade 4+ light fastness, sublimated T-shirts remain vibrant through extreme UV exposure and commercial laundering.
Demystifying the strategic, technical, and compliance requirements of Tier-1 B2B apparel buyers across international jurisdictions.
Intent mining across international B2B buyer queries indicates that corporate procurement teams, sport brand product directors, and private-label distributors no longer select OEM factories based solely on cut-and-sew unit prices. Modern procurement frameworks prioritize total cost of ownership (TCO), material sustainability certifications, structural supply chain resilience, and rapid prototype turnarounds.
| Evaluation Metric | OEM Digital Dye-Sublimation | Traditional Screen Printing | Direct-to-Garment (DTG) |
|---|---|---|---|
| Setup Cost / MOQs | Zero screen setup fees; Highly flexible MOQs (10-50 pcs/design). | High screen & film costs; Requires large volume (500+ pcs). | No setup fee; Cost-effective for 1-5 pcs, expensive at scale. |
| Fabric Compatibility | 100% Polyester & Poly-blend synthetics (Micro-mesh, Interlock). | 100% Cotton, Tri-blends, Synthetics (Requires diverse inks). | Primarily 100% Cotton or high-cotton content fabrics. |
| Hand-Feel & Breathability | 100% Seamless; Zero ink film feel; Fully breathable. | Rubberized / Plasticized layer; Impairs fabric ventilation. | Soft hand-feel on cotton; Can feel stiff with heavy pre-treatments. |
| Durability & Fastness | Lifetime durability; Will never crack, peel, or flake off. | Prone to cracking/peeling after 20-50 wash cycles. | Gradual ink fading after multiple domestic machine washes. |
| Customization Agility | Individual names, numbers, and sponsor logos in one pass. | Expensive; Requires separate screens for each custom variable. | Moderate agility; Slow print output per piece. |
Four structural transformations reshaping activewear manufacturing, fabric technology, and digital decoration.
Environmental regulations and corporate ESG mandates are accelerating the shift toward 100% Recycled Polyester sourced from post-consumer plastic bottles. Advanced OEM factories utilize GRS-certified (Global Recycled Standard) yarn that mirrors virgin polyester in tensile strength and dye affinity.
Modern short-sleeve sublimation T-shirts integrate functional textile treatments such as anti-microbial silver-ion coatings, phase-change cooling fabrics, and UPF 50+ UV-blocking yarns without interfering with the dye-sublimation ink transfer process.
Leading factories are fusing full-body dye sublimation with secondary processes—such as 3D high-density silicone heat transfers, reflective vinyl overlays, and metallic foil accents—creating high-value tactile contrast on performance garments.
AI-driven computerized vector nesting software optimizes fabric utilization yields beyond 92%, while high-speed vision-guided laser cutting systems automatically compensate for micro-stretches in printed paper rolls.
Inside the specialized industrial clusters of Shenzhen and Guangdong: How smart automation drives unmatched speed, quality, and scale.
China’s Greater Bay Area—specifically the manufacturing hubs of Shenzhen and Dongguan—remains the world’s most advanced ecosystem for digital apparel sublimation. Unlike fragmented supply chains where printing, cutting, stitching, and packaging are outsourced across multiple external vendors, Tier-1 Chinese Industry 4.0 factories consolidate these specialized units within unified, vertically integrated campuses.
Immediate proximity to world-class synthetic fabric mills, specialized dye chemical synthesizers, and precision trim suppliers cuts raw material procurement lead times down to under 48 hours.
Industrial multi-head digital printers (utilizing Epson PrecisionCore or Kyocera printheads) run 24/7 with continuous bulk ink feed systems, achieving daily outputs exceeding 15,000 sub-printed panels.
In-house testing laboratories evaluate tensile strength, seam slippage, color crocking (AATCC 8), and dimensional stability after washing, guaranteeing international compliance (Oeko-Tex Standard 100, REACH).
Tailored manufacturing specs designed to meet diverse operational environments and end-user demands globally.
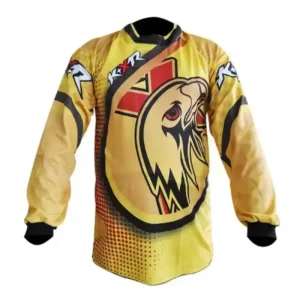
Technical Spec: 110-130 GSM Ultra-lightweight Micro-mesh (100% Poly). Moisture Wicking finish, flatlock anti-chafing seams, reflective rear heat-transfer tabs, high-contrast sublimation graphics visible under harsh sunlight.
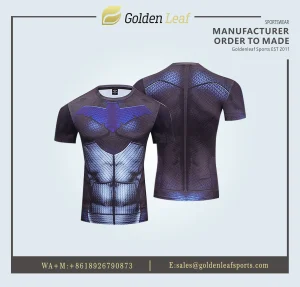
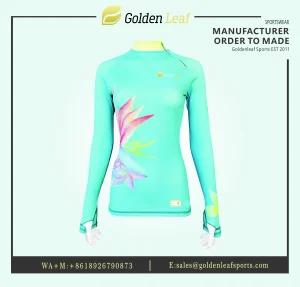
Technical Spec: 160-180 GSM Interlock Poly-Spandex Blend (92/8). 4-way elastic recovery, structured stand-up collar options, edge-to-edge sublimation print covering complex vector gaming crests and multiple sponsor logos.
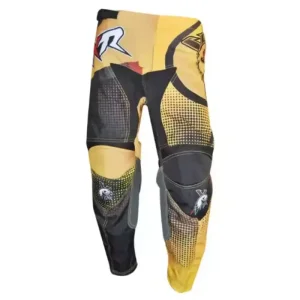
Technical Spec: 140-150 GSM Honeycomb Birdseye Polyester. Breathable structure, quick-drying performance, fade-resistant vibrant branded pantone colors, pill-resistant finish engineered for 50+ industrial laundry washes.
Expert answers addressing key engineering, ordering, and logistics inquiries from international B2B purchasers.
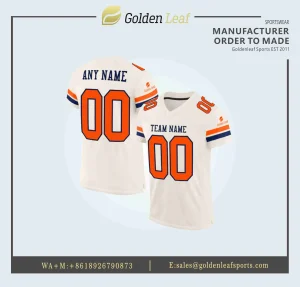
Our standard manufacturing MOQ is 10 pieces per design run. Because dye-sublimation transfers graphics from printed paper onto cut panels prior to stitching, we can accommodate variable player names, squad numbers, and individual garment sizes within that 10-piece run at zero artwork surcharge.
Dye-sublimation inks require synthetic polymer chains to bond. Optimum visual saturation, Delta-E accuracy, and wash durability are achieved using 100% Polyester (Interlock, Micro-mesh, or Birdseye knit) or high-polyester stretch blends (e.g., 88% Polyester / 12% Elastane). Natural fibers such as 100% Cotton are unsuited for sublimation dye chemistry.
We utilize standardized X-Rite spectrophotometers combined with specialized Ergosoft RIP software. All digital artwork files are color-calibrated against dedicated media profile cards created specifically for our ink-and-fabric combinations, maintaining color variance within a strict target of Delta-E < 1.5.
Digital 3D virtual mock-ups are rendered within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production runs (300 to 5,000 units) ship in 12 to 18 business days after sample sign-off, supported by express air freight or ocean freight logistics.
Yes. We offer complete OEM/ODM customization services. This includes sublimated neck labels, woven brand tags, silicone care labels, custom branded hangtags, barcode stickers, and printed eco-friendly polybags ready for direct distribution.
Explore our specialized sublimated athletic wear, custom accessories, and multi-sport tournament kit offerings.