GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our flagship OEM/ODM custom sublimated gear manufactured inside GoldenLeaf Sports' 3,000 m² Shenzhen production facility.
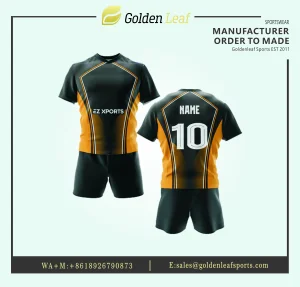
An In-Depth Technical Whitepaper on Modern Athletic Apparel Engineering, Global Sourcing Dynamics, and Sublimation Technologies.
The cricket teamwear landscape has undergone a monumental structural shift over the past decade. Traditionally dominated by heavy cotton-blend weaves and panel-stitched embroideries—which added unwanted tare weight and caused severe chafing during multi-day Test matches—the contemporary cricket uniform market demands high-performance, ultra-lightweight polyester synthetics. Modern international formats like T20, One Day Internationals (ODIs), and fast-growing franchise leagues (e.g., IPL, Major League Cricket in the US, Big Bash) require vibrant, intricate gradient color schemes, complex sponsor placement matrices, and personalized player numbers. Original Equipment Manufacturers (OEMs) and factories are now assessed on their capability to execute full-body digital dye sublimation without compromising fabric breathability or structural durability under intense sunlight and high humidity.
Located in Longgang District, Shenzhen, GoldenLeaf Sports operates at the center of the world's most advanced textile and apparel manufacturing cluster. Integrating digital pattern design, automated laser cutting, heat press transfer at precise thermal thresholds (210°C), and dedicated flatlock stitching lines under one 3,000 m² campus, our facility eliminates sub-contracting latency. With over 160 skilled technicians—80% of whom possess senior apparel engineering expertise—we bridge the gap between high-volume commercial production and agile, low-MOQ custom roster demands for global sports brands, regional distributors, and professional cricket clubs.
Unlike traditional screen printing or vinyl transfers that apply a plastic film layer over top of the textile surface (blocking fabric pores and trapping heat), modern sublimation heat transfer gasifies Eco-friendly disperse dyes directly into the core of the polyester micro-fibers. This ensures 100% surface porosity retention, zero weight addition, and permanent color fastness against UV radiation and sweat abrasion.
Mapping the specialized sourcing needs of B2B athletic apparel buyers across major cricket-playing geographic sectors.
| Buyer Segment | Primary Sourcing Intent | Critical Technical Pain Points | GoldenLeaf OEM Factory Solution |
|---|---|---|---|
| International Brand Licensees | High-volume seasonal stock, strict color consistency across production lots, REACH compliance. | Color fading, batch-to-batch shade variation, long factory lead times (90+ days). | RIP software digital color management (Delta-E < 1.0), automated Swiss laser cutting, guaranteed 12–18 day turnaround. |
| Regional Sports Wholesalers | Low MOQ replenishment, rapid re-order capability for winning teams, custom labeling. | High MOQ barriers from tier-1 factories, hidden setup fees for short runs. | Flex 10-piece MOQ per design, free in-house 3D digital mockups within 24–48 hours, turnkey white-label neck tag printing. |
| Academy & School League Buyers | Durable materials withstand high wash cycles, multi-age sizing (Youth 6Y to Adult 5XL). | Inconsistent sizing standards across continents, poor seam elasticity leading to tearing. | Regionally calibrated pattern blocks (US, EU, AU, UK standard), reinforced twin-needle flatlock seam sewing. |
| Professional Franchise Clubs | Peak moisture management, ergonomic anatomical cut, lightweight anti-bacterial mesh. | Heat buildup during matches exceeding 40°C, skin chafing from rigid collars. | Custom knitted rib collars, zonal ventilation mapping using 145 GSM bird-eye moisture-wicking poly-spandex. |
High emphasis on traditional creams and whites for multi-day matches, paired with high-SPF (UPF 50+) sun-protection treated fabrics. White-label suppliers must meet stringent UK and Australian anti-pilling and color-fastness standards.
Explosive growth driven by Major League Cricket (MLC) and local T20 tournaments requires hyper-bold custom sublimated graphic aesthetics, quick turnarounds for roster updates, and lightweight fan-replica apparel lines.
Demand focuses on ultra-breathable open-mesh fabrics (140-150 GSM) capable of operating under extreme ambient field temperatures (40°C–45°C), paired with high-durability reinforced elastic waistbands for trousers.
How GoldenLeaf Sports selects, engineers, and tests specialized performance synthetic fabrics for elite cricket team shirts.
A cricket match can extend from several hours (T20 format) up to five days (Test cricket). The selection of Grams per Square Meter (GSM) directly governs player thermal comfort and garment longevity:
Our advanced cricket jersey fabrics undergo a permanent hydrophilic finish treatment during the yarn dyeing stage. Moisture wicking functions through capillary channel action:
Capillary Action Mechanism: Liquid perspiration is rapidly absorbed from the inner skin layer and dispersed across a 3x wider outer surface area. Ambient airflow speeds evaporation by 40% compared to standard untreated polyesters, maintaining core body temperatures under high sun exposure.
Furthermore, integrated silver-ion anti-bacterial treatments prevent microbial degradation and eliminate sweat-induced odors during multi-day tournament use.
Inside GoldenLeaf Sports' 8-Stage Precision Garment Manufacturing Process.
Vectorized pattern construction tailored to multi-regional sizing parameters (US, EU, UK, AU). Each size block guarantees zero graphics distortion when scaled up or down.
High-precision industrial printheads deploy Eco-friendly imported disperse sublimation inks. Calibrated against Pantone Matching System (PMS) palettes for 99.8% color fidelity.
Dye transfer onto white polyester rolls executed under strictly controlled parameters (210°C thermal pressure for 30 seconds), bonding color permanently into micro-polyester filaments.
CCD camera optical registration scanners trace printed alignment marks, laser-cutting panel edges with zero fraying and high dimensional accuracy (±1mm tolerance).
High-tensile polyester sewing threads applied via 4-needle 6-thread flatlock machinery. Prevents inner-thigh and under-arm friction points for maximum athlete comfort.
Integration of soft heat-transfer neck labels, woven brand waist tags, customized barcode hangtags, and OEM branded polybag packaging per client specification.
Five dedicated quality assurance inspectors check seam tension, color vibrancy, print alignment, exact dimensional tolerances, and player name/number accuracy.
Sorted by team rosters, packed in heavy-duty moisture-sealed cartons, and shipped worldwide via DHL/FedEx Express, Air Cargo, or DDP Sea Freight options.
Meeting international athletic apparel regulatory frameworks and environmental responsibility guidelines.
All raw polyester yarns and imported sublimation inks utilized in our Shenzhen facility are certified free from harmful levels of toxic substances, azo dyes, heavy metals, and formaldehydes, ensuring safe skin contact under heavy perspiration conditions.
Our factory operates under ISO 9001:2015 certified production workflows. From raw fabric roll incoming inspections (AQL 2.5 standards) to final carton packing auditing, every stage carries documented sign-offs by qualified apparel engineers.
Supporting modern corporate environmental commitments, GoldenLeaf Sports offers optional 100% recycled polyester yarns produced from post-consumer plastic bottles, reducing energy consumption by 45% and carbon emissions by 52% per batch.
Anticipating the technological integration of smart fabrics and advanced biometric athletic uniforms.
As professional cricket leagues embrace real-time biomechanical player monitoring (tracking fast bowler workload, acceleration vectors, and heart rate variability), teamwear OEM factories must design integrated micro-pockets and flexible conductive yarn pathways. GoldenLeaf Sports is actively developing heat-sealed inner vest pouches designed to house ultra-light GPS and IMU tracking units without impeding player movement or creating skin pressure points.
Future short-format cricket kits will incorporate dynamic non-Newtonian fluid polymers directly into high-impact zones (such as thigh guard pockets and chest panels). These light, flexible foam layers remain pliable during normal running, but instantly stiffen upon high-velocity ball impact to absorb kinetic energy—revolutionizing modern batsman protection.
Direct factory answers to common procurement questions asked by commercial buyers, brands, and team outfitters.
Our baseline factory MOQ is 10 pieces per design for fully sublimated cricket shirts and uniforms. Because every fabric panel is digitally printed prior to automated laser cutting, each garment inside your 10-piece order can feature individual player names, squad numbers, and specific size gradings (from Youth 6Y to Adult 5XL) at no additional setup charge.
We utilize digital spectrophotometers paired with specialized Raster Image Processor (RIP) color-management software to match specified Pantone Solid Coated (PMS) reference codes. Prior to mass production, we generate a high-density printed fabric swatch grid (strike-off) and provide physical or digital high-resolution photography proofing to guarantee Delta-E color variance remains strictly under 1.0.
Initial 3D digital vector mockups are delivered within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Standard bulk manufacturing runs (300 to 1,000 pieces) ship within 12 to 18 working days following final artwork and size matrix approval. Urgent rush order capabilities are available upon consultation.
For high ambient temperature environments (such as Australian summer leagues or Middle Eastern desert tournaments), we recommend a hybrid panel construction: 145 GSM open bird-eye micro-mesh on underarm and rear back panels for maximal heat expulsion, combined with 160 GSM cool-dry interlock polyester across front chest panels for high print contrast and snag protection.
Yes. As a comprehensive ODM/OEM partner, we offer complete private-label branding services: customized heat-seal transfer inner neck labels, woven side seam labels, custom cardboard hangtags with barcodes, printed branded polybags, and outer carton routing labels tailored for direct distribution to your end-client or warehouse.
Complete your custom club collection with our full suite of athletic teamwear, tracksuits, hoodies, and training gear.