GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Direct Factory Digital Sublimation & Engineered Power Apparel Solutions for Global OEM/ODM Procurement
An Industry Whitepaper on Sublimation Chemistry, Dynamic Thermal Regulation, and Industrial-Grade Custom Manufacturing Excellence
In modern athletic engineering and commercial supply chains, the demand for high-output thermal management and structural polymer durability has transformed raw material processing. As a premier wholesale custom Goldenleaf power solutions manufacturer & factory, operating out of Shenzhen, China, GoldenLeaf Sports (ShenZhen) Co., Ltd. has pioneered an integrated ecosystem that bridges micro-denier textile physics with industrial power solutions for global sports brands, corporate fleets, and institutional athletic programs.
Established in 2011, our 3,000 m² smart manufacturing campus leverages Industry 4.0 IoT-enabled printing machinery, digital dye sublimation chemistry, and automated panel registration systems. By maintaining 100% in-house production control—spanning pattern grading, raster image processing (RIP) color calibration, heat-press thermal bonding, high-precision laser trimming, and rigorous 5-stage quality assurance—we eliminate third-party latency and guarantee seamless batch-to-batch repeatability for international distributors across North America, Europe, and Oceania.
Direct-from-factory pricing structures eliminate broker markups, while dynamic 10-piece MOQs unlock high-margin micro-batch distribution for private labels.
Every piece of technical sportswear and custom uniform set complies with OEKO-TEX Standard 100 and ISO9001:2015 quality control protocols.
Utilizing high-grade 100% polyester interlock, 4-way stretch poly-spandex (88/12), and open bird-eye mesh for optimal moisture evaporation.
How Modern Automation and In-House Production Verticalization Secure Global B2B Supply Chains
In the wake of global supply chain volatility, enterprise buyers require more than low-cost manufacturing; they require predictable throughput, digital transparency, and strict adherence to technical specifications. The GoldenLeaf Shenzhen facility represents the vanguard of China's Factory 4.0 transition. By integrating automated resource planning with physical manufacturing execution systems, we ensure that every order—whether a 10-unit custom club re-order or a 50,000-unit retail rollout—moves through an optimized workflow.
Unlike conventional screen printing or vinyl transfers which apply a surface layer prone to cracking and thermal traps, GoldenLeaf’s digital sublimation process forces eco-friendly, imported inks directly into the polymer lattice under controlled temperature (200°C) and pressure. This solid-to-gas phase transition embeds graphic pigment permanently into the filament, retaining 100% of the fabric’s original breathability and structural elasticity. Colour fastness tests routinely achieve Grade 4+ under international ISO/AATCC wash standards.
Hand-cutting sublimated panels inevitably introduces geometric distortion across size runs. Our factory utilizes optical camera-guided laser cutting beds that scan printed alignment targets in real-time. The system automatically adjusts for subtle fabric stretch during heat transfer, guaranteeing zero-drift pattern cutting for intricate multi-panel jerseys, lacrosse pinnies, and rugby wear.
By retaining an inventory of over 50 technical performance fabrics—ranging from 145 gsm ultra-light mesh to 280 gsm heavy-duty rugby twill—our facility eliminates raw material sourcing delays. Five full-time QA/QC technicians conduct inline stitch density verification, tensile strength testing, and seam-burst evaluation before packaging.
Quantifiable operational benchmarks reflecting 14+ years of industrial sportswear production
Tailored Supply Solutions for Educational Institutions, Professional Leagues, Distributors, and Private Labels
School athletic directors face strict budgeting and tight seasonal deadlines. GoldenLeaf provides streamlined roster management, allowing unique player names, numbers, and custom sizes within a single 10-piece production batch at no surcharge.
Complete ODM/OEM white-labeling services including custom woven neck tags, heat-seal care labels, barcoded polybags, custom hangtags, and branded master cartons ready for direct Amazon FBA or 3PL warehouse fulfillment.
Rugby, American Football, and Lacrosse demand high-tensile fabric constructions. Our proprietary reinforced twin-needle stitching, flatlock dynamic flexibility seams, and 280 gsm heavyweight stretch panels resist tearing during match play.
Pioneering Next-Generation Bio-Polymers, Waterless Sublimation, and Smart Performance Wear
Transitioning 40% of standard stock interlock fabrics to rPET (recycled polyethylene terephthalate) derived from ocean plastics, alongside closed-loop sublimation paper recycling systems that reduce solid waste by 65%.
Deployment of generative neural algorithms for pattern layout optimization, lowering fabric offcut waste to under 3% while enabling instant digital pre-production proofing within 4 hours of artwork submission.
Incorporation of conductive micro-filaments and phase-change materials (PCM) within Goldenleaf power solution garments, offering real-time physiological thermal regulation for extreme climate sports performance.
Comprehensive Regulatory Adherence and Friction-Free International Trade Management
Expanding across international borders requires rigorous compliance with environmental, chemical, and labor regulations. GoldenLeaf Sports operates with total transparency, providing enterprise clients with complete documentation and frictionless trade terms.
A Controlled Manufacturing System Guaranteeing Zero Defect Shipments
Verification of vector vector artwork, Pantone color mapping, fabric weight selection, and size break submission.
Computer-assisted 2D/3D pattern grading tailored to specific sport mobility requirements and regional size standards.
Delivery of high-resolution digital proofing within 24–48 hours for client approval before physical sample execution.
Color-managed high-density printing onto specialized thermal release paper using non-toxic imported ink formulations.
Deep-fiber thermofixation at 200°C ensuring permanent color lock that withstands high-temperature industrial laundering.
Contour-guided optical camera laser cutting for zero distortion on geometric stripes, side panels, and sleeve badges.
Flatlock four-needle six-thread and twin-needle seam construction by senior apparel technicians with 10+ years experience.
Individual 100% garment inspection for dimensional accuracy, thread trimming, polybag packaging, and master carton auditing.
Explore Extended Team Kits, Protective Apparel, and Specialty Sublimated Sportswear Lines
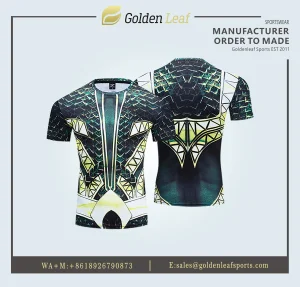
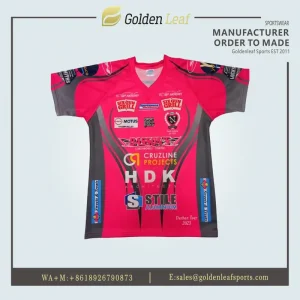
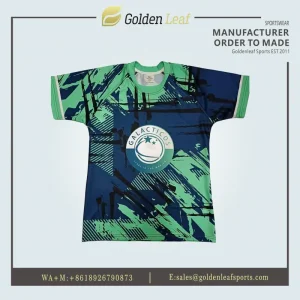
In-Depth Operational Insights Directly from Our Factory Production Desk
Our standard Minimum Order Quantity is 10 pieces per design for sublimated jerseys, shorts, pinnies, and technical tops. Because each panel is printed digitally prior to cutting, individual player names, squad numbers, and specific body sizes can vary across the 10-piece run at zero additional charge. Knitted accessories such as socks and headwear carry separate minimum thresholds based on yarn setup.
We utilize standardized X-Rite spectrophotometers combined with custom RIP software calibration profiles engineered specifically for our sublimation ink chemistry. Physical color swatches or digital Pantone (PMS) codes are matched with less than Delta E < 1.5 variance, ensuring complete visual unity across re-orders season after season.
Digital 2D artwork mockups are delivered within 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Standard production orders of 300 to 1,000 units are fully printed, cut, sewn, and inspected within 12 to 18 working days. Expedited production slots are available upon commercial review.
Yes. We offer complete turnkey private-label execution. This includes custom woven neck labels, heat-seal neck transfers, custom barcode hangtags, individual branded polybags, and specialized master carton marking designed to sync directly with your 3PL or retail distribution centers.
We maintain an extensive inventory of engineered synthetic textiles including micro-interlock (145-180 gsm), high-performance bird-eye mesh, 4-way stretch poly-spandex blends (88/12), abrasion-resistant rugby twill, and fleece-backed thermal micro-fibers. All textiles are pre-treated for moisture wicking, antimicrobial behavior, and UPF 50+ UV protection.