GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
High-performance sublimated teamwear engineered for global exporters, clubs, and sports apparel distributors.
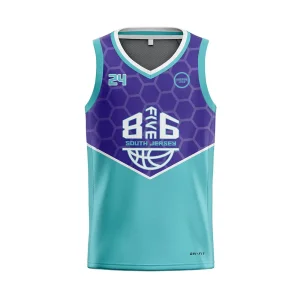
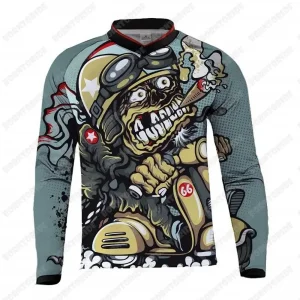
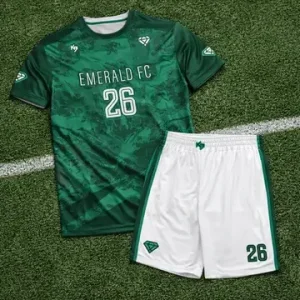
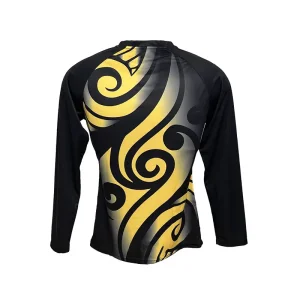
Evaluating the structural transition from legacy cut-and-sew apparel to high-precision full-dye sublimation uniform manufacturing.
The global market for custom athletic teamwear is accelerating toward an estimated $11.4 Billion valuation by 2028. Within this expansion, wholesale fully sublimated football kits represent the fastest-growing segment, projected at a CAGR of 7.8%. Commercial buyers are rapidly moving away from traditional screen-printed stock items toward full-custom, digitally dyed team solutions.
Professional leagues, collegiate academies, and regional sporting goods importers increasingly require single-source OEM/ODM suppliers. Modern B2B procurement strategies prioritize manufacturers capable of supporting micro-batch agility (low MOQs starting at 10 units) alongside high-capacity scaled production runs exceeding 100,000 units per month without compromising color fastness or seam durability.
Distributors and e-commerce exporters are adopting print-on-demand B2B supply chains. By establishing strategic partnerships with China-based export manufacturers like GoldenLeaf Sports, global buyers eliminate stock-holding risks, enabling infinite design variations, personalized player rosters, and multi-sponsor integrations embedded directly into the fabric matrix.
Understanding molecular dye infusion, synthetic filament construction, and performance moisture-wicking mechanics.
Unlike surface-applied screen printing or heat transfer vinyl (HTV), high-precision dye sublimation is a chemical phase-change process. Solid disperse dyes printed on transfer paper are subjected to thermal press conditions calibrated between 195°C and 205°C under controlled pneumatic pressure for 28 to 35 seconds.
Under these conditions, the dye sublimates directly into a gaseous state without entering a liquid phase. Concurrently, the polymer chains of the white 100% polyester substrate heat up and open their molecular pores. The gaseous dye penetrates deep into the synthetic fibers. As the fabric cools, the polymer pores close, permanently locking the pigment within the core filament. This yields zero surface weight, absolute zero cracking, and unlimited resistance to fading across hundreds of industrial wash cycles.
Engineering premium football jerseys requires balancing structural integrity, tear resistance, and moisture dissipation. GoldenLeaf Sports utilizes specialized polyester warp-knitted and circular-knitted technical textiles:
Inside GoldenLeaf Sports' 3,000 m² Shenzhen facility: 8-stage industrial precision execution.
3D CAD master patterns are digitally graded across global sizing scales (US, EU, AU, Asian, Youth 6Y–14Y, Adults up to 5XL). Vector graphics are nested to optimize fabric yield.
Industrial Epson & Mimaki print engines deploy fluorescent and standard inks, driven by customized Raster Image Processors (RIP) calibrated to target Pantone PMS color profiles precisely.
Continuous oil-heated rotary calenders maintain uniform temperature distribution (+/- 1°C variance), bonding dyes across raw white polyester rolls without shrinkage distortion.
Automated optical camera-guided laser cutters read printed registration marks, executing panel cuts with millimeter precision to prevent graphic misalignment along seam boundaries.
A quantitative evaluation of apparel customization technologies for commercial buyers.
| Evaluation Vector | Full Dye Sublimation | Traditional Screen Printing | Heat Transfer Vinyl (HTV) |
|---|---|---|---|
| Graphic Lifespan | Permanent (Fibers Dyed) | 50–80 Washes (Prone to Peeling) | 30–50 Washes (Prone to Cracking) |
| Fabric Breathability | 100% Retained (Zero Feel) | Blocked in Printed Zones | Completely Sealed / Heavy Plastic Feel |
| Color Granularity | Unlimited Colors, Gradients & Shadows | Cost per Added Spot Color | Limited to Solid Vector Shapes |
| Micro-Order Feasibility (MOQ) | High (Economical from 10 units) | Low (High Setup/Screen Fees) | Medium (High Labor Setup) |
| Player Personalization | Included at Zero Extra Cost | Expensive Separate Number Setup | Time-Intensive Manual Cutting/Pressing |
| Environmental Impact | Waterless Dye Process, Low Waste | High Chemical Sludge & Wash Water | High Synthetic Film Waste |
Aligning export sportswear production with global quality regulations and territory-specific consumer requirements.
Demands heavy focus on athletic sizing scales (extended sizing up to 5XL), high durability against physical tackle sports, and strict compliance with CPSIA lead and phthalate restrictions for youth apparel lines.
Requires strict compliance with REACH regulations regarding Azo dye restrictions and heavy metal concentrations. Environmental certifications such as OEKO-TEX Standard 100 certification and recycled fiber adoption (rPET) drive purchasing decisions.
Demands elevated UV protection factors (UPF 50+) integrated into base fabrics to withstand intense solar radiation, alongside lightweight micro-mesh panels to maximize moisture evaporation in heat-dense environments.
How next-generation materials and AI-driven workflows are transforming custom football uniform manufacturing.
GoldenLeaf Sports is transitioning core inventory lines toward certified recycled polyester extracted from post-consumer water bottles. By converting ocean-bound plastic waste into high-tenacity yarn, our rPET football kits reduce carbon emissions by 45% and energy consumption by 52% compared to virgin polyester, while delivering identical dye-receptive performance.
By integrating machine learning algorithms into vector nested marker software, our automated cutting tables optimize panel geometry across multiple sizes simultaneously. This technical advancement reduces textile cutting scrap from the industry average of 18% down to under 4%, directly passing cost savings to wholesale buyers.
Streamlining the global sourcing experience for international brands, wholesalers, and importers.
Every production batch undergoes rigorous AQL 2.5 inspection protocol. Five dedicated QA inspectors check seam tensile strength, neckband stretch memory, logo alignment, and color fastness before single-garment polybagging.
We provide full custom branding packages including heat-transfer neck labels, custom woven hem tags, barcoded hangtags, custom eco-polybags, and master carton markings customized for your local warehouse management system.
Support for flexible commercial trade terms including EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid). Express air shipping delivers within 4–7 business days; optimized sea freight provides bulk cost containment.
Direct factory answers covering technical specifications, ordering workflows, and custom capabilities.
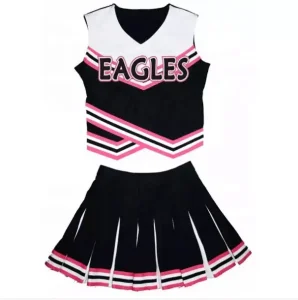
Explore our broader manufacturing capabilities spanning rugby, cricket, cheerleading, and daily athletic wear.