GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our export-grade sublimated and custom-cut performance line engineered for professional leagues, clubs, and international distributors.
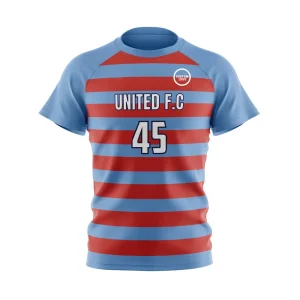
The transition from low-end promotional fleece to high-end structural streetwear requires advanced textile science, precision GSM calibration, and rigorous garment construction.
High-quality hoodie manufacturing begins at the yarn level. Premium weight tiers range from 350 GSM (midweight streetwear) to 500+ GSM (heavyweight structured fleece). Utilizing 100% ring-spun combed cotton or technical cotton-poly blends (80/20 ratio), our mills ensure low-pilling performance (Grade 4.5+ under ISO 12945-2) while maintaining superior hand-feel and dimensional stability after industrial laundering.
We engineer two primary interior structures: 3-Thread French Terry for breathable multi-season versatility, and Brushed Back Fleece for maximum thermal retention. Our tight-knit face construction (32-singles yarn) creates a dense, smooth canvas ideal for high-definition screen printing, direct-to-garment (DTG), intricate embroidery, and edge-to-edge sublimation without fiber distortion.
Structural failure in hoodies typically occurs at the armhole, kangaroo pocket, and ribbing junctions. We utilize 5-thread flatlock stitching and double-needle cover-stitching across all stress points. Hoods are constructed with double-layered self-fabric linings to prevent sag, featuring reinforced metal eyelets and high-density braided drawstrings with aglets.
Quality Assurance Protocol: All fabric rolls undergo pre-shrinkage steam setting and compaction treatment. Our final garments guarantee a post-wash shrinkage tolerance of under 3% (AATCC 135 standards), ensuring consistent fit retention across global retail channels.
Based in the technology and manufacturing hub of Shenzhen, China, our integrated production facility leverages automated precision machinery to deliver rapid turnaround and scale.
Our 3,000 m² Shenzhen campus integrates computer-aided design (CAD) software with high-speed automated CNC knife and laser cutting systems. By analyzing pattern layout efficiency down to the millimeter, we optimize fabric utilization by over 92%, reducing material waste and ensuring absolute size consistency across thousands of hoodie units.
Utilizing a Manufacturing Execution System (MES), every batch of custom hoodies is tracked from grey cloth dyeing to final polybag packaging. Our flexible assembly lines seamlessly transition between small-batch custom team orders (MOQ 10 pcs) and large-scale private label enterprise shipments (50,000+ pcs) without compromising quality control timelines.
Solving complex supply chain bottlenecks through flexible production tiers, rapid prototyping, and end-to-end OEM/ODM custom branding solutions.
We provide comprehensive private label customization. From custom woven neck labels, silicone sleeve badges, screen-printed wash tags, to custom embossed metal drawcord aglets and branded bio-degradable polybags, we turn your line-sheets into retail-ready apparel.
Avoid heavy capital lockup. Our quick-turn replenishment program allows brands to test market demand with low initial MOQs (starting at 10–50 pieces per tech pack) and scale rapidly into thousands of units within 12 to 18 working days once sales velocity is validated.
We support DDP (Delivered Duty Paid), FOB Shenzhen, CIF, and express air shipments worldwide. Our export documentation team manages customs clearance seamlessly across North America, Europe, Australia, and the Middle East, delivering straight to your fulfillment centers.
Meeting strict international environmental, labor, and chemical safety standards to ensure smooth market access for global retail brands.
Our raw materials and auxiliary trims are thoroughly vetted against EU REACH regulations and US CPSIA chemical limits. We strictly prohibit lead, phthalates, heavy metals, and harmful azo dyes, ensuring your apparel range qualifies for global commercial release without regulatory roadblocks.
In response to growing ESG requirements, we offer GOTS-certified (Global Organic Textile Standard) organic cotton and GRS-certified (Global Recycled Standard) recycled polyester yarns sourced from post-consumer PET bottles. All digital sublimation processes utilize non-toxic, eco-friendly water-based inks.
Driving the future of smart apparel manufacturing through technical innovations, digital twin prototyping, and functional textiles.
Integration of phase-change materials (PCM) and micro-encapsulated thermal insulation. Next-gen hoodies will dynamically adapt to body temperature shifts, offering lightweight insulation in cold environments while enhancing moisture breathability during active use.
Accelerating design cycles from weeks to hours. By leveraging 3D digital twin rendering software (CLO3D / Browzwear), brands can visualize fit, fabric drape, pattern placement, and colorways prior to physical sampling, cutting prototyping cost and time by over 70%.
Expanding our 3D seamless circular knitting technology. By knitting complete garment panels directly from yarn inputs without cutting loss, zero-waste manufacturing guarantees unmatched seam comfort and superior energy efficiency.
GoldenLeaf Sports (ShenZhen) Co., Ltd. is a specialized OEM & ODM manufacturer of digital sublimated teamwear and custom sportswear, serving global clients since 2011.
Operated by a team of over 160 skilled professionals—80% of whom are senior apparel technicians—GoldenLeaf Sports manages pattern grading, RIP color management, heat-press transfer printing, precision cutting, sewing, and strict quality control inside our 3,000 m² factory campus in Longgang District, Shenzhen.
Our dedicated 5-person QA/QC team inspects 100% of finished orders, verifying color fastness (Grade 4+), seam strength, size measurements, and print alignment before shipping to the US, Canada, Australia, UK, Germany, and beyond.
Factory Address: Room 2309, Yingfeng Center, Jianxin Road South, Longgang District, Shenzhen, Guangdong, China. (518117)
“We ordered these for our youth league. The quality is amazing—washes and wears well. Print execution was spotless. We will definitely reorder for next season.”
“Comfortable, durable fabric and true to sizing. The sublimation colors are vibrant and hold up extremely well through repeated washings.”
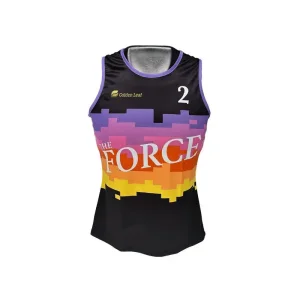
“Great customer service and fast delivery turnaround. The custom volleyball uniform material is lightweight, breathable, and top-tier quality.”
Factory-direct insights on minimum order quantities, lead times, customization techniques, and global shipping policies.
Our standard flexible MOQ starts at just 10 pieces per design for digitally printed sportswear and custom hoodies. This allows emerging brands, clubs, and distributors to launch custom line-ups without heavy inventory risk. Bulk production scaling spans up to tens of thousands of units with tiered quantity discounting.
We supply a diverse range of fabric options including 100% Cotton, Cotton/Polyester blends (80/20, 65/35), and 100% Performance Polyester fleece. Available fabric GSM ranges from 280 GSM lightweight fleece, 350 GSM standard midweight, up to 450–500 GSM ultra-heavyweight luxury loopback French Terry and brushed fleece.
We offer end-to-end customization services including 3D Puff Embroidery, High-Density Screen Printing, Digital Direct-to-Garment (DTG), Full-Coverage Digital Sublimation, Custom Woven Labels, Heat-Transfer Neck Tags, Custom Drawstring Aglets, and Branded Outer Packaging.
Digital mock-ups and virtual tech pack approvals are completed within 24–48 hours. Physical pre-production samples take 5 to 7 working days. Once the sample is approved, bulk production of 300 to 1,000 pieces typically ships within 12 to 18 working days from our Shenzhen factory floor.
Yes, we export globally via EXW, FOB Shenzhen, CIF, and DDP (Delivered Duty Paid) terms. We partner with DHL, FedEx, UPS, and air/sea freight logistics providers to ensure clear tracking, prepaid import duties, and hassle-free door-to-door delivery worldwide.
Browse additional customized garments from our extensive manufacturing matrix built for athletic leagues, performance teams, and global distributors.