GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
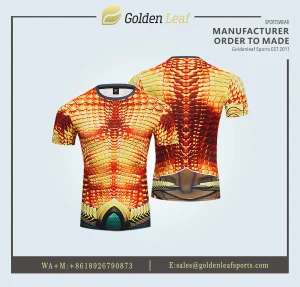
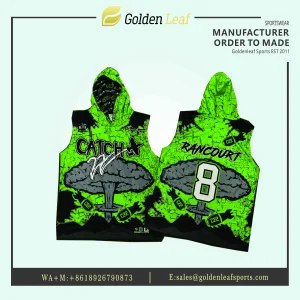
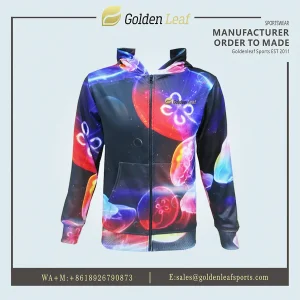
Explore our flagship custom engineered jerseys, training wear, and sublimation athletic garments built for high-level athletic performance.
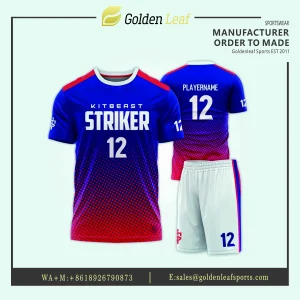
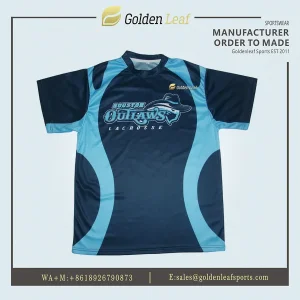
A comprehensive technical evaluation for enterprise procurement managers, sportswear brand owners, and global distributors seeking long-term supply resilience.
In the contemporary apparel ecosystem, selecting an authoritative wholesale shirt supplier involves moving beyond transactional unit costing. Modern procurement requires a holistic analysis of textile technology, colorimetric consistency, supply chain agility, and strict compliance frameworks. As modern sportswear and corporate apparel demand higher thermal regulation, mechanical stretch, and vibrant branding durability, original equipment manufacturers (OEM) and original design manufacturers (ODM) must operate at the intersection of material science and digital automation.
Core Procurement Insight: Digital dye-sublimation technology eliminates the physical film layer associated with traditional screen printing or vinyl transfers. By bonding disperse dyes directly into the synthetic polymer matrix at temperatures reaching 200°C–215°C, garments maintain 100% of their base fabric breathability, tensile strength, and moisture management performance.
Performance apparel performance relies on base polymer selection. Leading B2B shirt suppliers leverage specific yarn structures engineered for distinct kinetic environments:
| Fabric Type | Composition & Structure | Weight (GSM) | Primary Athletic / Industrial Application | Key Performance Indicators |
|---|---|---|---|---|
| Micro-Mesh Interlock | 100% Poly-micro filament, High-Gauge Knit | 145 - 160 GSM | Soccer, Running, Lacrosse Training Shirts | Rapid evaporative cooling, anti-pilling Grade 4+ |
| Bird-Eye Moisture Mesh | 100% Polyester 3D Honeycomb Structure | 150 - 180 GSM | Basketball Practice Jerseys, Active Tops | Maximized surface area for directional sweat transport |
| 4-Way Poly-Spandex | 88% Polyester / 12% Elastane Blend | 180 - 220 GSM | Cycling Shorts, Compression Tops, Rugby Kits | High elastic recovery, dynamic muscular compression |
| Heavyweight Rugby Twill | 100% High-Tenacity Polyester Twill | 260 - 300 GSM | Contact Sports, Rugby League & Union Uniforms | Superior tear strength, anti-grab structural integrity |
How state-of-the-art digital workflows in Shenzhen transform traditional textile production into an agile, transparent manufacturing engine.
Utilizing high-speed optical vision laser cutters, panel shapes are trimmed along sublimation registration lines within a 0.5mm tolerance. This prevents pattern misalignment along shoulder and side seams across all graded sizes.
By employing high-density imported European sub-inks integrated with color-managed Raster Image Processor (RIP) software, our manufacturing lines ensure precise Pantone matching (Delta E < 1.0) and zero hazardous solvent discharge.
Our Manufacturing Execution System (MES) tracks every cut piece from raster printing to final needlework, giving B2B clients full visibility into order progression and guaranteeing fast 12-to-18-day turnaround times.
Bridging the gap between raw manufacturing capability and the complex compliance, packaging, and logistical requirements of international B2B buyers.
Enterprise shirt buyers—ranging from multi-location corporate gear suppliers to high-volume athletic apparel brands—encounter distinct operational friction points. Securing a trusted wholesale shirt supplier requires a manufacturing partner capable of executing customized specifications without sacrificing scalability.
Traditional shirt factories often require high minimum order quantities (MOQs) exceeding 1,000 units per style/color combination. GoldenLeaf Sports solves this by offering a flexible baseline MOQ of just 10 pieces for full-sublimation runs. Because graphics are transferred directly onto uncut fabric panels via digital transfer, each individual garment within a single batch can feature dynamic variables (e.g., individual player names, numbers, regional sponsor logos, and unique sizes) with zero re-tooling cost.
For distributors looking to build proprietary brand equity, we provide full ODM and private-label packaging integrations. These include:
Athletic performance apparel requires specialized seam construction to endure intense physical stress. Our production lines implement 4-needle 6-thread flatlock stitching along critical stress junctions (such as armholes, raglan shoulders, and inseams). This low-profile seam lies completely flat against the skin, virtually eliminating chafing during movement while delivering exceptional seam tensile strength.
Pioneering sustainable materials, smart textiles, and AI-driven pattern optimization for next-generation apparel programs.
Transitioning base cloth offerings to 100% post-consumer recycled polyethylene terephthalate (rPET) derived from ocean plastics. These yarns offer identical tensile strength and dye receptivity while reducing carbon emissions by up to 32% per garment production cycle.
Algorithm-driven marker placement software minimizes fabric off-cut waste down to less than 6%. Automated pattern grading instantly scales anatomical dimensions across XS to 5XL sizing matrixes without distortion.
Integrating micro-encapsulated phase-change materials (PCMs) within shirt fibers to absorb, store, and release body heat dynamically, establishing optimal microclimate comfort under extreme environmental conditions.
Ensuring seamless market entry into North America, Europe, and Oceania through rigorous quality standards and trade compliance.
Exporting high-performance custom teamwear and commercial shirts across international borders demands total alignment with safety and environmental legislation. GoldenLeaf Sports operates under audited quality control regimes to ensure your imports clear customs swiftly:
Technical clarity on production schedules, fabric performance, customization parameters, and order fulfillment.
Digital vector mock-ups are delivered within 24 to 48 hours following artwork submission. Once pre-production artwork is formally approved, physical sampling requires 5 to 7 working days. Standard bulk production runs (ranging from 100 to 2,500 pieces) typically ship in 12 to 18 working days from our Shenzhen manufacturing plant.
Screen printing lays a thick layer of plastisol ink over top of the fabric, which can crack over time and block the fabric's natural pores. Dye sublimation converts ink into a gas under extreme heat, bonding it directly into the polyester fibers. This produces zero hand-feel, preserves full breathability, guarantees colorfastness, and allows unlimited logo and color placement at no extra cost per shirt.
Yes. We maintain fully calibrated pattern libraries for North American, European, and Australasian sizing standards across Men's, Women's, and Youth cuts (from 6Y up to 5XL). Furthermore, buyers can submit custom measurement specification sheets (tech packs), and our pattern masters will create tailored CAD grading templates accordingly.
Every production lot undergoes a rigorous 5-stage quality inspection matrix: 1) Raw fabric tension and defect scan, 2) Post-sublimation color-matching verification against Pantone standards, 3) Laser-cut measurement checks, 4) In-line seam tensile strength testing, and 5) Final inspection of finished polybagged units by 5 dedicated QA inspectors prior to packing.
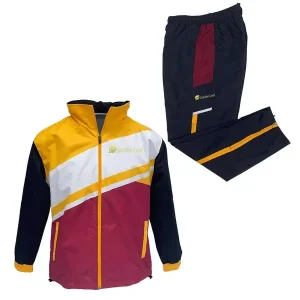
Explore additional specialized performance garments, outerwear, and custom sports accessories engineered to meet global trade requirements.