GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
High-performance digital sublimated teamwear engineered for global distributors, professional clubs, and regional athletic brands.
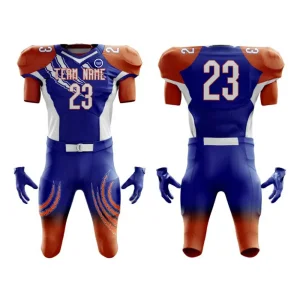
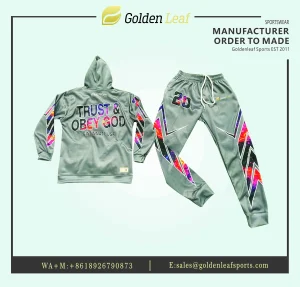
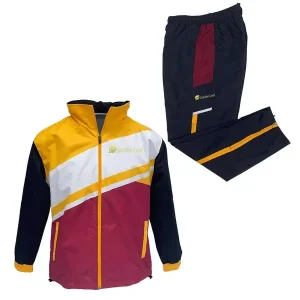
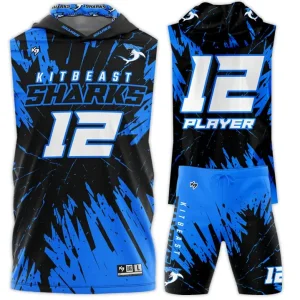
An exhaustive technical evaluation of macro industry shifts, OEM agility demands, and supply chain resilience for modern athletic teamwear sourcing.
The global athletic apparel ecosystem is experiencing a profound paradigm shift. Enterprise buyers—ranging from multi-brand athletic distributors to national sports leagues and university procurement departments—no longer evaluate wholesale sports uniform manufacturers purely on piece-rate pricing. Today, strategic intent revolves around supply chain velocity, technical textile integrity, zero-defect quality control, and deep OEM/ODM customization capability.
Offshore apparel sourcing traditionally introduced significant friction: unpredictable fabric batch dye variations, delamination of screen-printed numbers, misaligned pattern seams, and extended 60-day transit cycles. Leading Chinese sports apparel manufacturers have responded by integrating end-to-end digital sublimation workflows, automated optical registration cutting, and standardized ISO 9001:2015 quality inspection gates directly under one factory roof.
Decoupling performance limitations through molecular dye diffusion, micro-denier synthetic fibers, and advanced ergonomic pattern grading.
Unlike traditional screen printing or vinyl heat transfers which deposit a surface film over the weave (choking yarn breathability), digital dye-sublimation vaporizes dispersion inks at 200°C–220°C. Under high pressure, gasified dyestuffs permeate the amorphous regions of the polyester polymer matrix, forming a permanent molecular bond. The result: absolute color fastness (Grade 4.5+), zero hand-feel weight, and uninhibited capillary moisture transit.
Our engineering team formulates proprietary fabric blends tailored to sport-specific biomechanics. Interlock weaves (145–180 GSM) offer smooth tensile strength for soccer and ultimate frisbee. High-density bird-eye micro-mesh provides maximum airflow for basketball heat dissipation. Meanwhile, 4-way stretch poly-spandex (88/12 ratio, 220 GSM) enables unrestricted dynamic range for compression baselayers and volleyball uniform sets.
Color fidelity remains the chief benchmark for teamwear authenticity. Utilizing imported Italian eco-certified inks alongside raster image processor (RIP) software, our color technicians execute strict Pantone Matching System (PMS) target profiling. Every production run undergoes spectrophotometer analysis to ensure batch-to-batch color delta (ΔE) remains below 1.0 across full team rosters.
| Fabric Classification | Composition & Weight | Primary Athletic Application | Key Performance Metrics |
|---|---|---|---|
| Cool-Max Interlock | 100% Micro-Polyester (145-160 GSM) | Soccer, Frisbee, Running Kits | Hydrophilic wicking, Anti-bacterial finish, UPF 30+ |
| Bird-Eye Open Mesh | 100% Polyester Mesh (160-180 GSM) | Basketball, Lacrosse Pinnies | High porosity ventilation, Rapid evaporative cooling |
| Pro-Flex Stretch Poly | 88% Polyester / 12% Spandex (200-240 GSM) | Volleyball Shorts, Compression Wear | 4-way elastic recovery, Flatlock chafe reduction |
| Heavy-Duty Rugby Twill | 100% High-Tenacity Poly (280-320 GSM) | Rugby Match Kits, American Football | Extreme tensile/burst strength, Reinforced collar seam |
From vectorized CAD block patterns to final individual poly-bagging: an 8-stage zero-defect manufacturing standard.
Precision pattern grading based on international sizing standard blocks (US, EU, AU, Youth). Digital registration mark insertion ensures exact logo placement across sizes XS to 5XL.
Wide-format industrial inkjet plotters print vector graphics onto specialized heat-transfer paper using high-chroma, non-toxic sublimation inks calibrated to exact PMS values.
Flatbed rotary heat presses maintain strict thermal equilibrium (210°C at 6 bar pressure) to infuse dye deeply into un-cut white fabric rolls without ghosting or blurring.
Automated optical camera lasers scan registration marks and slice fabric panels with sub-millimeter precision, fusing raw synthetic edges to eliminate fraying during assembly.
Skilled technicians utilize multi-needle overlock and 4-needle 6-thread flatlock machines. Stress points (armpits, necklines, crotch seams) receive double-tacked reinforcement.
Application of customized private-label woven neck tags, heat-seal size transfers, elastic drawcords, anti-slip silicone waist grippers, and sponsor patches.
A dedicated 5-inspector QC station checks dimensional tolerance (+/- 1cm), seam tensile integrity, player name/number matching against master roster, and color hue accuracy.
Individual eco-polybag packing sorted by team roster, carton consolidation with moisture-absorbent desiccant, and rapid DDP/FOB dispatch via express courier, air, or sea freight.
Meeting international trade regulations, environmental safety directives, and market-specific sizing standards.
Environmental governance is mandatory for modern sports apparel compliance. All raw base fabrics and sublimated dye compounds utilized in our Shenzhen production facility comply with OEKO-TEX Standard 100 (Class I for skin contact) and EU REACH regulations, guaranteeing freedom from heavy metals, azo dyes, formaldehydes, and perfluorinated chemicals (PFCs).
Navigating international customs tariffs requires expert logistic coordination. We offer complete OEM private-label branding packages—including customized barcode ticketing, HS-code tariff optimization (e.g., 6114.30 synthetic teamwear classifications), and flexible shipping terms (EXW, FOB Yantian/Shenzhen, CIF, and door-to-door DDP duty-paid options).
For regional sportswear brands seeking to expand product offerings without capital expenditure in machinery, our factory functions as an invisible manufacturing engine. We support full custom neck taping, custom zipper pulls, heat-transfer wash instructions, retail hangtags, and custom-printed polybags to present a seamless brand image to your end customers.
Detailed factory-direct answers addressing critical buyer considerations regarding order volumes, lead times, custom sizing, and quality assurance.
Our baseline MOQ is just 10 pieces per design for full-sublimation jerseys, shorts, tracksuits, and pinnies. Because every panel is digitally printed prior to precision laser cutting and assembly, individual player names, squad numbers, and specific player sizes can vary within the same 10-piece order at no additional setup surcharge. For large bulk distributor orders (500+ pieces), stepped volume discounts automatically apply.
Once vector artwork files and player roster spreadsheets are signed off:
• Digital Artwork Vector Proof: Delivered within 24 to 48 hours.
• Physical Pre-Production Sample: Completed and dispatched within 5 to 7 working days.
• Standard Bulk Run (100 to 1,000 Pcs): Manufactured, audited, and ready for shipment within 12 to 18 working days. Rush production options are available for urgent league kick-off deadlines.
We store master RIP digital color profiles alongside physical fabric swatch archive references for every customer project. By strictly monitoring heat-press temperature stability, humidity levels, and utilizing imported non-fading Italian inks, we guarantee a color delta variance (ΔE) of less than 1.0. Re-orders placed 12 months later will match the original team kits seamlessly.
Yes. While we maintain standard CAD pattern blocks for US Youth, US Adult Men's, European Slim Fit, and Australian/UK sizing, we frequently manufacture custom sizing charts provided directly by enterprise clients. Whether your brand requires extra length in basketball jerseys, specific inseams in lacrosse shorts, or tailored ladies' athletic cuts, our pattern engineers can adapt all garment blocks prior to cutting.
Every garment passes through a 4-tier inspection process: (1) Raw fabric inspection for tension defects and GSM consistency; (2) Post-sublimation print inspection to catch paper creases or color spots; (3) Sewing line inline inspection for seam strength, thread tension, and structural symmetry; and (4) Final table QC audit checking measurements against specs, spelling of player names, number accuracy, and overall finishing before individual poly-bag packaging.
Explore our specialized performance series including racing polos, baseball jerseys, tracksuits, compression tops, and lacrosse equipment shorts.