



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our premium custom-manufactured athletic lines designed for maximum durability, breathability, and color vibrancy.
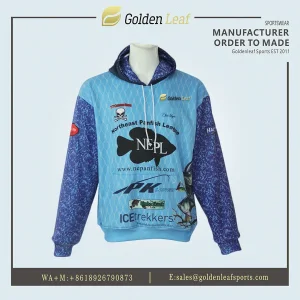
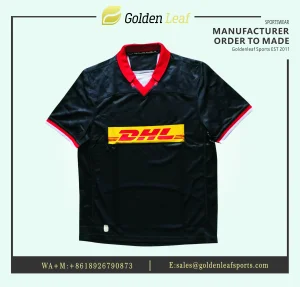
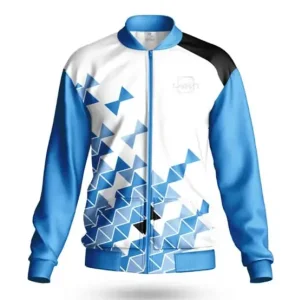
An in-depth analysis of global procurement trends, material innovation, and textile engineering in professional baseball apparel.
For decades, traditional baseball uniforms relied on heavy cotton twill, screen-printed vinyl, or stitched tackle-twill patches. While visually classic, these legacy methods introduced severe technical limitations on the field: excessive overall garment weight, restricted shoulder movement, thermal heat retention, and seam abrasion during sliding.
Modern sports science demands ultra-lightweight, thermoregulated fabrics. Digital dye sublimation infuses eco-friendly inks directly into the microscopic structure of polyester microfibers under high temperature and pressure. The result is zero added weight, 100% fabric breathability, and lifetime resistance against fading, cracking, or peeling.
B2B apparel buyers, brand managers, and sports league procurement teams must weigh performance, cost-efficiency, and design complexity when specifying custom teamwear. The matrix below outlines the operational advantages of wholesale sublimated baseball uniforms:
| Evaluation Parameter | Full Digital Dye Sublimation | Traditional Tackle Twill / Embroidery | Screen Printing / Heat Transfer |
|---|---|---|---|
| Garment Mass Index | Ultra-Lightweight (145 - 220 GSM) | Heavy (300+ GSM due to patches) | Medium (Rubberized ink mass) |
| Moisture Management | Unrestricted Capillary Wicking | Blocked by heavy embroidered backing | Blocked by non-porous ink films |
| Design & Color Freedom | Unlimited Pantone gradients & logos | Restricted to basic layer cuts | Limited color screens & high setup fees |
| Durability & Longevity | Permanent fiber-level bonding (Grade 4.5+) | Stitches fray, pull, and tear over time | Prone to surface peeling and cracking |
| Variable Player Customization | Zero extra charge per player name/number | High labor charge for individual embroidery | Expensive setup per unique roster item |
Understanding the exact intent and criteria of international athletic wear importers, regional brand owners, and club managers.
Global distributors no longer want to lock up working capital in massive static inventory. Enterprise buyers actively seek manufacturers capable of supporting flexible MOQs down to 10 pieces per design, enabling fast mid-season roster top-ups without minimum unit penalties.
Brand identity relies on precise PMS (Pantone Matching System) alignment across different garment production batches. Advanced suppliers must utilize automated digital RIP color profiling to eliminate batch-to-batch shade variation across jerseys, shorts, and caps.
A true wholesale exporter must master regional sizing profiles: US Adult (S-5XL extended sizing), European Athletic Slim-Fit, Youth Graded (6Y-14Y), and Female-specific ergonomic cuts with side panel stretch zones.
Combining Shenzhen's high-tech digital ecosystem with specialized apparel craftwork for uncompromised quality.
At our 3,000 m² Shenzhen facility, manual scissor cutting has been completely superseded by high-precision optical registration laser cutters. This technology automatically aligns vector pattern artwork with fabric grain lines, ensuring zero distortion across multi-panel baseball jerseys, pinstripe alignments, and raglan sleeves.
Safety and compliance are paramount for sports apparel exported to North America, Europe, and Oceania. We utilize imported, OEKO-TEX Standard 100 certified non-toxic sublimation inks. Garments are skin-friendly, hypoallergenic, and possess high color fastness under heavy sweat and aggressive UV exposure.
With over 160 skilled technicians—80% holding senior garment engineering credentials—GoldenLeaf Sports manages the full supply chain under one roof: from initial vector design proofing in 24-48 hours to digital printing, rotary thermal transfer, laser precision cutting, flatlock reinforcement sewing, and multi-stage QA inspection.
Different competitive tiers and geographic regions require specific material weights, cuts, and functional attributes.
Requires heavy-duty 220 GSM polyester interlock bodies paired with full-button fronts, reinforced double-knee sliding pants, and deep moisture-wicking bird-eye mesh underarm panels to withstand rigorous 50+ game seasons.
Demands quick turnarounds, vibrant full-bleed graphics, lightweight 150 GSM micro-mesh construction, and affordable two-button or crew-neck jersey options for fast-growing youth athletes.
Focuses on precise aerodynamic athletic tailoring, semi-invisible flatlock stitching to prevent skin chafing, and specialized indigenous or custom art patterns integrated into jersey sleeve panels.
Complementary OEM & ODM product lines built with the same digital sublimation excellence.
Direct answers from our manufacturing engineering and international logistics team.
Our standard production minimum is 10 pieces per design. Because each panel is digitally printed prior to precision cutting, individual player names, numbers, and sizes can be customized inside the same batch at no additional artwork setup charge.
Digital vector mock-ups are delivered in 24 to 48 hours. Physical pre-production samples require 5 to 7 working days. Bulk production orders (300 to 1,000 units) ship in 12 to 18 working days directly from our Shenzhen production facility.
We supply 100% micro-polyester interlock (180–220 GSM) for jersey bodies, heavy-duty 4-way stretch poly-spandex (260 GSM) for sliding pants, and high-flow bird-eye mesh for underarm ventilation inserts. All cloths are tested for color fastness above Grade 4.
Yes. We offer complete OEM/ODM private-label integration, including custom woven back-neck tags, heat-transfer size labels, customized hangtags, branded polybags, and master carton shipping marks compliant with global customs standardizations.