GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our primary manufacturing lines. Built with high-filament micro-polyesters, eco-friendly sublimation inks, and athletic ergonomics for elite multi-sport requirements.
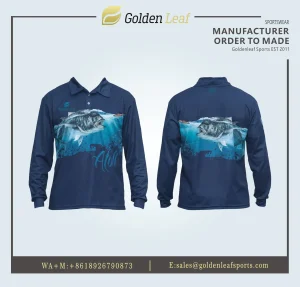
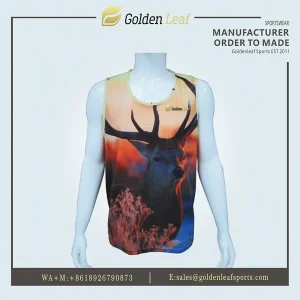
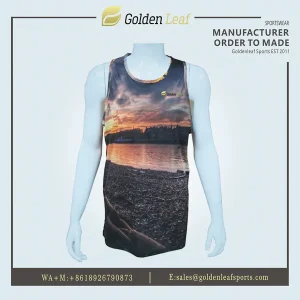
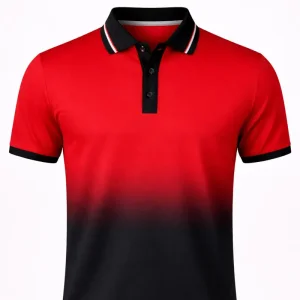
The international cricket teamwear ecosystem is undergoing a monumental paradigm shift. Transitioning from traditional heavy-weight cotton blends to high-tech, ink-fiber fused dye-sublimated synthetics, modern cricket apparel demands structural resilience, moisture thermo-regulation, and high-frequency brand customization.
The rapid proliferation of global T20 & T10 leagues (such as IPL, BBL, CPL, and Major League Cricket in North America) has driven unprecedented commercial demand for vibrant, fully customized team uniforms. Sublimation technology permits dynamic color gradients, multi-sponsor emblem integration, and rapid vector graphics printing without adding physical weight or blocking fabric breathability.
Cricket is played in intense tropical and desert micro-climates where athletes endure up to 6–8 hours in direct sun. Modern wholesale buyers require micro-polyester knits engineered with hydrophobic capillary channels that pull sweat away from the dermis to the outer fabric surface, accelerating evaporation and maintaining athlete homeothermy.
Sun exposure during Test matches and One-Day Internationals demands fabrics treated with TiO2 (Titanium Dioxide) microscopic additives to yield UPF 50+ protection. Furthermore, uniforms must withstand high abrasion from diving on hard outfield turfs without piling, snagging, or seam rupture.
Digital dye sublimation represents the pinnacle of modern sports apparel manufacturing. By fusing disperse dyes directly into the core of synthetic micro-fibers under high temperature and pressure, apparel achieves permanent, photo-realistic visual fidelity that will never crack, peel, or fade.
Understanding why full dye-sublimation dominates modern B2B sourcing over traditional screen printing or embroidered appliques:
| Technical Dimension | Full Dye-Sublimation (GoldenLeaf Standard) | Traditional Screen Printing | Vinyl Heat Transfer / Badges |
|---|---|---|---|
| Fabric Breathability | 100% Uncompromised (Ink fuses at fiber level) | Reduced (Ink creates plastic barrier) | Severely Blocked under patch area |
| Weight & Feel | Zero-Weight / Seamless hand-feel | Adds measurable gram weight | Heavy, rigid patches on torso |
| Durability & Washability | Permanent (No fading, peeling, or cracking) | Cracks after 20-30 industrial washes | Peels off under extreme dryer heat |
| Color & Design Freedom | Unlimited vector colors, photorealistic, no extra cost | Priced per color screen setup | Limited color layering options |
| Variable Player Customization | Seamless dynamic printing (Names/Numbers) | High labor cost per unique name | Requires manual alignment & pressing |
Global market requirements differ significantly based on weather conditions, regional cricket board regulations, and turf characteristics. GoldenLeaf Sports engineers customized specifications tailored to localized target markets.
Requires ultra-lightweight 145–160 GSM bird-eye micro-mesh featuring certified UPF 50+ sun reflection treatments. Pants feature reinforced 4-way stretch poly-spandex knee and groin gussets to survive sliding on hard synthetic and natural grass fields.
Specifies traditional cream/white Test match kit standards alongside vibrant T20 colorful club gear. Demands slightly heavier 170–190 GSM interlock polyester with water-repellent exterior coatings for damp pitch conditions, complemented by sublimated long-sleeve knit sweaters.
Driven by rapid growth in adult recreational leagues and school programs. Requires agile, low-MOQ sourcing (10-15 pieces per order), rapid 10-14 day turnaround, dynamic modern color combinations, and integrated US athletic size grading (S to 5XL).
Focuses on extreme breathability, anti-bacterial scent-control finishes, and high-density stitching. Designed to withstand intensive academy training regimes in 40°C+ ambient temperatures.
From raw yarn selection to final container loading, GoldenLeaf Sports enforces strict ISO-compliant quality control checkpoints to guarantee zero-defect production runs for global apparel brands.
Custom weaving of virgin or rPET eco-polyester yarns into specified GSM weights (Interlock, Pin-Tec, or Bird-Eye mesh).
Calibrating Italian/Japanese eco-solvent sublimation inks using spectrophotometers for 99.8% Pantone PMS matching.
High-pressure roll-to-roll cylinder pressing at 210°C, bonding dye into fabric fibers at microscopic levels.
Camera-guided automatic laser cutting ensuring millimeter precision on vector sleeve and side-panel alignments.
Flatlock anti-chafing stitching followed by tensile strength, seam stress, and AATCC grade 4.5 wash inspections.
We eliminate international supply chain friction through comprehensive OEM/ODM infrastructure, predictable freight management, and low financial barrier entry points.
Full custom branding suites including woven neck labels, heat-transfer inner neck sizing tags, customized hangtags with barcodes/SKUs, and eco-friendly printed polybags ready for direct retail distribution.
Cricket seasons require fast re-order cycles when new players join club rosters. Our digital vector archiving allows mid-season re-orders from as low as 10 pieces with guaranteed matching color hues and a fast 7-10 day delivery timeline.
We provide comprehensive global shipping services under EXW, FOB Shenzhen, CIF, and DDP (Delivered Duty Paid) terms via air express (DHL/FedEx/UPS) or ocean freight, absorbing customs hassle for importer partners.
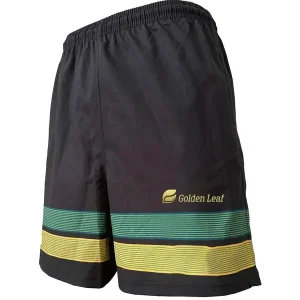
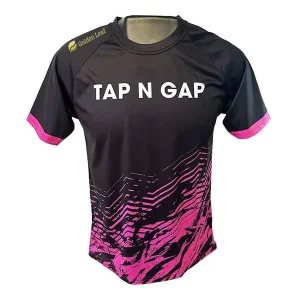
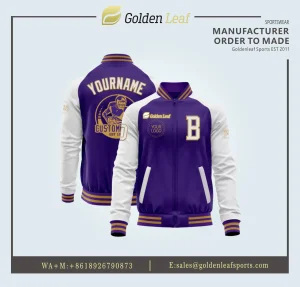
Discover our specialized bottoms, outer garments, and multi-sport custom kits built to identical professional sublimation and durability standards.
Expert insights on customization mechanics, minimum order thresholds, chemical compliance, and production turnaround for global apparel buyers.