GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
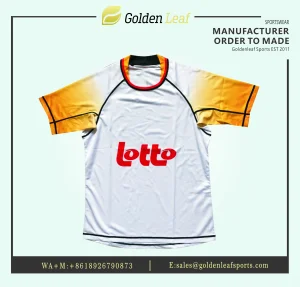
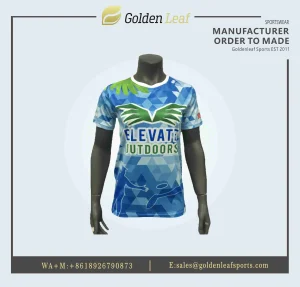
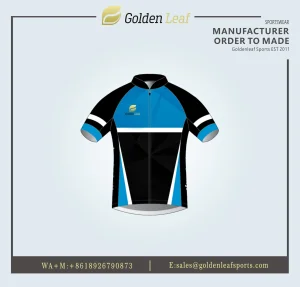
Explore our top-tier custom sublimated sportswear manufactured with imported eco-friendly inks, precision laser-cutting, and reinforced stitching.
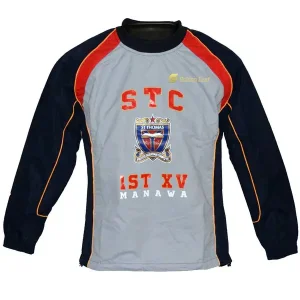
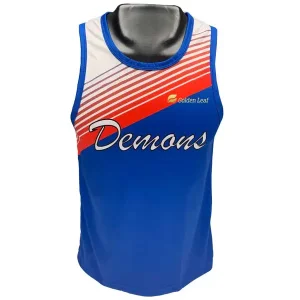
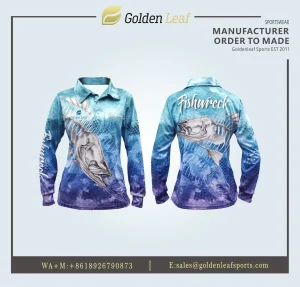
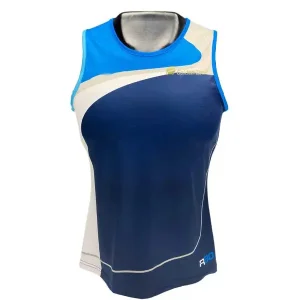
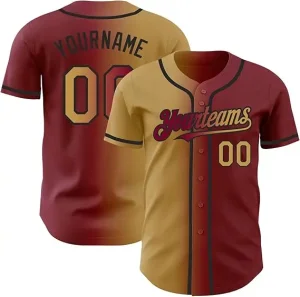
An industrial analysis of digital dye-sublimation technology, supply chain agility, and technical textile engineering in modern B2B sportswear procurement.
"The shift toward custom sublimated teamwear is no longer merely aesthetic; it is an engineering evolution. Today's global sports organizations demand dynamic thermal regulation, permanent color fastness, and zero-waste digital panel printing to meet strict environmental and performance standards."
Traditional screen printing and vinyl heat transfer introduce rigid layers that restrict airflow and peel under stress. Advanced digital dye-sublimation fuses eco-friendly aqueous inks directly into the micro-structure of synthetic fibers, guaranteeing zero fading, cracking, or peeling even after 100+ commercial wash cycles.
Modern B2B importers require extreme SKU flexibility. By leveraging digital artwork RIP (Raster Image Processor) software and integrated pattern grading, OEM facilities can execute complex multi-size, multi-name team orders with minimum order quantities (MOQs) as low as 10 units per design without incurring costly plate setups.
With global regulations like EU REACH and OEKO-TEX Standard 100 tightening, tier-1 sportswear factories strictly utilize non-toxic, heavy-metal-free sublimation dyes and recycled poly-spandex blends (RPET), protecting both athlete skin health and international brand reputation.
Operating from China's premier hardware and textile innovation hub, GoldenLeaf Sports integrates raw material knitting, digital printing, and expert sewing under a unified quality assurance protocol.
From white base-cloth stock management (145 gsm to 280 gsm polyester, bird-eye mesh, 4-way stretch poly-spandex) to automated registration-mark laser cutting, maintaining all operations within a single 3,000 m² facility eliminates third-party outsourcing delays and quality variances.
Quality assurance is embedded in every workflow step: fabric weight checking, pre-print color matching (Pantone PMS RIP validation), heat transfer bonding checks, flatlock stitching tension audits, and final dimensional measurement sign-offs by 5 full-time inspectors.
In-house digital graphic engineers deliver virtual vector mock-ups within 24–48 hours. Physical pre-production samples are completed and ready for express global courier dispatch within 5 to 7 working days, drastically accelerating brand launch cycles.
A granular breakdown of performance base-cloth materials engineered for elite athletic wear, collegiate sports, and active lifestyle brands.
| Fabric Classification | Composition & GSM | Primary Application | Key Performance Features | Color Fastness Rating |
|---|---|---|---|---|
| Micro-Mesh Interlock | 100% Polyester | 145–160 gsm | Soccer, Basketball, Ultimate Frisbee | High air-permeability, rapid-dry moisture wicking, ultra-lightweight. | Grade 4.5 (AATCC Standard) |
| Bird-Eye Knit Mesh | 100% Polyester | 155–170 gsm | Lacrosse Pinnies, Gym Shirts, Running Sets | 3D honey-comb breathability, tear resistance, soft skin-contact touch. | Grade 4.5 |
| 4-Way Stretch Performance Blend | 88% Poly / 12% Spandex | 180–220 gsm | Volleyball Shorts, Cycling Tops, Tight Pants | Multi-directional elasticity, muscle compression support, zero shape distortion. | Grade 4.0–4.5 |
| Heavyweight Reinforced Twill | 100% Tough-Knit Poly | 260–300 gsm | Rugby Kits, American Football Practice Wear | High tensile strength, abrasion resistance against tackle friction, bound seams. | Grade 4.5 |
| UV-Blocking Outdoor Poly | 100% Cool-Max Poly | 140–150 gsm | Performance Fishing Shirts, Outdoor Wear | UPF 50+ Solar Protection, moisture management, anti-bacterial treated. | Grade 4.5 |
Customized sportswear supply frameworks tailored to regional market standards, compliance laws, and logistical requirements across key continents.
Focus on Youth Leagues, High School Athletic Associations (NFHS compliance), and Collegiate Lacrosse & Basketball clubs. We provide US standard oversized grading (Youth Small to Adult 5XL), DDP (Delivered Duty Paid) air freight services, and private label neck transfers for seamless retail delivery.
Tailored for Rugby Union, Rugby League, Netball, and Touch Football teams requiring heavyweight 280gsm twill fabrics, aboriginal art sublimation reproduction with high Pantone precision, and anti-chafing flatlock stitching engineered for intense contact sports.
Meeting strict EU REACH chemical standards and eco-textile demands. We service amateur football academies, cycling clubs, and athleisure brands demanding slim European modern fit blocks, recycled polyester (RPET) base materials, and custom eco-friendly polybag packaging.
Key technology trends shaping the next decade of athletic apparel production, customization, and smart supply chain integration.
Computerized AI nesting algorithms optimize printable vector panels on paper transfer rolls, reducing fabric waste by up to 18% compared to manual layout, lowering costs while minimizing environmental impact.
Integration of graphene-infused polyester threads provides passive thermo-regulation, actively drawing excess body heat away during intense physical exertion and releasing warmth during rest periods.
Moving completely away from wet dyeing processes, thermal transfer dye sublimation consumes zero water in the coloration phase, positioning it as the ultimate clean manufacturing solution for global ESG compliance.
Discover activewear, technical cycling tops, baseball jerseys, and compression wear built for high endurance and style.
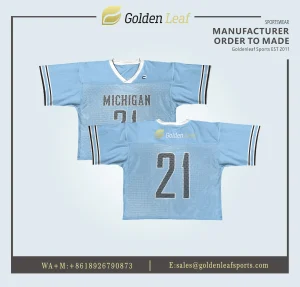
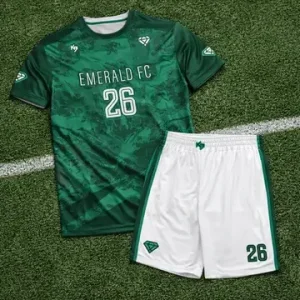
Detailed technical answers addressing minimum order quantities, private labeling, fabric testing, and international shipping protocols.