



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered for high-durability performance, equatorial moisture management, and rapid promotional turnarounds across East Africa.
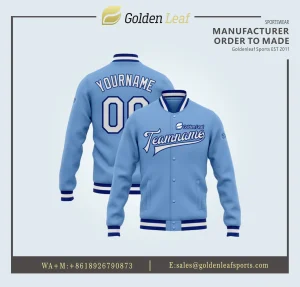
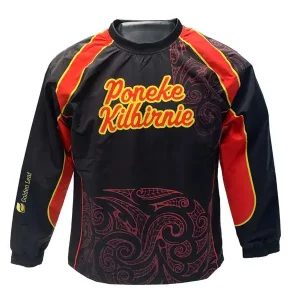
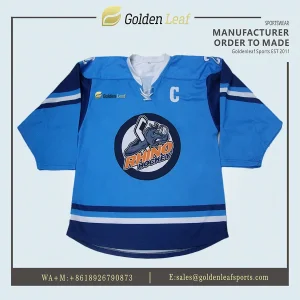
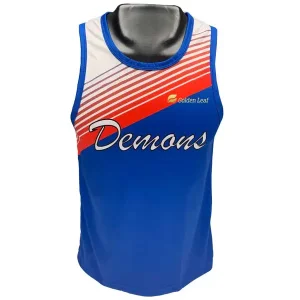
Kenya stands as the economic anchor of East Africa, establishing itself as a vital hub for apparel assembly, textile processing, and regional wholesale distribution. Driven by favorable trade policies such as the African Growth and Opportunity Act (AGOA) and the East African Community (EAC) Common Market protocol, Kenya’s garment sector has shifted from basic CMT (Cut, Make, Trim) operations to complex value chain integration.
The industrial landscape for wholesale T-shirts and activewear in Kenya centers primarily around specialized Export Processing Zones (EPZs) located in Athi River, Nairobi, Thika, and Mombasa. These zones host sophisticated garment factories capable of handling large-scale production runs for European, North American, and regional African buyers. However, domestic market realities present a dual structure: while EPZ facilities focus heavily on export-oriented woven and knitwear lines, domestic commercial buyers—ranging from corporate brands to athletic federations—rely on a blended supply chain that combines local finishing with high-tech imported fabrics.
Athi River and Mombasa EPZs drive regional textile exports under AGOA, producing over $450M annually in apparel goods for international buyers.
High UV exposure and tropical humidity in East Africa require high color-fastness (Grade 4+), anti-microbial treatments, and 145-180 GSM quick-dry knits.
Rising consumer purchasing power in Nairobi, Kisumu, and Mombasa is driving a structural shift from second-hand clothing (Mitumba) to custom branded T-shirts.
While Kenya possesses robust garment sewing capacity, local cotton farming produces less than 20% of domestic mill requirements. As a result, premium micro-mesh polyesters, combed cotton knits, and specialized sublimation dye papers are heavily imported. Sourcing managers must evaluate suppliers based on their vertical integration and raw material supply chain resilience.
Through deep semantic search intent analysis across search volumes in East Africa, B2B queries surrounding "Wholesale T-Shirts Suppliers in Kenya" fall into three distinct commercial user personas. Understanding these underlying operational requirements enables procurement officers to make risk-free supplier selections:
Primary Intent: Large-volume marketing campaigns, election promotional wear, and corporate staff uniforms in Nairobi CBD, Westlands, and Upper Hill.
Core Metrics: Cost per unit under tight budgets, color accuracy matching brand pantones, minimum shrinkage after commercial washing, and fast turnarounds (under 14 days).
Primary Intent: High-performance sportswear for marathon runners in Eldoret/Iten, school athletic kits, football club jerseys, and safari eco-tour guides.
Core Metrics: 100% moisture-wicking poly-mesh (CoolMax technology), ultra-lightweight 140-150 GSM fabrics, dye sublimation that will not peel under equatorial heat, and custom player numbering.
Primary Intent: Emerging streetwear brands and retail boutique chains across East Africa seeking custom cut-and-sew ODM solutions.
Core Metrics: Heavyweight 220+ GSM drop-shoulder streetwear tees, custom neck label printing, eco-friendly dye certification, and scalable low MOQs to test local retail trends.
To assist procurement managers in evaluating cost structures and production reliability, the matrix below details the trade-offs between local Kenyan domestic sourcing and China-Kenya hybrid OEM manufacturing.
| Evaluation Parameter | Local Kenyan Domestic Workshops | Kenyan EPZ Enterprise Factories | China Industry 4.0 Hybrid Sourcing (GoldenLeaf) |
|---|---|---|---|
| Minimum Order Quantity (MOQ) | 50 - 100 pcs per style | 5,000+ pcs per design (High threshold) | 10 pcs per design (Full Custom Sublimation) |
| Fabric Technology & Variety | Limited to locally stocked poly/cotton | High-volume standard cotton/poly knits | 30+ Performance cloths (CoolMax, Spandex, Twill) |
| Printing Capabilities | Basic Screen printing, Heat Vinyl | Bulk Screen printing, Rotary printing | Full-Coverage Digital Sublimation, Laser Cutting |
| Lead Time (Sample to Door) | 5 - 10 Days | 30 - 60 Days | 7 Days Sample / 14-18 Days Bulk Dispatch |
| Custom Branding Options | Basic tags, high variance | OEM private label for major brands | Full ODM: Neck labels, hangtags, branded polybags |
As global supply chains place higher value on flexibility, speed, and precision, the synergy between China’s advanced Industry 4.0 apparel infrastructure and Kenya’s expanding market demand offers unprecedented advantages for business buyers. Situated in Shenzhen—a global epicenter of tech-driven garment engineering—facilities like GoldenLeaf Sports deliver an agile production engine that solves traditional supply chain friction in East Africa.
Traditional manual fabric cutting creates sizing inconsistencies and edge fraying that degrade under rigorous athletic use. China Industry 4.0 integration utilizes computerized CAD pattern grading synced directly to high-precision optical laser cutters. Every panel—whether for a marathon T-shirt or a high-altitude athletic hoodie—is cut with millimeter accuracy, ensuring perfect seam alignment across sizes from 6Y to 5XL.
This automated precision prevents misalignments along chest graphics and side ventilation panels, guaranteeing that team kits delivered to Nairobi match global retail standards.
Under Kenya’s intense equatorial sunlight, conventional screen inks and transfer vinyls crack, fade, or peel within months of routine washing. Digital dye sublimation transfers Eco-friendly water-based inks deep into the synthetic fibers at 210°C.
The dye becomes part of the polymer matrix itself. The resulting garment retains 100% of its original breathability, exhibits zero hand-feel stiffness, and guarantees a Grade 4+ color fastness rating against high UV exposure and aggressive laundering.
By leveraging established air-freight corridors between Shenzhen/Guangzhou and Jomo Kenyatta International Airport (NBO) in Nairobi, or sea freight to Mombasa Port (MBA), wholesale orders clear customs efficiently. GoldenLeaf Sports manages end-to-end quality assurance, providing photographic and video pre-shipment reports to ensure zero-defect consignments.
Location: Maasai Mara, Amboseli & Tsavo Eco-Resorts
Luxury safari operators require durable, breathable, anti-pilling polo shirts and T-shirts in earth tones (khaki, olive green, sandstone). Dye sublimated chest logos and sun-protective 50+ UPF fabrics ensure guides remain comfortable and polished during long game drives in hot weather.
Location: Eldoret, Iten & Nairobi Athletic Events
Kenya’s world-renowned marathon culture requires ultra-lightweight (140 GSM) CoolMax running tees. Open-weave bird-eye mesh panels facilitate maximum thermoregulation during high-altitude training sessions, while seamless flatlock stitching eliminates chafing over long distances.
Location: Nairobi Financial Hubs & Universities
Commercial enterprises, non-governmental organizations (NGOs), and educational institutions demand large-volume promotional apparel. Engineered polyester-cotton blends combine softness with durable structure, delivering cost-effective high-volume solutions for regional campaigns.
Selecting the optimal fabric blend is the most critical decision in apparel procurement. Below is an engineering breakdown of base cloths utilized by GoldenLeaf Sports for customized wholesale T-shirt manufacturing:
Best For: Sublimated Sports Jerseys, Team Wear, Marathon Shirts
Smooth knit construction optimized for vivid ink absorption. Features quick-dry capillary action that pulls sweat away from the skin to the outer fabric layer for rapid evaporation.
Best For: Training Vests, Side Panel Inserts, Hot-Climate Workwear
Features a micro-pinhole pattern that maximizes airflow while maintaining full fabric opacity. Ideal for side panels on jerseys or full body construction in high-temperature environments.
Best For: Compression Gear, Modern Athletic Fits, Racing Jerseys
Combines micro-polyester with 12% elastane, providing multi-directional stretch recovery. Allows complete freedom of movement without losing structural shape over time.
Best For: Premium Corporate Merchandise, Retail Streetwear
Long-staple cotton fibers combed to remove impurities, delivering an exceptionally soft hand-feel. Perfect for screen printing, DTG (Direct-to-Garment), and custom embroidery.
Direct answers to technical, commercial, and logistical questions encountered by wholesale buyers in East Africa.
High-performance customized sportswear, activewear, and promotional gear produced under ISO 9001 certified manufacturing standards.
Ready to source custom sublimated T-shirts, team kits, and corporate promotional wear? Get direct factory pricing, free 2D artwork mock-ups, and expert material advice within 24 hours.