



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Precision-engineered sportswear and event uniforms manufactured at our 3,000 m² Shenzhen campus. Built for extreme durability, weather-resistance, and high visual impact.
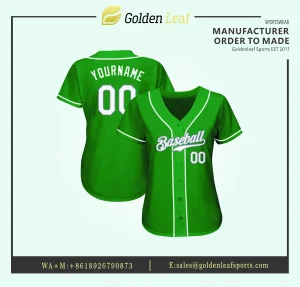
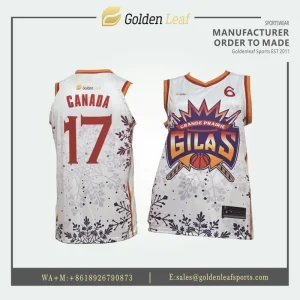
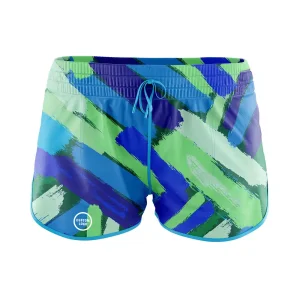
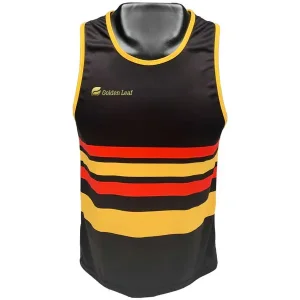
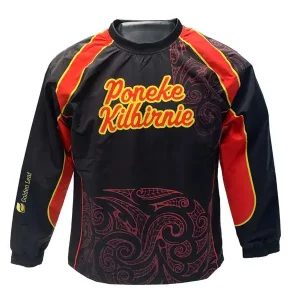
The global live event and music festival industry has undergone a radical operational shift. Uniforms are no longer merely identification markers; they are critical brand assets and technical gear.
Global event organizers are mandating net-zero sustainability targets. Modern festival apparel utilizes recycled polyethylene terephthalate (rPET) derived from post-consumer plastics, paired with non-toxic, water-based Italian digital sublimation inks certified under OEKO-TEX Standard 100.
Technological convergence has introduced heat-sealed RFID and NFC chip pockets within festival uniforms. This allows staff access control to restricted zones (Stage, VIP, Backstage), time-tracking, and seamless inventory management directly through crew apparel.
The line between working staff uniforms and retail festival merch has blurred. Event organizers now leverage high-fashion, edge-to-edge sublimated designs, oversized streetwear cuts, and vintage baseball jersey silhouettes that attendees purchase as premium souvenirs.
According to recent global event supply metrics, festivals with multi-day outdoor operations require high-performance technical fabrics rated at least UPF 50+ UV protection and engineered with hydrophilic wicking properties (145-180 GSM bird-eye mesh) to prevent staff fatigue and withstand extreme sun exposure, heavy rain, and high friction environment.
Managing multi-national festival tours, stadium shows, and global event series requires robust manufacturing operations capable of overcoming key sourcing hurdles.
Festival production deadlines are inflexible. Suppliers must offer quick-turnaround prototyping (24-48 hour digital mock-ups, 5-7 days pre-production samples) and rapid bulk production within 12-18 working days. Low Minimum Order Quantities (MOQs) of 10 pieces per design allow event managers to place last-minute add-ons for specialized artist crews without punitive costs.
Global brands demand strict Pantone Matching System (PMS) accuracy. Using advanced Raster Image Processor (RIP) color-management software, uniform factories must ensure that stage crew hoodies produced in January perfectly match security vests printed in August across all fabric densities.
A single major music festival requires up to 15 distinct uniform iterations: Audio/Lighting Crew, Security, Medical Staff, Hospitality, VIP Hosts, Tech Directors, and Volunteers. Factories must offer uniform pattern libraries spanning breathable V-neck baseball tees, 4-way stretch rugby jerseys, light jackets, and athletic shorts.
B2B distributors and brand managers require complete white-label manufacturing. This includes customized woven neck labels, heat-seal size tags, custom branded polybags, specialized hang tags, and barcoded packaging sorted directly by event zones and staff sizes.
GoldenLeaf Sports (ShenZhen) Co., Ltd. solves the core pain points of international B2B buyers through vertical integration, end-to-end quality control, and advanced dye-sublimation technology.
Spanning 3,000 m² in Shenzhen, China, our manufacturing campus integrates vector design, pattern grading, digital paper printing, high-temperature heat-press transfer, automated laser cutting, flatlock/overlock stitching, and final QC inspection under one roof.
We engineer specialized textiles tailored to outdoor environments: 100% polyester interlock (145-180 GSM), bird-eye moisture-wicking mesh, 4-way stretch poly-spandex (88/12), heavyweight rugby twill, and water-repellent windbreaker shells.
Our digital dye-sublimation process fuses ink directly into the synthetic polymer fibers at high temperatures. Unlike traditional screen printing or vinyl transfers, our graphics will never crack, peel, or fade, surviving over 100+ commercial wash cycles.
Every festival uniform order follows strict ISO-compliant manufacturing steps overseen by experienced apparel engineers.
Review festival environmental requirements, target quantity, fabric GSM preferences, and sizing blocks (US, EU, AU, Youth).
Garment technicians adjust vector patterns across full size ranges (6Y to 5XL) to maintain design proportion across all fits.
Dedicated graphic designers create 24-48 hour virtual 3D mock-ups, fine-tuning Pantone colors and logo placements.
High-resolution printers output designs onto specialized thermal transfer paper using eco-friendly ink formulation.
Calender heat rolls transfer pigment deep into white polyester fabrics under controlled heat (200°C) and uniform pressure.
Registration-mark laser cutters slice printed panels with microscopic edge precision, preventing fabric fraying.
Industrial sewing technicians execute reinforced twin-needle, flatlock, and cover-stitch operations for intense physical wear.
Five full-time quality inspectors verify dimensions, stitch count, color fidelity, and packaging compliance prior to export.
GoldenLeaf Sports ensures hassle-free customs clearance and full regulatory alignment across all major target markets including North America, Europe, Oceania, and the Middle East.
All raw textiles, elastic bands, zip closures, and sublimated dyes used in our plant pass strict chemical testing. Our products are fully compliant with EU REACH standards, US CPSIA guidelines, and carry OEKO-TEX Eco-Passport verification, ensuring skin-safe, zero harmful azo-dye properties.
Fit preferences vary significantly by country. We offer region-specific pattern blocks: loose-fit streetwear blocks for the US market, tailored slim-fit blocks for European festivals, and specialized athletic proportions for Australian rugby and sports events.
We support a full suite of international trade agreements including EXW, FOB Shenzhen/Yantian, CIF, and Delivered Duty Paid (DDP). Our logistics network provides express air freight (3-5 days delivery) for emergency tour needs, as well as sea/rail freight for cost-optimized bulk orders.
We back our production with a 100% replacement warranty on manufacturing defects, measurement errors exceeding acceptable tolerance (±1cm), or color discrepancies against approved pre-production strike-offs.
Explore our automated sublimation printing lines and skilled sewing workshops in Longgang District, Shenzhen.
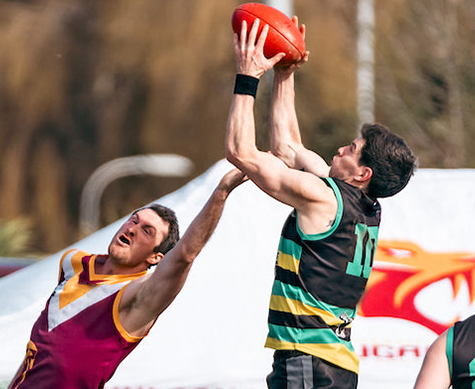
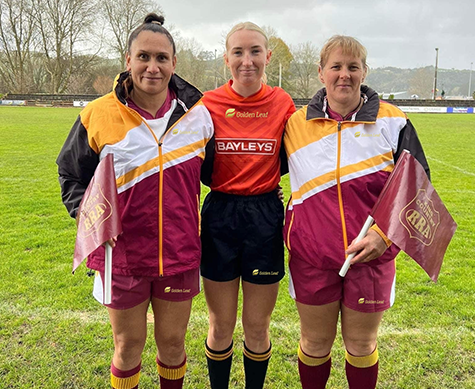
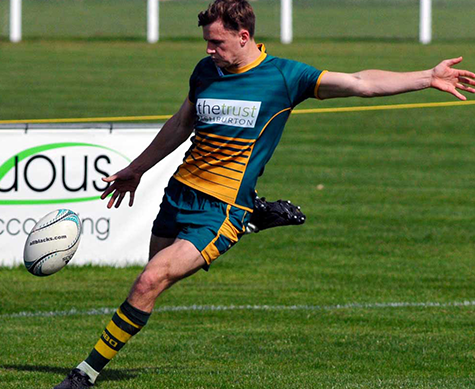
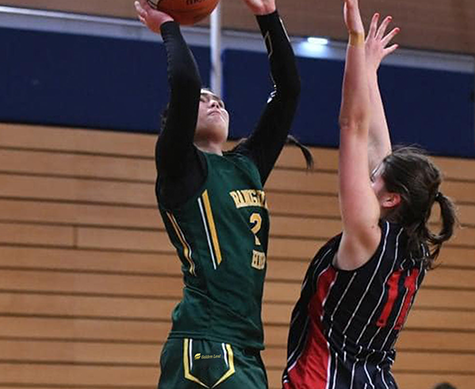
GoldenLeaf Sports is investing heavily in Next-Gen manufacturing processes to pioneer the future of event crew apparel and smart activewear.
Integration of AI pattern-nesting software reduces fabric waste by up to 18%, significantly lowering raw material consumption and minimizing overall production costs for high-volume B2B orders.
Development of specialized sublimation inks that incorporate photoluminescent pigments for low-light night-stage environments, enhancing crew visibility and safety during midnight festival shift changes.
Transitioning toward waterless heat transfer printing across 100% of product lines, drastically reducing industrial water consumption and aligning with global clean-energy initiatives.
Read authentic performance reports from event coordinators, athletic directors, and tour apparel managers.
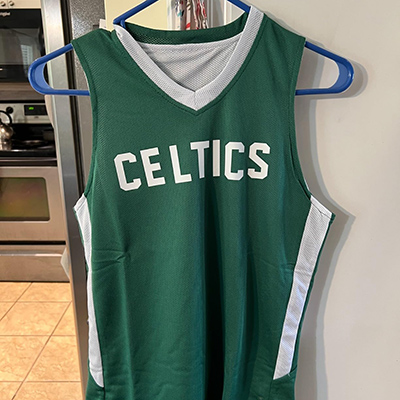
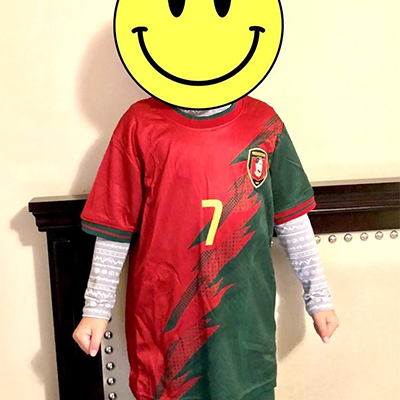
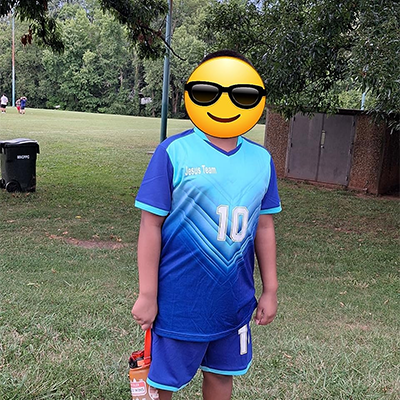
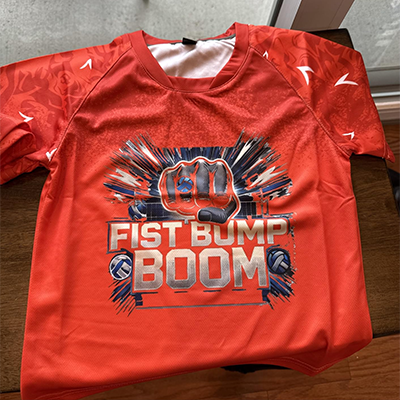
Detailed factory-level responses addressing common technical questions raised by B2B buyers and event directors.
Our standard MOQ is just 10 pieces per design for sublimated tops, jerseys, pinnies, and shorts. Because each fabric panel is digitally printed prior to automated laser cutting, you can customize player/staff names, security numbers, and individual body sizes within the same 10-piece production batch at no extra setup cost. Accessories like woven socks or embroidered caps carry separate MOQ thresholds depending on yarn specifications.
Vector artwork proofing and 24-48 hour digital mock-ups are completed free of charge. Physical pre-production strike-offs or complete samples require 5 to 7 working days. Once the sample is approved, bulk orders of 300 to 1,000 garments ship in 12 to 18 working days. Rush manufacturing slots are available for sudden festival tour schedule adjustments.
For high-temperature outdoor events, we recommend our 145-160 GSM Bird-Eye Micro-Mesh or 150 GSM Cool-Max Polyester Interlock. These synthetic knits feature open-hole hydrophilic micro-channels that pull perspiration away from skin, facilitating rapid evaporation. Furthermore, all our white base fabrics undergo UV-blocking baths offering certified UPF 50+ protection.
Yes. We specialize in dual-layer reversible sublimated pinnies and vests for security and stage technicians needing swift color changes (e.g., Daytime Setup vs. Nighttime Show). We also customize functional elements such as utility pockets, reinforced radio loops, mic tabs, and heavy-duty YKK zips.
We utilize industry-grade RIP software coupled with calibrated spectrophotometers. Before mass printing, our technicians output physical color swatches onto your selected fabric stock to verify RGB-to-CMYK Pantone translation. This guarantees color harmony between poly-spandex jerseys, nylon jackets, and cotton-feel hoodies.
We provide comprehensive private labeling: woven neck labels, tagless heat-transfer neck prints, custom barcoded hang tags, eco-friendly polybag printing, and custom master carton labeling sorted by festival zones or staff sizes for frictionless field distribution.
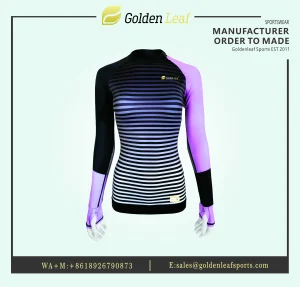
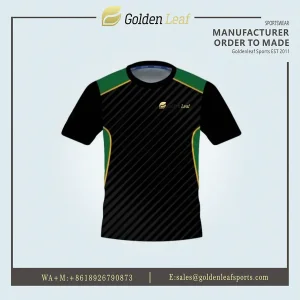
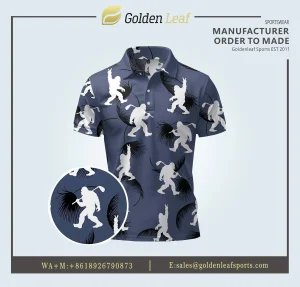
Explore our full range of performance activewear, outerwear, and team uniforms available for global OEM bulk order.
Consult with our Shenzhen apparel engineering team today. Get free 3D digital mock-ups within 24 hours, custom fabric swatch packages, and factory-direct pricing for your next major event.