



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our top-tier custom OEM/ODM teamwear and performance shirts produced using state-of-the-art dye-sublimation and moisture-wicking technology.
Analyzing global trade shifts, functional textile demands, and why top apparel brands partner with specialized OEM/ODM manufacturing hubs.
The global polo shirt market is projecting a steady CAGR of 5.8% through 2030. Growth is driven by the blurring lines between professional workwear, executive casual attire, and high-performance technical sports apparel.
Traditional heavy cotton piqué is rapidly losing market share to modern polyester-spandex blends, micro-mesh weaves, and eco-friendly recycled fibers offering moisture management, UPF solar protection, and four-way stretch flexibility.
Modern brand distributors no longer hold massive unprinted inventory. Global sourcing managers demand responsive suppliers capable of delivering custom dye-sublimated runs starting at just 10 pieces with zero color compromise.
From raw yarn selection to molecular ink bonding, explore the rigorous manufacturing processes that guarantee anti-pilling, colorfastness, and thermal regulation.
| Fabric Technical Spec | Composition & Weight (GSM) | Key Performance Attribute | Primary B2B Application |
|---|---|---|---|
| Micro-Piqué Poly-Spandex | 88% Polyester / 12% Elastane (160 - 180 GSM) | 4-Way Stretch, Wrinkle Resistance, UPF 50+ | Executive Corporate & Championship Golf Polos |
| Cool-Max Birdseye Mesh | 100% Quick-Dry Polyester (145 - 160 GSM) | High Air Permeability, Rapid Moisture Evaporation | Motorsport Racing, Outdoor & Ultimate Frisbee Shirts |
| Heavyweight Rugby Twill Interlock | 100% High-Tenacity Polyester (220 - 280 GSM) | Tear Resistance, Reinforced Collars, High Tensile | Rugby Match Wear, Tactical Outdoor & Workwear |
| Recycled rPET Eco-Knit | 100% Repreve® Post-Consumer Poly (150 GSM) | Low Carbon Footprint, GRS Certified, Soft Hand-feel | Eco-Conscious Corporate Apparel & University Kits |
Using solid-to-gas phase transfer at 210°C, custom graphics, sponsor logos, and Pantone matched gradients are fused directly into the polyester polymers. Unlike screen printing, graphics will never crack, peel, or block airflow.
Automated optical laser cutting machines read printed registration targets on paper-transferred fabric rolls. This guarantees millimeter-exact alignment across collar seams, plackets, sleeves, and side vents across all size runs.
Engineered with twin-needle flatlock stitching and reinforced collar taping. Friction points are minimized to ensure comfort during intense physical movement or long corporate workshifts.
Leveraging Shenzhen's advanced technological infrastructure and integrated textile ecosystem to deliver unmatched agility, rapid prototyping, and cost performance.
Located in Longgang, Shenzhen, our direct proximity to world-class yarn spinning mills, digital ink chemical synthesis facilities, and automated trim suppliers reduces raw material transit lead times to less than 24 hours.
Our proprietary lean manufacturing matrix allows seamless switching between 10-piece custom small orders and 50,000-piece bulk corporate runs without sacrificing machine efficiency or altering pricing transparency.
Every piece undergoes 5 strict QA inspection checkpoints: digital artwork vector verification, printed transfer paper audit, post-sublimation color spectrum matching, seam-pull stress test, and final needle detection.
Custom engineered polo shirt solutions tailored to the strict compliance, environmental, and aesthetic demands of global industries.
Designed for brand consistency. Anti-curl knitted collars, discrete embroidery or subtle sublimation logos, and stain-resistant fabric finishes ideal for tech, airline, and logistics staff.
Premium lightweight piqué knits with high elastane content providing full rotational torso freedom. UV sunblock UPF 50+ rating protects players during 18-hole outdoor sessions.
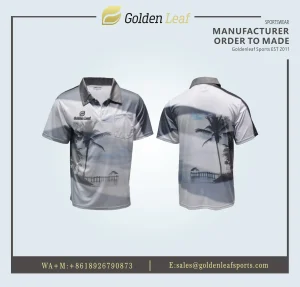
High-contrast, vibrant edge-to-edge sublimation printing that reproduces complex sponsor graphics, carbon-fiber textures, and racing stripes without adding heavy rubberized layers.
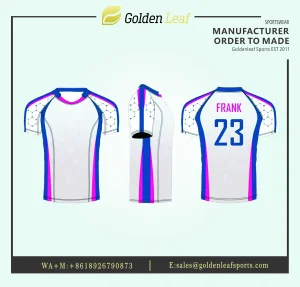
Durable, machine-washable team polo kits engineered to withstand frequent heavy laundering. Graded patterns available from Youth XS (6Y) up to Adult 5XL.
Seamless international trade integration with full regulatory compliance, custom brand trims, and flexible incoterms.
All sublimation inks are imported and non-toxic, complying with OEKO-TEX Standard 100 Class I (safe for skin contact) and REACH European chemical safety standards. Formal test reports supplied upon request.
Complete ODM branding packages including custom woven neck tags, heat-transfer inner size labels, printed barcode hangtags, individual eco-polybags, and branded master shipping cartons.
We support EXW, FOB Shenzhen, CIF, and DDP shipping terms via DHL, FedEx, air cargo, and sea transport directly to warehouses across North America, Europe, Australia, and the Middle East.
Everything you need to know about customizing, ordering, and importing high-quality polo shirts directly from our factory floor.
Complete your line with custom fishing apparel, athletic shorts, casual hoodies, and specialized tournament shirts built for maximum durability.
Direct Factory Pricing · Free Virtual Mockups in 24h · ISO9001 Certified Production · Low 10-Piece MOQ
Request Technical Quote & Fabric Catalog