GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered for high-intensity movement, rapid thermal regulation, and structural elasticity across demanding athletic environments.
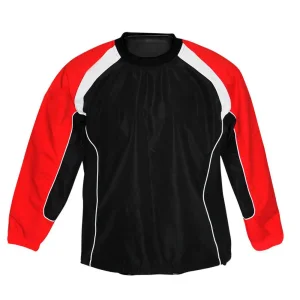
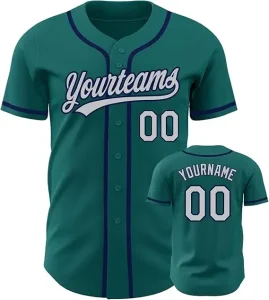
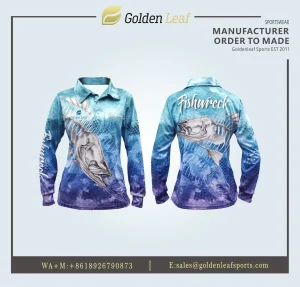
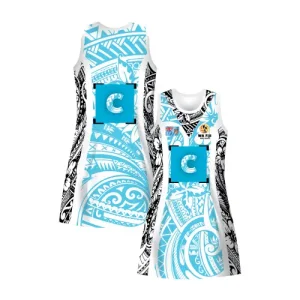
Operational data across our 3,000 m² Shenzhen manufacturing complex, serving international sports organizations, motorsport crews, and global teamwear brands.
Direct export lines operating under DDP, FOB Shenzhen, and CIF protocols across North America, Europe, Australia, and the Middle East with verified compliance paperwork.
High-temperature molecular ink bonding into 100% micro-polyester and poly-spandex blends ensures zero surface peeling, cracking, or color fading over heavy washing cycles.
Every lot undergoes stress tests for tensile seam strength, fabric GSM density verification, color fastness checks (Grade 4+), and dimensional stability reviews.
In modern high-performance sports and motorsport pit environments, technical apparel serves as vital equipment rather than decorative gear. The phrase "Racing Supplier & Factory" represents a specialized engineering vertical focused on producing lightweight, thermo-regulating, and mechanically resilient garments tailored to the rigorous demands of professional drivers, pit crews, track technicians, and endurance athletes.
At GoldenLeaf Sports, operating out of our specialized manufacturing hub in Longgang District, Shenzhen, we integrate full-chain R&D, digital artwork rendering, precision sublimation printing, laser panel cutting, and dynamic flatlock assembly under one operational umbrella. Achieving optimal performance requires a structural understanding of how synthetic polymer textiles interact with heat transfer dyes and dynamic muscular movements.
Unlike traditional screen printing or vinyl transfers which place an opaque rubberized layer on top of textiles, full-dye sublimation heats specialized eco-friendly inks to 200°C (392°F). At this precise threshold, the synthetic polyester fibers expand, allowing gaseous dye molecules to penetrate directly into the core matrix of the yarn. The result is zero added weight, 100% structural breathability, and absolute resistance to peeling or abrasion.
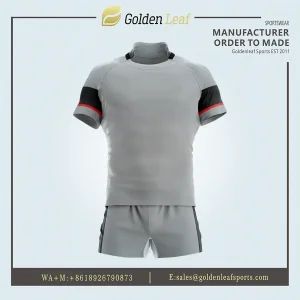
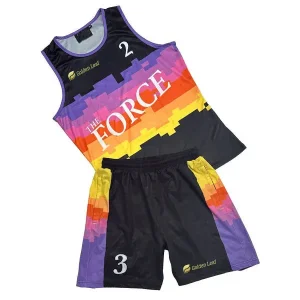
Our operational framework caters to OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) buyers globally. Whether supplying high-visibility pit crew polo shirts, flame-retardant outer layer shells, moisture-wicking compression base layers, or sublimated team kits for rugby, baseball, netball, and basketball, technical accuracy in textile selection remains non-negotiable.
| Technical Specification | Standard Commercial Textiles | GoldenLeaf Engineered Racing Textiles |
|---|---|---|
| Yarn Composition | Generic 100% Spun Polyester | High-Filament Micro-Interlock & Poly-Spandex Blends (88/12) |
| Fabric Weight (GSM) | Fixed 120 - 140 GSM | Custom Graded 145 GSM, 180 GSM, to Heavyweight 280 GSM Twill |
| Moisture Vapor Rate (MVTR) | < 3,000 g/m²/24h | > 8,500 g/m²/24h (Cool-Max Hydrophilic Treatment) |
| Color Fastness (Washing/UV) | Grade 2 - 3 (Fades after 15 washes) | Grade 4 - 5 (Tested for 50+ Industrial Wash Cycles) |
| Seam Construction | Standard 3-Thread Overlock | Reinforced Twin-Needle Flatlock & Anti-Chafing Seams |
How Shenzhen's advanced manufacturing ecosystem enables unmatched turnaround speed, cost efficiency, and raw material optimization.
Operating in Guangdong placing us within a 50-kilometer radius of the world's dense raw material mills. This direct proximity allows us to source high-grade bio-polyesters, micro-mesh textiles, and elastane yarn in under 24 hours, dramatically cutting down pre-production lead times.
From RIP digital color management to computerized multi-head sublimation printers and automated laser registration cutters, every manufacturing phase happens inside our 3,000 m² facility. Outsourcing zero critical steps guarantees total quality control and protects customer IP.
China's athletic apparel manufacturing sector has evolved from low-cost bulk assembly into high-value technical manufacturing. By combining automated vector pattern grading with low-impact eco-friendly inks imported from specialized chemical developers, Shenzhen factories set global standards for quality-to-cost ratios.
Furthermore, the agility of China's logistics network enables seamless export routines. Goods produced on our factory floor can be consolidated, customs-cleared, and placed aboard express air carriers within 48 hours of final QC packaging, guaranteeing delivery to warehouses in the United States, Europe, or Australia within 5 to 7 business days.
Modern B2B buyers—ranging from independent apparel brands and regional sports clubs to corporate event organizers and motorsport leagues—face complex procurement challenges. Maintaining high stock levels carries financial risk in fluctuating markets, making inventory flexibility vital for operational success.
While traditional garment mills demand 500+ units per style, our production lines accept minimum orders starting at just 10 pieces per design. Because panel graphics are sublimated prior to cut-and-sew, individual player names, numbers, and custom sizing can change dynamically within a single short-run order at zero extra setup fee.
We provide full white-label and private-label packages including custom woven neck labels, heat-seal brand logos, personalized swing tags, barcodes, and custom-printed polybags to ensure products arrive retail-ready for immediate distribution.
Our in-house design team generates digital 3D apparel mock-ups within 24–48 hours of receiving vector graphics. Physical pre-production samples are completed in 5 to 7 working days, allowing buyers to physically audit fabric hand-feel, collar structure, and color accuracy.
Purchasing agents require absolute transparency across the supply chain. Through dedicated project managers, buyers receive continuous updates—including digital fabric print swatches, laser cutting video logs, and pre-shipment inspection checklists—ensuring full alignment with signed specifications before goods depart the facility.
Operating on an international scale requires strict adherence to regional regulatory frameworks and distinct regional ergonomic sizing preferences. A uniform cut designed for Western European football leagues requires different sleeve pitch and torso contouring than apparel tailored for Asian or North American athletic body profiles.
All textiles and dyes used in our factory comply with international safety standards including OEKO-TEX Standard 100 Class I, REACH chemical limitations, and CPSIA (Consumer Product Safety Improvement Act) standards in North America. Base materials are independently laboratory tested for skin sensitivity, AZO-dye absence, and formaldehyde thresholds.
We maintain an extensive database of regional master patterns spanning Men's, Women's, and Youth sizing categories (from 6Y up to 6XL). Custom adjustments for extended torso lengths, tapered sleeves, high-waist athletic leggings, or specialized compression fits are handled effortlessly via vector pattern software.
The global custom sportswear market is undergoing a structural transition toward smart, eco-responsible textiles and digitized manufacturing workflow. Key trends driving this evolution include:
Targeted apparel configurations tailored to specialized athletic and commercial environments.
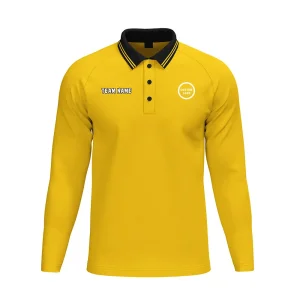
Durable 180 GSM micro-interlock button polo shirts featuring dirt-resistant coatings, UV50+ solar protection, and reinforced armpits to endure trackside friction and variable weather conditions.
Rugby, American football, and lacrosse jerseys built with 280 GSM heavyweight stretch-twill and flatlock stitching capable of resisting pull forces exceeding 400 Newtons without seam failure.
Lightweight 145 GSM bird-eye mesh tees and high-waist quick-drying joggers optimized for thermal transfer during marathons, gym training, and high-intensity interval workouts.
Detailed insights into factory capabilities, order workflows, material choices, and international shipping terms.
Expand your product catalog with high-performance teamwear, outdoor sports apparel, and casual athletic wear options.